
瑞铁机床(苏州)股份有限公司
Taicang, Suzhou, Jiangsu
DERATECH FA lasers: fit the blank and the loading route
Compare 3 × 1.5 m, 4 × 2 m and 6 × 2.5 m cutting formats. Plan the longer machine footprint, exchange-table access and material-specific cut before choosing a package.
Official FA parameter tab, original images and municipal company record reviewed 8 October 2026
Match the largest blank before increasing power
Start with material grade, thickness, stock size and a representative nest. FA3015, FA4020 and FA6025 provide different sheet formats in the standard FA family. A larger bed can avoid splitting a large blank; it does not automatically improve the quality or cycle time of a smaller part.
| Reference | FA3015 | FA4020 | FA6025 |
|---|---|---|---|
| Processing range | 3000 × 1500 mm | 4000 × 2000 mm | 6000 × 2500 mm |
| X / Y travel | 1550 / 3050 mm | 2050 / 4050 mm | 2550 / 6050 mm |
| Z travel | 300 mm | 300 mm | 300 mm |
| Listed machine dimensions | 9525 × 2850 × 2650 mm | 13200 × 3500 × 2650 mm | 15500 × 4005 × 2650 mm |
| Family laser-power entry | ≤6000 W | ≤6000 W | ≤6000 W |
| Existing model record | FA3015 ↗ | FA4020 ↗ | FA6025 ↗ |
Swipe to compare cutting format, axis travel and machine dimensions.
The X/Y axis labels differ from the long/short dimensions used to describe sheet format. Preserve the manufacturer's axes when checking a layout or program. Z travel is head motion, not a maximum material thickness. The shared ≤6000 W entry is a family upper limit; specify the actual source power being quoted rather than assuming every model ships with 6 kW.
Draw the full sheet-handling route
Storage → loading
Specify blank length, width, thickness and mass; show how it reaches the loading area from stock storage. Check lifting equipment, approach direction and how an operator positions the sheet on its supports. Maximum cutting format does not establish the included sheet-handling capacity.
Exchange → cutting
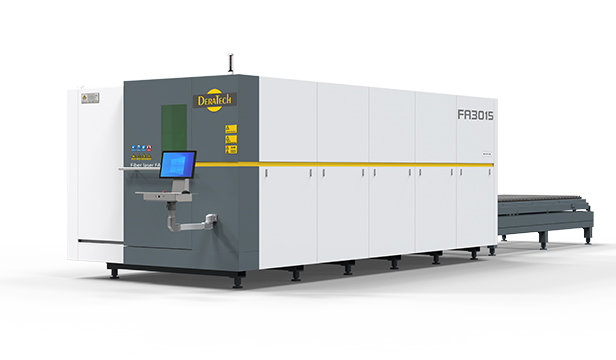
Compare the listed 9.525 m, 13.2 m and 15.5 m machine lengths with the quoted installation drawing. Reserve exchange-table movement, operator access, opening doors and maintenance clearances. Confirm the table arrangement and exchange restrictions for the exact FA version.
Unloading → next operation
Plan removal of large cut parts, small parts and the remaining skeleton. State whether parts go directly to bending, welding or coating. Provide sorting space and a handling method that protects accepted edges and prevents the scrap skeleton from obstructing the next sheet.
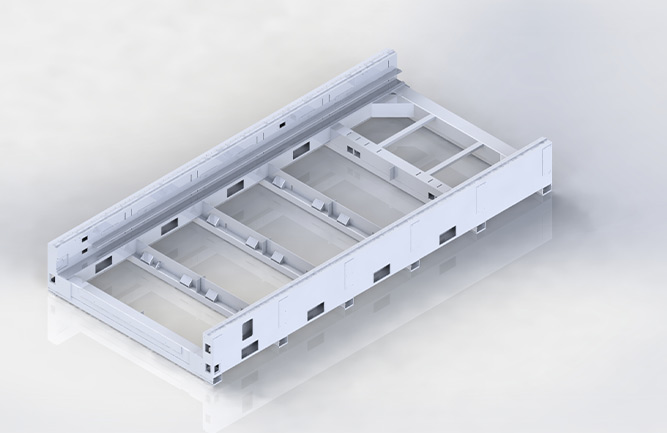
The published machine dimensions are a starting reference, not a complete occupied-area guarantee. Add the actual chiller, extraction system, gas equipment, electrical cabinets if separate, staging areas and safe access. Ask for floor-load and foundation requirements with the operating layout.
Order one defined cutting system
- Source and head
- The manufacturer describes fiber-laser cutting with an autofocus head. Specify source maker/model/power, head model, focus range, protective optics, nozzles and matching cooling. High-power products elsewhere in the catalogue are a separate route; their ratings should not be added to the standard FA references.
- Gas, cooling and extraction
- Give the planned assist gases and facility supply. Obtain required pressure/flow, gas quality, chiller rating and ambient conditions for the selected source. Confirm extraction, filters and maintenance access for the actual materials and duty. Source watts alone do not determine electrical supply or gas consumption.
- Software and nesting
- Specify drawing formats, units, kerf compensation, material libraries and the nesting workflow. Demonstrate import of your own drawing revision, piercing strategy, part ordering and restart after interruption. Ask which software licenses and training are included; a machine photograph cannot establish them.
- Safety and handover
- Request the delivered machine's guarding, interlock and operating documentation, destination conformity requirements and commissioning responsibilities. Confirm the power/voltage, gas connections and emergency procedures before installation. Agree consumable spares and who provides on-site support.
Accept a nest that produces usable edges
The FA specification page explains that its displayed product and performance information comes from the company's own tests. Use it to shortlist a configuration; validate the required result on your grade, thickness and drawing.
Include difficult features
Use long straight cuts, corners, the smallest holes, narrow webs and parts at both central and edge-of-sheet locations. Include the largest blank or longest finished contour needed by the job. Agree nozzle, gas, focus and pierce settings, and retain them with the results.
Measure after unloading
Inspect dimensions, hole form, burr, dross, edge condition and flatness against the drawing. If the part will be bent or welded, include that downstream operation in acceptance. A clean-looking cut photograph is not a measured production sample.
Time the complete sheet
Record loading, exchange, piercing, cutting, unloading and sorting. Compare repeated sheets under the same conditions rather than quoting head motion as production output. Include planned consumable changes and any deburring required for the next operation.
Retain a repeatable handover
Keep the drawing/nest revision, material identification, NC job, parameter file and measurement method. Agree operator training, routine inspection, spare optics/nozzles and the response process for edge-quality changes during the planned batch.
DERATECH's Suzhou sheet-metal scope
The current official site identifies 瑞铁机床(苏州)股份有限公司 and describes cooperation with DERATECH in Belgium. Its catalogue covers electric, hybrid and electro-hydraulic press brakes, fiber lasers, shears, turret punches, grooving and automated sheet-metal lines. Group operating history does not establish the age or ownership of the local legal entity.
The Suzhou government's 2020 recognition notice, Su Fu [2020] No.16, names the same company's technical center at attachment entry 38. It supports a specific historical R&D record; it is not certification of an FA laser or independent proof of the cutting results described above.
This page reviews the three existing FA-format records. Other product families need their own tooling, machine and acceptance evidence. Catalogue facts are from reviewed manufacturer material; layout and trial guidance are CNCVerified purchase-planning analysis. Confirm the exact legal supplier, ordered configuration and service responsibilities in the proposal.
Send a nest and a shop-layout sketch
Include material/thickness, blank dimensions and mass, drawing or nest, small-feature and edge requirements, downstream operations, batch target and destination. Show the available loading/unloading route, utilities, desired FA format and the source/head package to be tested.
Send DERATECH RFQ ↗