

普锐米勒机床(东莞)有限公司
Huangjiang, Dongguan, Guangdong
PRIMINER: rotate the part or the head?
Separate fixed-table gantry work from cradle five-axis and swivel-head machining. Start with the part, fixture and access to its features.
Company and four product-family pages reviewed 8 October 2026
Which motion does the job actually need?
- A supported part on a non-tilting table
- Use the V2516 or GT16/GT18 gantry path when the planned operations fit three linear axes and the chosen setup. Check the opening, spindle clearance and clamps around the part. A large table does not provide access to every side without another setup or a specified attachment.
- A part that can move with a cradle
- C800 lists A/C table rotation. Include the fixture, part and center of gravity when checking the swept volume and permitted load at the required angle. Its listed table load is not an all-angle load curve.
- A large part with a moving spindle head
- GT428-5X lists a direct-drive A/C head over a large table. Keep the fixture and workpiece support in the proposal, then check the tilted head, holder and tool against the part and clamps. Nominal XYZ travel does not define reach at every head angle.
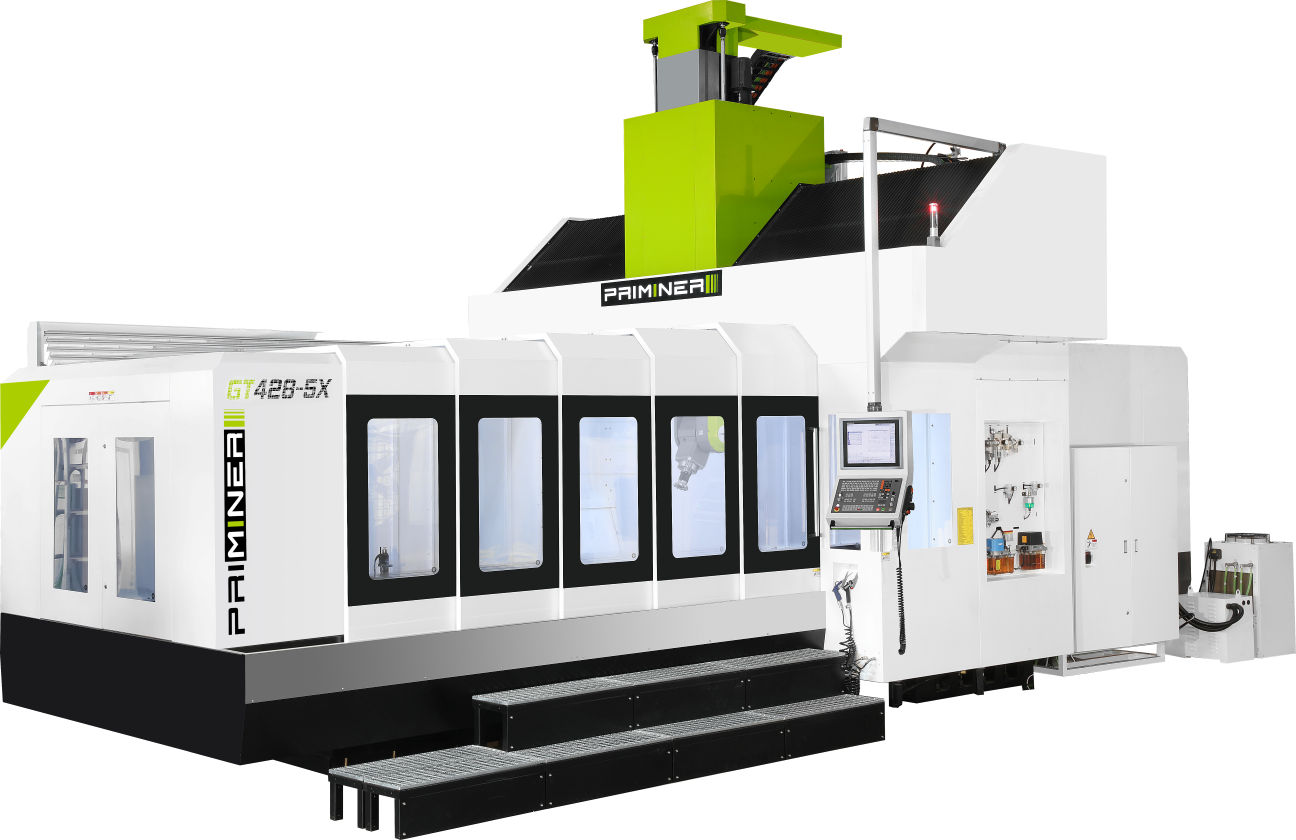
Compare structures before spindle speeds
| Constraint | V2516 gantry | C800 cradle | GT428-5X head |
|---|---|---|---|
| X / Y / Z travel | 2500 / 1600 / 800 mm | 900 / 850 / 600 mm | 4200 / 3300 / 1200 mm |
| Table size, as listed | 2500 × 1400 mm | Ø800 × 700 mm | 4000 × 2400 mm |
| Listed table load | 7000 kg | 800 kg | 12000 kg |
| Angular travel | Not listed for this three-axis entry | A: ±120°; C: 360° | A: ±108°; C: ±360° |
| Spindle interface / speed | HSK A100 / 12000 rpm | HSK A63 / 16000 rpm | HSK A100 / 12000 rpm |
| Existing model page | V2516 ↗ | C800 ↗ | GT428-5X ↗ |
Swipe to compare all three structures on a narrow phone.
V2516 lists 200–1000 mm spindle-nose clearance and a 1600 mm gantry opening. C800 lists 170–770 mm clearance, but its part and fixture also sweep through space as the table tilts. GT428-5X publishes −10–1110 mm spindle-nose clearance; obtain the reference angle and tool/setup drawing rather than treating that unusual entry as unrestricted space.
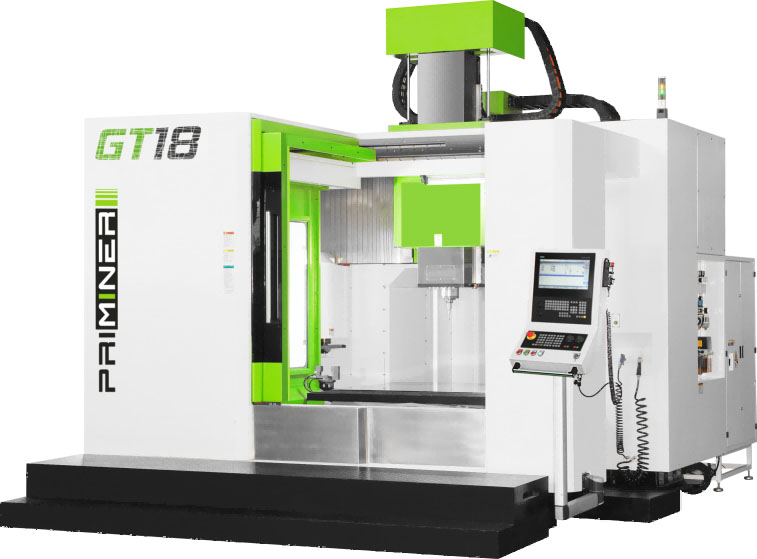
GT16 or GT18 for a smaller gantry job?
GT16 lists 1600/1200/600 mm travel, an 1800 × 1050 mm table and 3000 kg load. GT18 lists 1800/1400/800 mm, an 1800 × 1400 mm table and 6000 kg load. Both specify HSK A63 at 20000 rpm; the GT18 comparison came from selecting its own model tab, not reusing GT16's numbers.
GT16's magazine is 40 positions; GT18's is 60. Both list 300 mm tool length, 8 kg tool mass and 78/150 mm diameter with full/adjacent-empty positions. Check actual fixture support and tool occupancy before choosing the larger arrangement.
Put the spindle, magazine and foundation into one package
HSK A63 and A100 are different tool chains. Match the holders, pull studs or clamping interface as applicable, tool length, diameter and loaded mass to the selected spindle and magazine; do not budget on reusing tooling until the interface is confirmed.
C800 lists 40 tools, 300 mm length, 8 kg mass and 65/130 mm diameter with occupied/adjacent-empty positions. GT428-5X lists 60 tools, 400 mm length, 16 kg mass and 125/250 mm diameter under those conditions. Empty adjacent positions reduce the usable count, while a tilted head or cradle may impose another collision limit.
Published power entries are V2516:20/22.5 kW, C800:30/36 kW, GT16/GT18:30/36 kW and GT428-5X:50/61 kW. The slash entries do not define duty here. Request the selected spindle's torque/speed curve and sustained conditions for the intended roughing and finishing job.
Installation needs more than transport dimensions. The GT428-5X table lists 52000 kg machine mass and 10580 × 5855 × 6320 mm overall dimensions. Obtain foundation loads, anchoring, leveling and rigging plans, doors and maintenance access, magazine space, cooling and chip-removal layout before confirming the destination workshop.
Prove the tool path and finished geometry
Simulate the quoted kinematics
Supply the part, fixtures and complete tool assemblies to the actual CAM/postprocessor and controller configuration. State indexed or simultaneous motion. Check tilted-table/head clearance, travel limits, rotary transitions and retracts, then prove the important paths on the machine.
Agree a representative cutting trial
Use the intended material and loading arrangement, with features at the difficult angles and depths. Record reclamping, complete cycle steps, warm-up and cooling conditions. The pages' linear/angular scales and ±0.1° spindle-water-cooling entries do not establish finished-part accuracy or part-temperature control.
Measure and retain the process
Define datums, contour or hole-position requirements, instruments, sampling and inspection after release from the fixture. Preserve accepted programs, postprocessor/version, offsets, tool and fixture lists, rotary calibration records and destination commissioning tests.
For heavy or off-center C800 setups, require the permitted load and inertia at the operating tilt, not only the catalogue's 800 kg entry. For GT428-5X, agree the effective cutting reach and acceptance across the intended head angles. Add probing, tool measurement or monitoring only when its hardware, software and acceptance scope are in the quote.
Dongguan manufacturing and the German company
The official company material identifies 普锐米勒机床(东莞)有限公司 in Huangjiang, Dongguan, and Priminer Werkzeugmaschinen GmbH in Neumünster, Germany. It describes Chinese-German cooperation in five-axis and high-speed machining-center manufacturing. That description does not establish the legal supplier or destination service obligations for a particular order.
The official GB/T 23713.1-2024 standard record, published 31 December 2024 and implemented 1 July 2025, names the exact Dongguan company among drafting organizations for machine-condition monitoring and prognostics guidance. This is a defined drafting role, not certification of the machines here or evidence that monitoring functions are included.
The model figures belong to their separate official entries. Setup, tool-chain and acceptance guidance is CNCVerified's editorial analysis. Other catalogue families need their own configuration review; confirm contracting entity, commissioning, training, parts and warranty for your destination.
Send the part and required angles
Attach the drawing, material, fixture, total mass and center of gravity. Name the machine path, required features and angles, tool assemblies, CAM/controller, batch and acceptance method. Include workshop height, foundation/site constraints and destination.
Send PRIMINER RFQ ↗