
山东普鲁特机床有限公司
Tengzhou, Shandong
Pulute CK lathes: start with how you hold the part
Separate disc chucking, tailstock-supported shafts and through-spindle stock before choosing CK6140, CK6150 or CK6160 and its bed length.
Company, separate Chinese model sheets and English catalogue reviewed 8 October 2026
A larger bed swing does not solve every setup
- Discs and short blanks
- Check the chuck jaws, blank diameter, slide clearance and tool approach together. A disc that clears the bed may still interfere with the slide or tool station. Include the jaw opening and grip length in the proposal.
- Long shafts between supports
- State the finished length, unsupported span and center requirements. The listed distance between centers is longer than the machining length. Leave room for the chuck, tailstock and tool approach; ask whether the job needs a steady rest and how it changes usable travel.
- Stock through the spindle
- Specify the stock diameter, straightness and feeding arrangement. Spindle bore, usable bar passage and hydraulic chuck drawtube are different limits. None of these three model sheets establishes an included bar feeder, subspindle or automatic second-end machining.
Compare clearance and the selected spindle package
| Constraint | CK6140 | CK6150 | CK6160 |
|---|---|---|---|
| Swing over bed / slide | 400 / 240 mm | 500 / 250 mm | 600 / 395 mm |
| Spindle bore choices | 48 / 82 mm | 82 / 130 mm | 82 / 130 mm |
| Published spindle-speed ceiling | 2000 rpm | 1800 rpm with 82 mm bore; 800 rpm with 130 mm bore | 1800 rpm with 82 mm bore; 800 rpm with 130 mm bore |
| Main motor | 5.5 kW | 7.5 kW; 11 kW option | 7.5 kW; 11 kW option |
| Four-position square tool shank | 20 × 20 mm | 25 × 25 mm | 25 × 25 mm |
| Tailstock quill / travel / taper | 60 mm / 100 mm / MT4 | 75 mm / 150 mm / MT5 | 75 mm / 150 mm / MT5 |
| Existing model page | CK6140 ↗ | CK6150 ↗ | CK6160 ↗ |
Swipe to compare the three spindle packages.
The Chinese sheets and merged English catalogue contain different length, speed, tool and weight entries. This comparison uses the separate Chinese sheets rather than combining both versions. Obtain one dated specification for the exact quoted machine, bore, chuck, bed and controller; do not assume an older catalogue entry describes every available build.
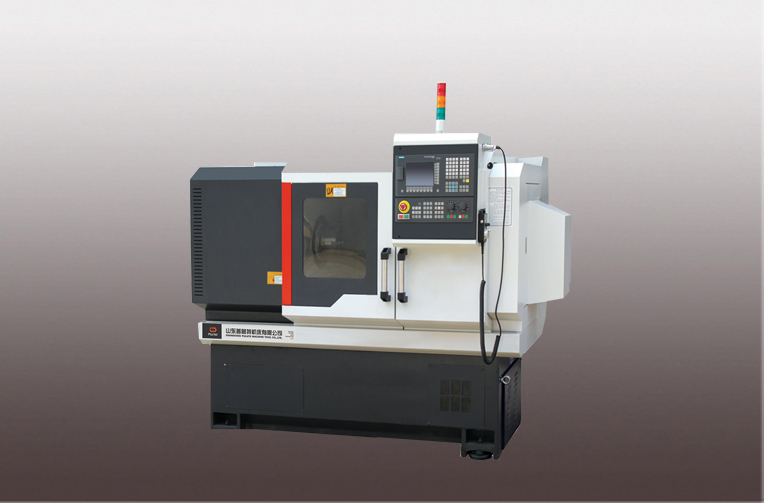
CK6140: check the short-part setup first
The model sheet lists conventional 200/250 mm chuck choices, a four-position electric toolpost and manual tailstock. Its 240 mm swing over the slide is the useful second clearance check after the 400 mm bed swing. Send the installed jaws and protruding blank dimensions, not just finished diameter.
The English combined table lists a different speed range and additional lengths. Keep those figures separate from this Chinese sheet's 2000 rpm ceiling and 420/650 mm machining-length entries.
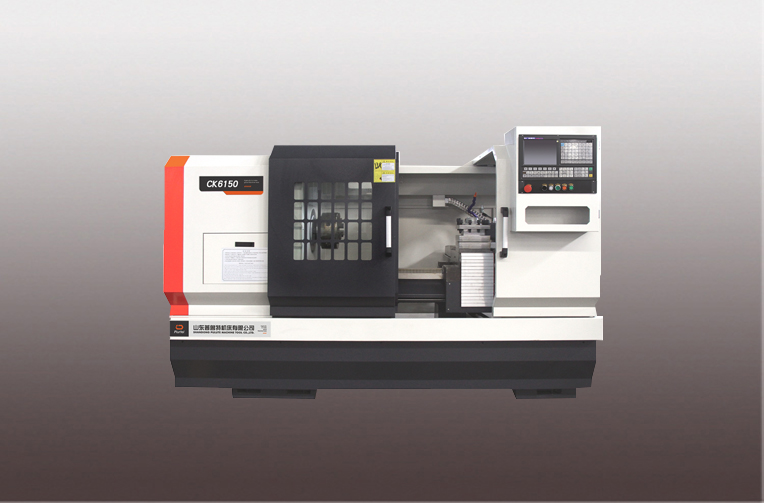
CK6150: the larger bore changes speed and chucking
The 82 mm spindle package is paired with a conventional 250 mm chuck; the 130 mm package with a 380 mm chuck. The sheet lists 1800 and 800 rpm ceilings respectively. Choose for the stock and cutting-speed requirement together, rather than treating the larger bore as an upgrade with unchanged spindle behavior.
A separate optional 10-inch hollow chuck entry gives a 65 mm drawtube passage. That entry is not a promise that every 82 mm bore installation passes 82 mm stock. Request the exact assembled chuck/drawtube limit and safe bar support.
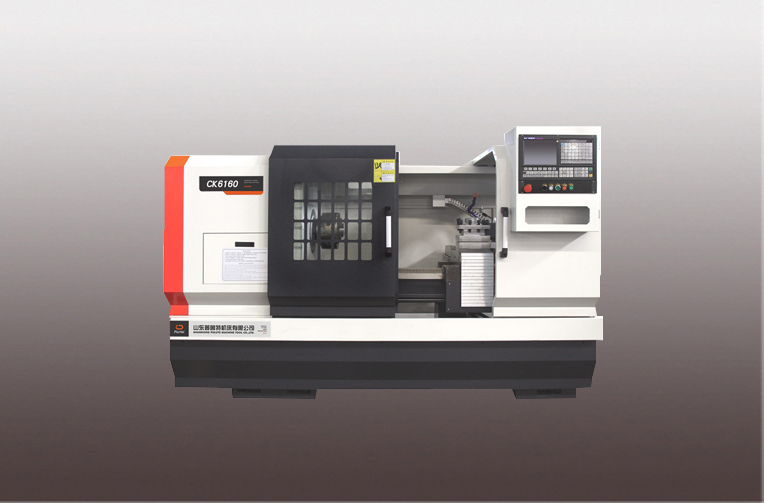
CK6160: more slide clearance, with turret conditions
The 395 mm slide swing is larger than CK6150's 250 mm entry. Its sheet separately lists 80/128 mm bar diameters for the 82/130 mm spindle bores. Use those actual passage figures as the starting point, then verify the ordered chuck, drawtube and feeding equipment.
Four tool positions are listed, with six/eight-position electric options. The sheet attaches 600/480 mm maximum disc diameters to the six/eight-position choices. Do not quote 600 mm disc capacity together with an eight-position turret without an interference drawing.
Keep center distance, cutting length and floor space separate
| Variant suffix | /1000 | /1500 | /2000 |
|---|---|---|---|
| Distance between centers | 1000 mm | 1500 mm | 2050 mm |
| Published machining length | 850 mm | 1350 mm | 1920 mm |
| Listed machine length × width × height | 2650 × 1650 × 1820 mm | 3150 × 1650 × 1820 mm | 3750 × 1650 × 1820 mm |
| Listed net mass | 2650 kg | 3060 kg | 3260 kg |
Swipe the three bed-length columns.
These are catalogue values for the named bed variants, not the space required to operate them. Add service access, door movement, stock support or feeder, loading route and chip/coolant handling to the installation plan. A /2000 suffix alone does not establish a 2000 mm usable cutting length.
For a supported shaft, supply the blank length and diameter, grip length, live-center projection and critical shoulder locations. Ask for a setup drawing showing tool travel to both ends, quill reserve and any steady-rest position. Confirm the specified manual tailstock or quoted hydraulic option and its pressure/force suitability for a slender part.
Accept a supported, released part—not a catalogue number
Freeze the workholding and tool list
Record jaw contact, centers or steady rest, clamping forces, stick-out, boring-bar reach and every tool station. The material, blank condition and bore package must match the intended production job.
Measure the complete operation
Include loading, tailstock engagement, roughing, finish passes, tool changes and any re-chucking. For long shafts, inspect taper and diameter along the length; for discs, inspect faces and concentric features against the agreed datums.
Inspect after releasing the fixture
Agree sampling, temperature, gauges and tolerances after unclamping. Include a second setup when both ends matter. A center-supported demonstration or axis resolution is not a finished-part tolerance guarantee.
Define the handover at your destination
Request foundation/loading drawings, total installed power and supply voltage/frequency, coolant/chip arrangements, controller and software versions, manuals and training language. State installation responsibility, spare parts, warranty scope and service travel arrangements in the quotation.
Company scope and the evidence used here
The official company page identifies Shandong Pulute Machine Tool Co., Ltd. (山东普鲁特机床有限公司) in Tengzhou, Shandong, and describes machine-tool design, development, manufacture and sales. Its catalogue also covers slant-bed and heavy horizontal lathes, machining centers, gantry equipment and turning/milling machines. This page compares the three existing CK references; it does not represent the full catalogue as reviewed model coverage.
The national standards platform lists this exact company among the drafting organizations for GB/T 9061-2025, general specifications for metal-cutting machine tools, published 5 October 2025 and effective 1 May 2026. That record establishes a drafting role; it does not certify a particular CK model or prove the ordered machine has passed an acceptance test.
Machine figures and pictured configurations come from the reviewed manufacturer material. Workholding, trial and handover guidance is CNCVerified's editorial analysis. Current configuration and legal supplier details belong in the actual purchase agreement.
Send the blank and holding plan
Attach the part drawing, material, blank diameter/length, grip and support plan, bore or bar-feed requirement, tool list, bed variant, batch target and released-part acceptance method. Include installation destination and the controller/service package you need.
Send Pulute RFQ ↗