
爱派尔(常州)数控科技有限公司
Jintan, Changzhou, Jiangsu
EMPIRE MV: plan the production fixture
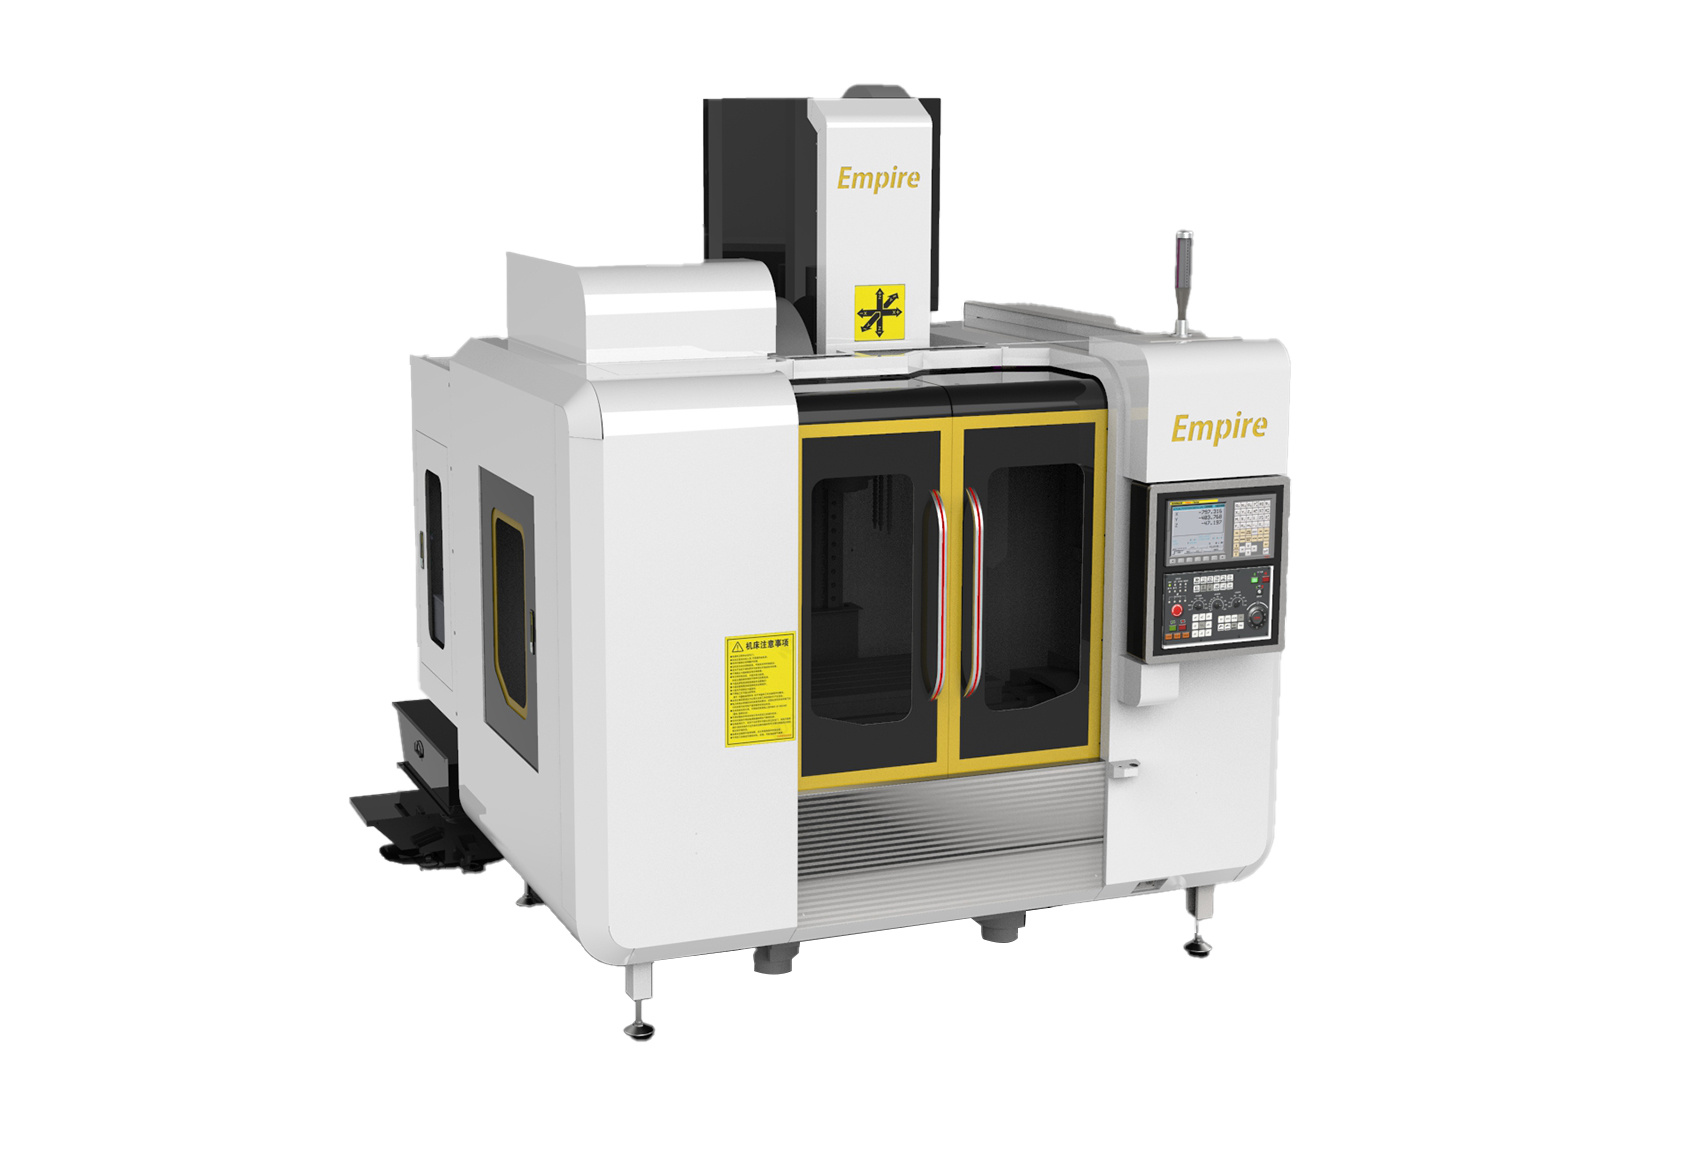
Compare EP-MV855L and EP-MV1160L by fixture length, loaded mass and tool access. More X travel does not mean a wider table.
Official company and MV catalogue reviewed 8 October 2026
Start with the fixture, not the catalogue size
A compact fixture with frequent tool changes
Check the EP-MV855L against the loaded fixture and every tool approach. Its 800 mm X travel and 500 kg listed table load are starting limits, not a finished-part envelope. Include vises, clamps, pallets and the blank in the load calculation.
A longer part or several stations
EP-MV1160L increases X travel to 1100 mm and listed load to 800 kg. Its table is 200 mm longer but still 550 mm wide. Ask for a supported fixture layout, permitted mass distribution and access at both ends; an overhanging blank is not validated by travel alone.
For either route, identify the datums that must stay in one setup. Submit the fixture height and longest assembled tool, then verify spindle-nose clearance, tool changes and retracts. If the job needs continuous five-axis motion or horizontal access, request an appropriate separate family rather than treating the MV page's general multi-axis wording as an included rotary system.
Read the two existing MV entries side by side
| Job constraint | EP-MV855L | EP-MV1160L |
|---|---|---|
| X / Y / Z travel | 800 / 550 / 550 mm | 1100 / 600 / 600 mm |
| Table length × width | 1000 × 550 mm | 1200 × 550 mm |
| Listed table load | 500 kg | 800 kg |
| Table to spindle nose | 120–670 mm | 120–720 mm |
| T-slots: count, width, spacing | 5; 18 mm; 90 mm | 5; 18 mm; 100 mm |
| X / Y / Z rapid movement | 48 / 48 / 48 m/min | 36 / 36 / 36 m/min |
| Published cutting-feed range | 1–10000 mm/min | 1–8000 mm/min |
| Spindle motor power | 7.5 kW | 11 kW |
| Machine mass | 3600 kg | 4800 kg |
| Machine length × width × height | 2700 × 2450 × 2350 mm | 3050 × 2550 × 2520 mm |
| Existing model page | EP-MV855L ↗ | EP-MV1160L ↗ |
Swipe the table on a narrow phone.
The 1160L has 50 mm more Y travel but no increase in table width. Its maximum listed rapid and cutting-feed values are lower than the 855L's; neither value predicts a completed production cycle. Check cutting conditions, axis acceleration, tool changes and handling against your actual program.
Specify the whole cutting and chip-removal package
Spindle and tool chain
Both model columns list BT40, direct/belt connection alternatives and 12000/8000 rpm entries. Ask which drive, speed and motor package is offered, with its torque curve and duty rating. Do not assume every alternative is standard or simultaneously available.
The disc magazine lists 24/30 positions. Supply tool/holder length, diameter and mass, including any heavy boring tools. Confirm occupied-position rules, access near the fixture and the exact controller; FANUC, Mitsubishi, Siemens, Huazhong and Syntec are listed as controller alternatives.
Chips, coolant and daily access
The MV description specifies twin side screw conveyors and a coolant tank, with a chain-type chip elevator and chip cart available as options. Define chip form, material, coolant and unattended-run requirement so the quote includes the right removal and filtration arrangement.
Check where the chip cart, coolant equipment, cabinet doors and maintenance access sit in the final layout. Catalogue machine dimensions do not include every service clearance or auxiliary. Specify any abrasive-material protection separately.
The manufacturer describes HT300 castings with secondary ageing after rough machining, heavy-duty roller guides, spindle oil cooling and protective enclosure arrangements. Treat these as published design features; use a loaded cutting trial to establish the result for your part.
Accept a repeatable production job
Lock the setup and cycle
Use the quoted machine, controller, spindle, fixture and complete tool list. Run the difficult features as well as the easy ones, including any second setup. Record loading, probing if specified, tool changes, spindle acceleration, cutting, cleaning and unloading in the cycle definition.
Measure the released part
The MV table gives ±0.006 mm positioning and ±0.004 mm repeat-positioning accuracy. These are machine-axis specifications, not a guarantee for finished dimensions. Agree part datums, thermal condition, instruments, sampling and measurement after unclamping where fixture distortion matters.
Make installation and handover explicit
Listed electrical demand is 20 kVA for 855L and 25 kVA for 1160L; both require air pressure of at least 6 kgf/cm². Obtain voltage, frequency, air flow, cooling and all auxiliary loads for the actual package. Retain the accepted program, offsets, fixture/tool records, test report and destination commissioning requirements.
If the order includes automation, filtration, refrigeration or MES software, give each its own interfaces and acceptance criteria. A successful machining test does not prove unattended recovery, robot interlocks or traceability integration.
The Changzhou manufacturer within EMPIRE
The official site identifies 爱派尔(常州)数控科技有限公司 in Jintan, Changzhou. It describes EMPIRE's progression from trading to manufacturing, with Shenzhen, Changzhou and Hunan operations. Its stated 2006 origin belongs to the group story; the site's timeline identifies Changzhou CNC production in 2017.
The current catalogue includes MV vertical machining, horizontal and vertical-horizontal machining, gantry and five-axis families, blade machines and drilling/tapping equipment, alongside chip-handling, industrial cooling and digital/automation offerings. This profile compares the two existing MV model entries; their figures are not transferred to those other families.
The Changzhou machinery-industry talent-survey notice published 12 May 2021 lists the exact Changzhou company in Jintan at annex 1, entry 10. It supports the dated corporate and industry cross-check, not current machine certification. The fixture, configuration and acceptance guidance here is CNCVerified's editorial analysis.
Confirm the contracting entity and who supplies commissioning, training, spare parts and warranty at your destination. A group-wide capability description is not a service commitment for a specific ordered machine.
Send the fixture and production job
Attach your drawing, material, blank, fixture dimensions and total loaded mass. Name the MV model, required features, complete tools, controller preference, batch and cycle definition, inspection criteria and destination. Include chip-handling and automation interfaces if they belong in the order.
Send EMPIRE RFQ ↗