
YANGTIE · 杨铁
Suzhou, Jiangsu
Yangtie EV: match the fixture and tool chain
Compare EV-1275 with BT40 against the larger BT50 EV-1380/1580. Start with loaded-fixture size, tool mass and installation space.
Official company and EV model material reviewed 8 October 2026
Choose the envelope before choosing the larger model
The EV family is presented as a three-axis linear-guide range. These three catalog columns differ in Y travel, spindle interface, loaded-table capacity and rapid movement. A larger table does not establish a shorter production cycle.
| Selection input | EV-1275 | EV-1380 | EV-1580 |
|---|---|---|---|
| X / Y / Z travel | 1200 / 750 / 600 mm | 1300 / 800 / 700 mm | 1500 / 800 / 700 mm |
| Table width × length | 700 × 1300 mm | 800 × 1400 mm | 800 × 1600 mm |
| Table load | 800 kg | 1300 kg | 1500 kg |
| Nose to table | 120–720 mm | 160–860 mm | 160–860 mm |
| Spindle interface / speed | BT40 / 8000 rpm | BT50 / 8000 rpm | BT50 / 8000 rpm |
| Listed maximum tool mass | 8 kg | 15 kg | 15 kg |
| X / Y / Z rapids | 24 / 24 / 20 m/min | 20 / 20 / 15 m/min | 18 / 18 / 15 m/min |
| Dimensions | 3600 × 3110 × 2900 mm | 3600 × 3200 × 3000 mm | 4300 × 3200 × 3200 mm |
| Machine mass | 8 tonnes | 9.5 tonnes | 11 tonnes |
| Existing model pages | EV-1275 details ↗ | EV-1380 details ↗ | EV-1580 details ↗ |
Swipe the comparison on a narrow phone.
The catalog's 24(32)-position magazine row is marked optional. Its spindle-motor row is a recommended selection: 11–15 kW for EV-1275 and 15–18.5 kW for EV-1380/1580. Obtain the actual installed motor, duty rating and selected magazine in the quotation.
Build a loaded-fixture drawing, not just a part bounding box
Include what stays on the table
Add the blank, vise or fixture plate, clamps and any rotary equipment. Check their combined mass against the selected load entry. Provide the mass distribution and overhang; ask for the permitted arrangement rather than assuming the load applies everywhere on the table.
Check the complete approach
Show the datum height, tallest clamp and longest assembled tool. Travel and nose-to-table limits must both accommodate approach, cutting and safe withdrawal. The extra 100 mm of Z on EV-1380/1580 does not by itself prove clearance for a tall fixture.
For a long multi-station fixture, draw every station and tool-change clearance. For a wider individual part, compare the required Y access rather than table length alone. If neither arrangement fits, request a different family with its own reviewed envelope; do not extrapolate beyond these EV figures.
BT40 to BT50 changes the purchase beyond the spindle
Audit holders, cutters and storage together
List the assembled tools needed for the part. Check interface compatibility, pull studs, assembled mass, length, diameter and adjacent-pocket clearance against the selected magazine. EV-1275's 8 kg entry and the two BT50 models' 15 kg entries are tool limits, not cutting-force ratings.
A BT50 interface alone does not prove a particular material-removal rate. Ask for the spindle torque/power curve, recommended cutter and workholding for the actual material. Separate cutting feed from the rapid figures above.
Confirm control model, programming functions, postprocessor, coolant and any rotary-axis package as named items. A controller function or catalog family description is not evidence that its required hardware is included.
Make the trial answer both fit and production questions
Freeze the setup
Supply the revision-controlled drawing, material state, blank and fixture concept. Name datums, difficult features, tools and the inspection method. Confirm the tested machine, controller and option list.
Run the actual sequence
Include approach, tool changes, chip removal and unloading. For a multi-station fixture, measure the required features at each station. Record settings and separate cutting time from handling and inspection.
Agree what transfers to the destination
Collect the trial report, program/postprocessor, offsets, tool list and fixture documents. Define commissioning, training, backups and acceptance criteria on the delivered equipment. Require a foundation and service-space drawing; overall dimensions alone are insufficient.
Use the drawing's required dimensions and surface criteria for acceptance. Catalog travel, motor recommendations and a clean enclosure photograph do not establish finished-part tolerance or an agreed cycle time.
Yangtie's equipment and service scope
Official company material identifies 杨铁数控机床(苏州)有限公司, established in 2013, and describes CNC equipment development, design, production and sales alongside repair and parts activities. Its published range also includes horizontal and gantry machining centers, lathes, profile machines, drilling/tapping and engraving equipment. This page reviews the three EV models above; it does not claim that those other families have been fully assessed.
The original 2021 Jiangsu proposed technology-SME list names this exact company at entry 6885 in Suzhou. It is a historical proposed-list record, not a current certification, factory inspection or approval of an EV model.
For a new machine, identify the manufacturing and contracting entities, warranty, configuration and destination support. For repair or retrofit, identify the existing machine and controller, fault evidence, replacement scope, backups and post-work checks. These are different contracts; an EV new-machine specification cannot define a repair result.
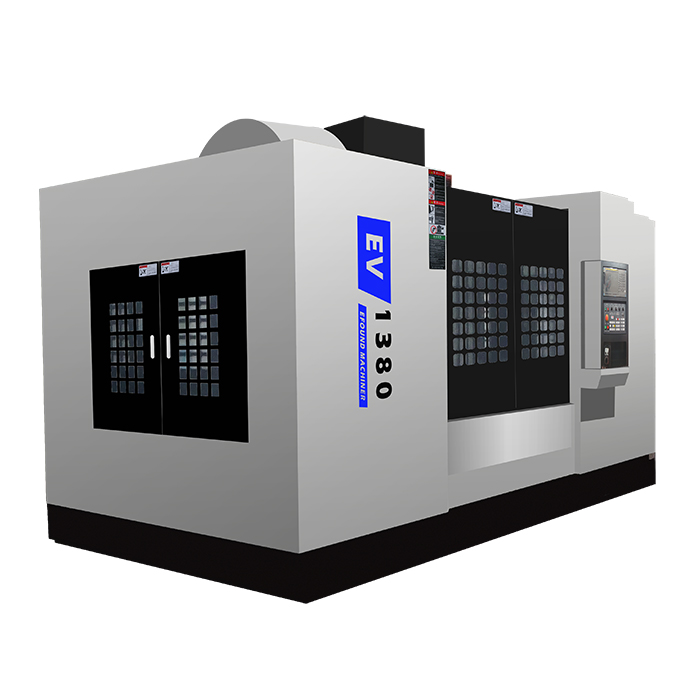
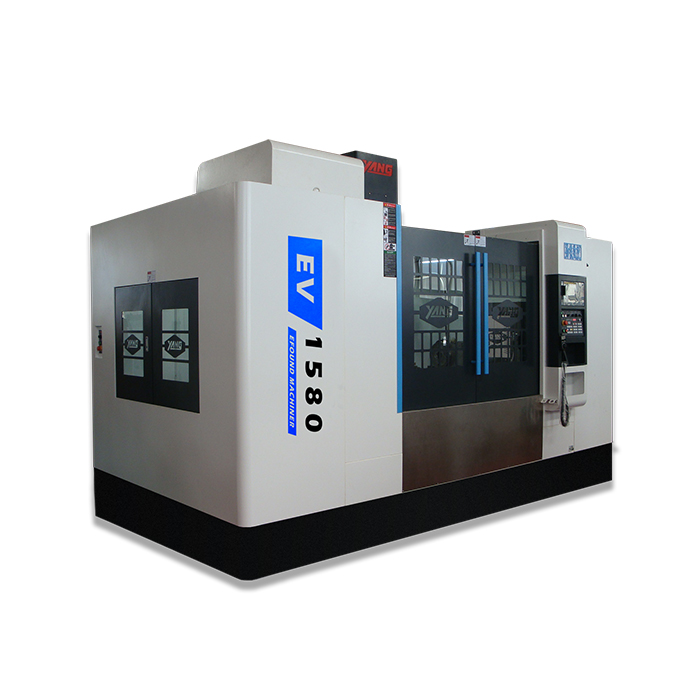
The fixture, tooling and trial guidance is CNCVerified's editorial analysis. The EV-1275 source page uses an image labelled EV-1270; this factory comparison therefore illustrates the accurately identified EV-1380 and EV-1580 instead.
Send the loaded fixture and tool list
State the preferred EV model, drawing revision, material, blank/fixture dimensions and combined mass. Add assembled tools, inspection criteria, batch requirement, installation site and destination. Say whether you need a new machine or service for an existing one.
Send Yangtie RFQ ↗