
JIER XK21
Gantry · JIER Machine-Tool Group Co., Ltd.
| Source/revision scope | XK21 series page dated 1 November 2020; offered build to confirm |
|---|---|
| Table width range | 2000–6000 mm |
| Table length expression | L = 2000 + n × 1000 mm; selected build to agree |
| Table load range | 5–25 tonnes/m; not total table load |
| Passage width / height ranges | 2600–6600 / 2000–6000 mm |
| W beam travel range | 1500–4000 mm |
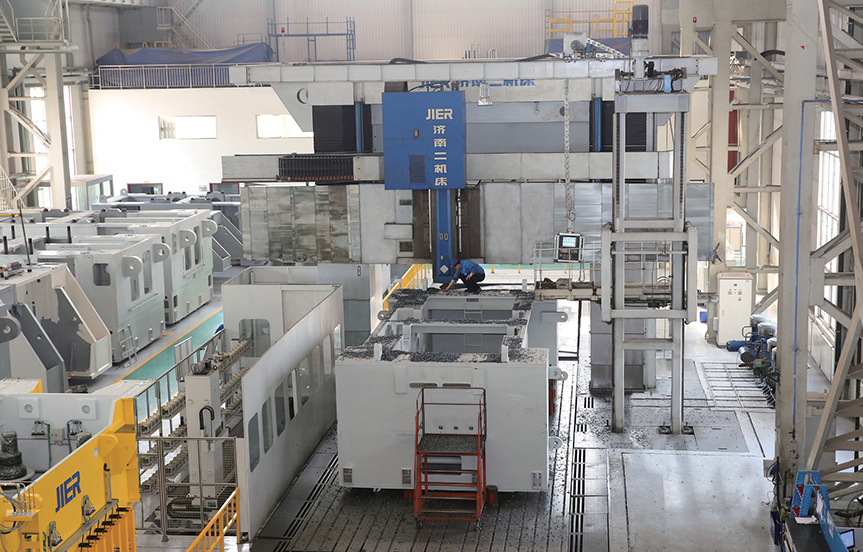
Whole original XK21 series image; illustrated configuration is not every build.
XK21 is a moving-beam gantry boring/milling series for large housings, plates and frames. The reviewed official page is dated 1 November 2020. Its ranges describe several configurations, not one machine with every maximum combined. Start with the loaded part and fixture, required faces and attachment-head approaches; agree the selected revision and complete working-envelope drawing.
Table width is listed at 2000–6000 mm, with length expression L = 2000 + n × 1000 mm. The table-load range is 5–25 tonnes per metre, not total load. Request the selected table’s distribution, point-load and fixture conditions. Passage width 2600–6600 mm and height 2000–6000 mm do not establish cutting access with the highest clamp or longest angle-head assembly.
W beam travel is 1500–4000 mm and ram travel 950–2000 mm. The manufacturer describes electrohydraulic proportional dynamic-balance compensation for W, along with boring/milling and attachment heads. Review tool extension and working stiffness for the critical cut. Spindle power 22–110 kW and maximum speed 1200–4000 rpm remain series ranges; obtain the actual torque/duty curve, head interface and control. Ambiguous X/Y typography in the rapid-motion line is left to the selected build sheet rather than used for a cycle claim.
Agree foundation, levelling, temperature, crane/loading and service access responsibilities before commissioning. Trial the tallest loaded setup and greatest required head/ram reach using the quoted material and tools. Inspect released bore/face datums and record head changes, loading, chips and restart separately from cutting. Request serial geometry and sample records; workshop component-capacity claims or compensation mechanisms do not certify the finished part.
| Same listing |
|---|
| TK/TH69 |