
LECROY / 力科 · 利联 catalogue record · Nantong, Jiangsu
Lilian / Like: fit the fixture, then choose the machine scale.
A hard-guideway VMC and a travelling-table gantry answer different workpiece problems. Compare the actual VMC850B and GMF3016 columns before choosing the load, tool and installation package.
Individual original product tables and the manufacturer's dated identity article reviewed 8 October 2026
Decide whether the problem is fixture size or long-workpiece access
- A contained fixture or housing
- VMC850B ↗
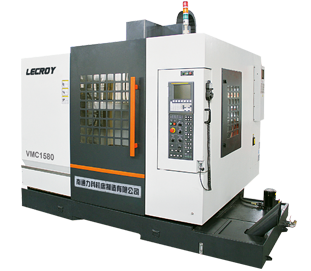
Its 1050 × 500 mm table and 800/500/500 mm travels are separate dimensions. Show the fixture, blank, toolholder and longest tool, then check spindle-to-table height through the required faces and holes.
- A long plate, base or mould
- GMF3016 ↗
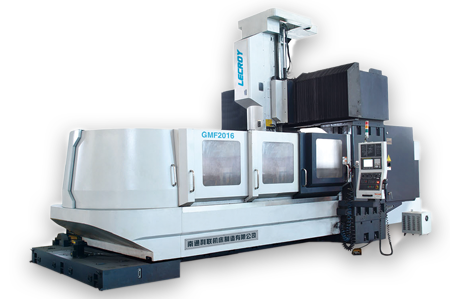
The 3000 × 1250 mm table, 1600 mm gate width and 3000/1600/900 mm travels answer different clearance questions. Include clamps and side tools inside the gate, with table movement and service access outside it.
The manufacturer's broader catalogue lists line-guideway VMCs, drilling/tapping centres, horizontal centres, CNC bed mills and conventional mills. Select those routes only against their own model documentation; a four-axis attachment or an automatic production cell is not established by either reference below.
VMC850B: the hard-guideway column, not the neighbouring VMC
The hard-guideway page describes plastic-lined rectangular sliding ways on X/Y/Z, hardened and scraped, with a herringbone column and rear-mounted motor. That is a machine construction description, not proof of a particular finish under heavy cutting. Match the actual duty, lubrication and thermal behaviour to the workpiece.
- Table / maximum listed load
- 1050 × 500 mm / 600 kg
- X / Y / Z travel
- 800 / 500 / 500 mm
- Spindle face above table
- 110–610 mm
- Spindle reference
- BT40, Ø120 mounting entry / 8000 rpm
- Disc magazine
- 24 positions; listed tool Ø80 × 120 mm, 8 kg
- Main motor entry
- 5.5 / 7.5 kW; duty mapping required
The original table uses merged cells: BT40/Ø120, 24 tools, Ø80 × 120 mm tool size, 8 kg tool mass and 5.5/7.5 kW belong to the 650B/850B pair. The 8000 rpm cell spans the first four models. The larger 1060B tool and motor entries must not be transferred to 850B.
Ask for the delivered magazine/holder drawing to confirm whether the unusually short 120 mm tool-length entry includes the holder and what clearance applies with adjacent pockets occupied. The listed 1.8 s is tool-to-tool change, not a part cycle. Travels, tool change and 18/18/15 m/min rapids do not establish output.
GMF3016: leave room for the fixture and the side operation
The exact GMF3016 column lists a 3000 × 1250 mm table with 12,000 kg maximum load, 1600 mm gate width and X/Y/Z 3000/1600/900 mm. The 150–1300 mm spindle-face-to-table range must be confirmed on the selected build: its 1150 mm span is different from the stated 900 mm Z travel. Request a dimensional drawing rather than resolving the difference by assumption.
For a long plate or mould, show clamps, packing blocks, fixture height and side faces. Check the farthest bore with its holder, any side head and the complete table stroke. Gate width is passage clearance; it is not usable machining width after fixtures and attachment offsets.
- Spindle / belt-head speed
- BT50, Ø190 mounting entry / 6000 rpm
- Rapid X / Y / Z
- 12 / 12 / 10 m/min
- Magazine / listed tool limits
- 24 positions / Ø110 × 300 mm / 18 kg
- Main motor entry
- 15 / 18.5 kW; duty mapping required
- Published machine mass
- 23,000 kg
- Published L × W × H
- 7500 × 4045 × 3870 mm
The technical table specifies roller linear guides on X/Y and a rectangular Z guide. The nearby family prose also describes a Z-linear-guide arrangement and optional all-gear drive. Do not combine those statements into one standard machine. Freeze the exact guide, drive, head and control package in the offer.
Keep attachments, controls and tool limits in one coherent build
VMC850B control and auxiliaries
The shared control line lists FANUC 0i mate-MD, Mitsubishi M70B, Siemens 828D and Syntec as alternatives. Some listed assemblies explicitly exclude the lubrication pump, coolant pump/tank, compressor or air/water separator. Ask for a complete supply boundary and the current control/drive revision, rather than treating the component list as a turnkey installation.
GMF3016 magazine and cutting duty
The table identifies FANUC 0i MF and pneumatic tool exchange, with BT50/24 tools. Show occupied pockets, adjacent-tool clearance, long boring bars and attachment handling. Clarify rated/peak motor duty and usable spindle torque for the material. The 7 m/min maximum cutting-feed reference is not a recommendation for every cutter.
Both records contain historical component/control names. Confirm current availability, substitution approval, backups, postprocessor and destination service in the delivered-build package. A family specification does not identify which individual factory, supplier or integrator owns each service obligation.
Trial the fixture—and prepare the site for the actual machine
Check the load as assembled
Count blank, fixture, clamps and attachments together. Ask how the maximum table-load rating applies to their distribution and overhang. For GMF3016, agree transport route, crane/lifting plan, foundation and the complete moving-table envelope. Its 23 t catalogue mass is not a shipping package or floor approval.
Measure the difficult feature after release
Trial the deep bore, far-end datum or heavy cut using the actual material and tooling. VMC850B lists 0.012 mm positioning and 0.006 mm repeat positioning; GMF3016 lists 0.021 and 0.02 mm respectively. Define the axis test standard, conditions and full travel separately from released-part form, size and datum acceptance.
Include all non-cutting time
Record warm-up, loading, fixture setting, roughing/finishing, tool or head changes, chip clearing and inspection across the agreed sample. Tool-to-tool time or rapid feed does not settle accepted output. For a long component, inspect the end-to-end result under agreed support and temperature conditions.
Confirm the utility boundary
The VMC850B table gives 20 kVA electrical capacity and air pressure ≥6 kg/cm². GMF3016 gives ≥6 kg/cm² and ≥0.5 m³/min air flow. Request current selected-build electrical, air quality/flow, coolant, guarding, access and maintenance requirements before installing equipment.
Put the exact company and service responsibilities on the order
The original article dated 16 January 2019 uses “南通力科机床制造有限公司(南通利联机床制造有限公司)” and the title “力科机床(利联机床)”. The website and LECROY mark use 力科, while this retained directory record uses 利联. This is evidence of the manufacturer's historical use of both names; it is not a current corporate-register extract or proof that two legal companies are interchangeable.
Confirm the contracting name, company identifier, builder/site and warranty provider for the quoted machine. The manufacturer's catalogue covers machining centres and mills and describes fixture, retrofit and integration support. Agree which work is included in this order and who supplies controls, attachments, training and destination service. Historical customer or certification statements are not current machine acceptance records.
Send the fixture drawing and the hardest feature
Include material, blank/fixture dimensions and combined mass, datums and tolerances, deepest or farthest feature, tool/attachment list, batch/output target, selected model/control, site utilities and installation destination. For GMF3016, show gate and table-stroke clearances; for VMC850B, show the longest tool and fixture height. Include the proposed legal seller in the quotation request.
Lilian / Like RFQ ↗