
台群精机 · Create Century group
Shenzhen · drilling and machining centres
Taikan: match the tool package to the part.
Compare compact BT30 drilling and tapping with BBT40 vertical machining. Check the loaded fixture and tool-pocket limits before choosing.
Compare the two routes ↓Taikan RFQ ↗
Original model material; August 2025 issuer record · reviewed 8 October 2026
Many small holes, or a larger machining setup?
Taikan is a machine-tool brand within the Create Century group. These two references answer different buying questions: T-500B combines drilling, tapping and milling for compact plate, disc and housing work; HT-V856S provides a larger vertical work envelope and a different tool interface and tool-load allowance. A faster spindle or a larger table does not settle which process is suitable.
| Check on your drawing | T-500B / English HT-500B | HT-V856S |
|---|---|---|
| Process to investigate | Compact drilling, tapping and milling; repeated hole/feature sequences | Plate, housing, valve or mould work needing more Z access and larger holders |
| X / Y / Z travel | 500 / 400 / 320 mm | 800 / 550 / 600 mm |
| Table / listed load | 620 × 400 mm / 250 kg | 1000 × 500 mm / 500 kg, evenly distributed |
| Nose-to-table window | 180–500 mm | 125–725 mm |
| Tool interface / listed speed | BT30 / 20–24000 rpm in the English table | BBT40 / 50–12000 rpm, directly coupled |
| Magazine / maximum tool mass | 21 / 3 kg | 24 / 7 kg |
| Maximum tool diameter, neighbours present / empty | 60 / 80 mm | 75 / 150 mm |
Swipe this comparison on a narrow screen. These are model-page references, not a capacity guarantee for a particular fixture or cut. T-500B configuration ↗ · HT-V856S configuration ↗
T-500B: make the hole sequence the trial.
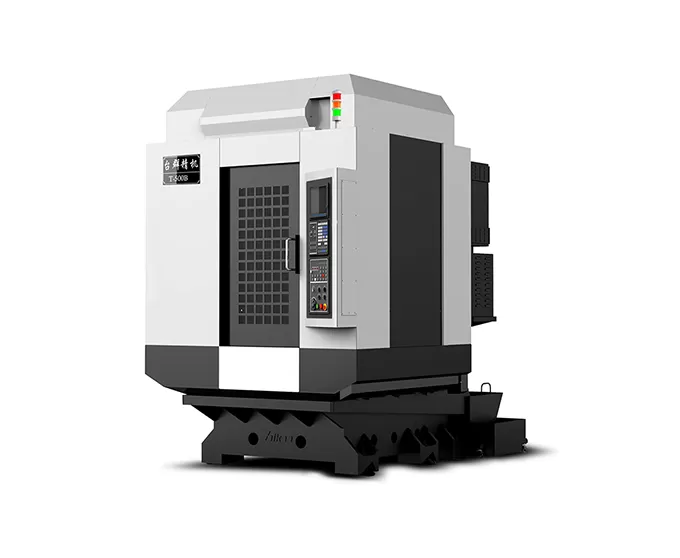
The Chinese catalogue calls it T-500B; the English product table uses HT-500B, while its headings and original image also use T-500B. Keep that naming difference in the quotation and confirm the offered revision. The English table lists Mitsubishi M80VA, BT30, 21 tools and 48 m/min rapid motion on each linear axis.
A 1.1-second adjacent-tool change is a manufacturer claim for the described 21-tool arrangement, not a finished-part cycle. A programme also includes approach/retract, spindle reversal, dwell, probing, chip clearing and loading. Time the actual drill/tap sequence with your material and tools, including the thread inspection and any tool-life intervention.
The English table lists 3.7/5.5 kW and 14.1/21 Nm as rated/short-time pairs. The short-time duration and speed-dependent torque curve still belong in the build sheet. A 24000 rpm entry does not establish that torque at maximum speed, or suitability for a large tap. The Chinese application material also contains a 20000 rpm description; agree the spindle revision rather than combining both descriptions.
Count occupied pockets before buying more nominal tools.
The reviewed table allows 300 mm tool length, 3 kg mass and 60 mm diameter with all adjacent tools present, versus 80 mm with adjacent pockets empty. Larger tools can reduce usable capacity. Chinese material describes 21/26/30/40-tool alternatives; those alternatives do not make the reviewed 21-tool build a 40-tool machine. Submit the full holder lengths, masses and pocket map.
Check the 180–500 mm spindle-nose window with the fixture, part, drill/tap holder and safe change position. The table’s 250 kg limit includes the loaded setup; ask for distribution and centre-of-gravity conditions. For repeated thin parts, prove clamping support and the released feature, rather than accepting an unloaded positioning figure as a part tolerance.
HT-V856S: use the extra Z with a complete holder and clamp plan.
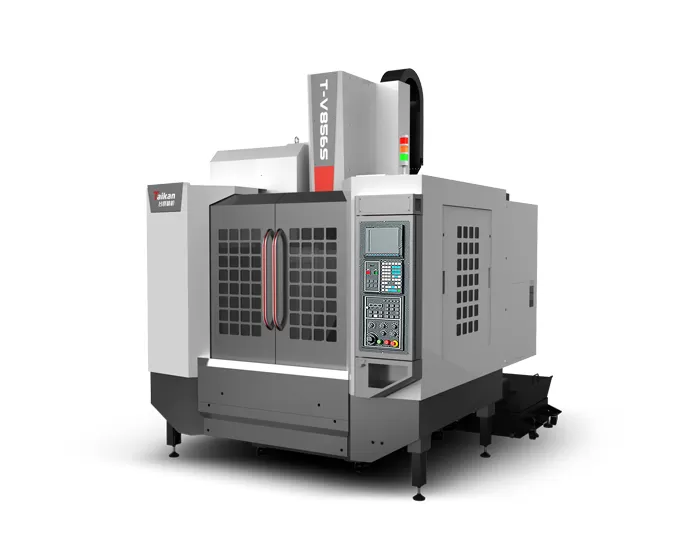
The English S-series page describes a fixed-column, cross-table machine with three linear guide axes. Its 800/550/600 mm travel and 125–725 mm nose-to-table window provide different setup references from T-500B. A 1000 × 500 mm table does not mean every part of that size can be reached in one clamping, particularly with a raised fixture or a long boring tool.
The listed spindle is directly coupled, 50–12000 rpm, with BBT40 interface and P40T-I (MAS403) retention-stud reference. Confirm compatible holders and studs with the supplier; do not transfer the BT30 tool package from the drilling centre. Rated/short-time motor entries are 7.5/11 kW and 35.8/95.5 Nm. Ask for the actual spindle curve and duty conditions for the planned roughing cut.
The 24-tool magazine permits 7 kg mass, 250 mm length and 75/150 mm diameter with neighbours present/empty. A large face mill or long boring assembly may occupy surrounding pockets. Reserve capacity for sister tools, probes and the real machining sequence. Mitsubishi M80VB is the control named in this table; a generic gallery of controller brands does not specify the offered build.
The 500 kg table load is explicitly described as evenly distributed. The buyer still needs a loaded-fixture review, safe access to each datum and a machining trial. Neither rapid traverse nor the larger interface alone proves a stable heavy cut.
Review the setup in three passes.
Clamping and reach
Send the part plus base plate, clamps, locators and complete holders. Identify the lowest cutting feature, highest obstruction and tool-change clearance. Ask for the working-envelope drawing and safe toolpath review; keep machining stroke separate from nominal table area.
Cutting and non-cutting time
For T-500B, include spindle reversal and thread quality in the repeated-hole trial. For HT-V856S, include roughing load, chip removal and the longest finishing holder. On either route, separate time in cut, traverse, tool change, measurement and manual handling. Do not estimate a parts-per-hour promise from the shared 48 m/min rapid figure.
Utilities and physical access
The English references list T-500B at 15 kVA with air flow at least 200 L/min ANR, and HT-V856S at 25 kVA with at least 280 L/min ANR; both list 0.6–0.8 MPa air. Obtain the actual electrical diagram, voltage/frequency, air-quality requirement and simultaneous demand. Catalogue body sizes exclude whatever extra service, conveyor, door and loading clearance the delivered layout needs.
Accept the thread or datum, not just the machine motion.
Use the offered control, spindle, fixture, tool package and coolant arrangement on a representative part. Agree material/blank condition, warm-up, cutting programme, tool life and measurement method before quoting a cycle.
A compact drilled/tapped part
Choose the deepest or smallest critical hole and the thread that challenges spindle reversal or chip clearance. Inspect hole location, thread gauge result, burrs and surface after unclamping. Repeat with the planned fixture loading and include the procedure for a worn or broken tap.
A housing, plate or mould setup
Choose the longest holder, a bore/deep feature and the datum relation that requires a second setup. Measure after release and re-clamping. Include roughing/finishing conditions, chips and coolant, loading access and restart after a controlled interruption.
The HT-500B English table gives 0.006 mm positioning and 0.004 mm repeatability with a full-travel GB/T 18400.4 reference. That is a published machine-test entry, not proof of the same tolerance on a thread or finished housing, and it is not transferred to HT-V856S. Request serial-machine test records and the agreed part-inspection result.
Separate the brand, manufacturing site and delivery responsibility.
The group publishes Taikan among its brands, with a Shenzhen headquarters and manufacturing bases in Dongguan, Suzhou, Huzhou and Yibin. The August 2025 issuer filing identifies 广东创世纪智能装备集团股份有限公司, code 300083, and lists 深圳市创世纪机械有限公司 as its wholly owned equipment subsidiary at that date. The filing confirms that relationship; it does not certify either model or independently inspect a production site.
Ask which legal entity sells, assembles and services the offered serial machine, where it is produced and what is included in destination commissioning. Confirm parameter/PLC backups, control options, programming and maintenance training, warranty handling and spindle/toolchanger spares. A group-wide service-network description is not an agreed local response time.
The broader group catalogue includes profile, horizontal, gantry and five-axis machines. Their capabilities are not added to these two references. Revised spindle packages, automation and extra axes need their own build-specific review.
Send the hole list and loaded setup with the drawing.
Include material and blank, hole/thread sizes and depths, datums/tolerances, batch and production mix, loaded fixture dimensions/mass, complete holders and tool-pocket map. Identify the critical cycle or finish requirement and the installation country, power and air supply.
Ask for the exact T/HT model revision, spindle/control package, fixture-reach review, itemised accessories, accepted sample programme and destination support scope through CNCVerified.
Prepare a Taikan RFQ ↗