
Hotman GP32
Grinding · Guangdong Hotman Machine Tool Co., Ltd.
| Maximum grinding diameter | 320 mm |
|---|---|
| Maximum swing | 320 mm |
| Distance between centers | 600 mm |
| Workpiece load between centers | 90 kg |
| Workhead load | 20 kg |
| Maximum wheel peripheral speed | 45 m/s |
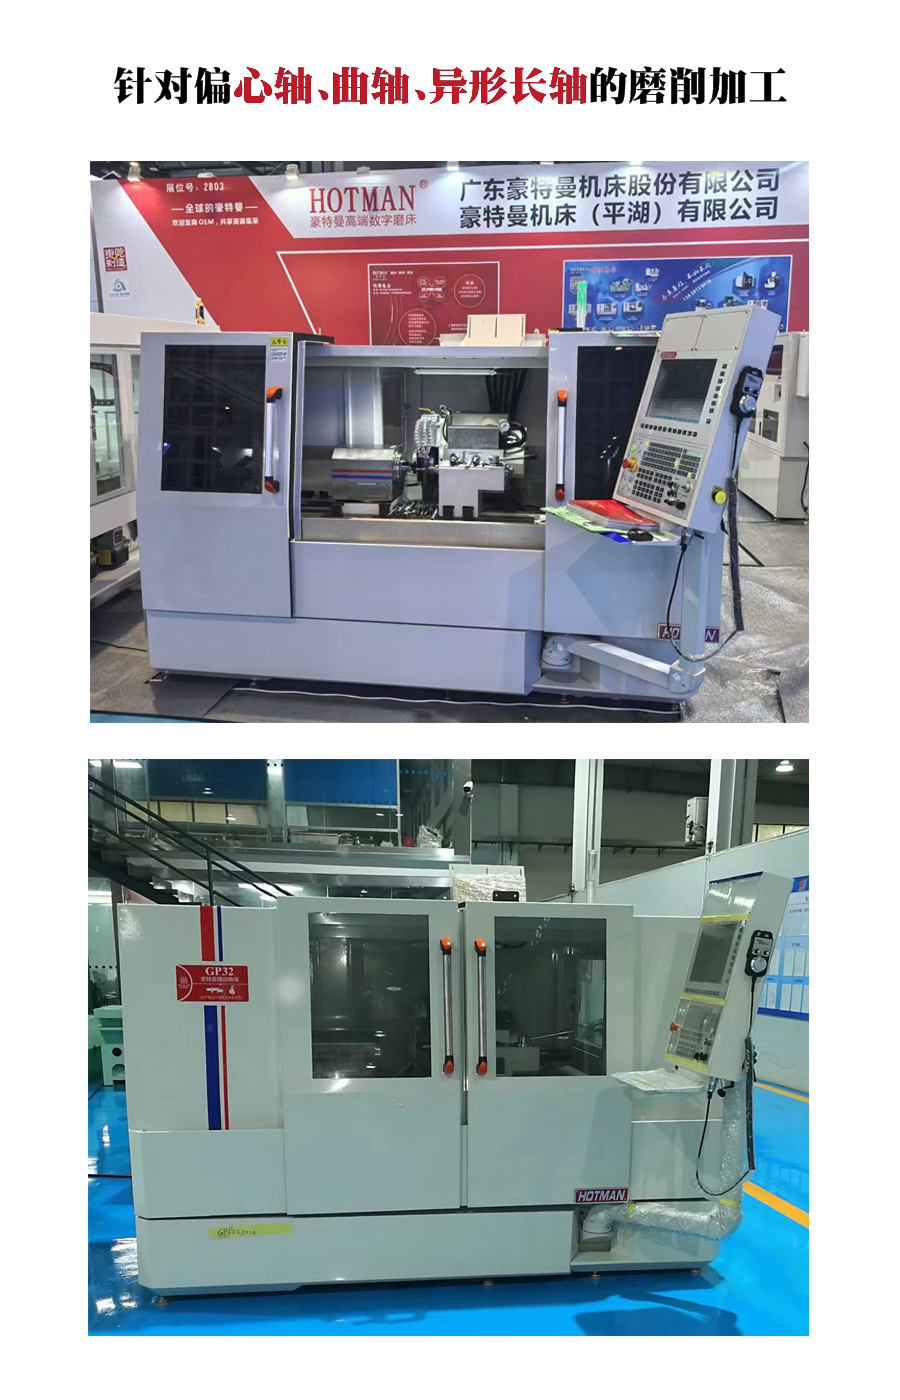
Whole original GP32-page image marked GP32CBN. Confirm the quoted wheel and machine configuration; the pictured CBN package is not universal.
Hotman GP32 is a follower-type grinder for eccentric shafts, crankshafts and elongated non-circular profiles, with cylindrical grinding also described. Its table lists 320 mm maximum swing and grinding diameter, 600 mm distance between centres, and separate loading limits of 90 kg between centres and 20 kg at the workhead. Choose the appropriate support reference and check the complete eccentric profile, shoulders, fixture and wheel approach instead of treating these figures as an unrestricted part envelope.
The construction description includes a direct-drive workhead, linear-motor wheelhead feed, a hydrostatic/dynamic-pressure grinding-wheel spindle and linear-scale feedback. Define the profile file, angular phase datum, compensation and dressing method for the required coordinated motion. Encoder or scale resolution does not establish a finished profile tolerance; retain the exact part and measurement method with the trial.
The GP32 table gives 260 mm X stroke, workhead speed up to 600 rpm, MT4 workhead and tailstock interfaces and 40 mm tailstock-quill travel. Wheel references are 450 × 127 × 50 mm or 405 × 203 × 50 mm, with 45 m/s maximum peripheral speed. Confirm abrasive, bore, width, mounting and permitted speed together. The official image is marked GP32CBN, documenting that pictured configuration rather than making a CBN package standard for every order.
Provide material and heat treatment, stock allowance, support plan, profile/phase and journal relationships, surface-integrity requirements and accepted output. Run the difficult curvature and shoulder with the quoted wheel, then repeat after dressing; inspect the released part and include handling, measurement, rejected work and any second operation. Agree warm-up, filtration and temperature control, program/profile backups, wheels/dressers and destination commissioning.
| Same listing |
|---|
| Z850 |