
Jiangnan JN-IV850
3-axis machining · Jiangnan CNC Machine Tool Co., Ltd.
| X / Y / Z travel | 800 / 500 / 500 mm |
|---|---|
| Table size / load reference | 1000 × 500 mm / 500 kg |
| Spindle nose to table | 150–650 mm |
| Spindle interface | BT40 |
| Web A spindle reference | 12,000 rpm direct drive / 7.5 kW (duty rating not stated) |
| Web B spindle reference | 8000 rpm belt drive / 11 kW (duty rating not stated) |
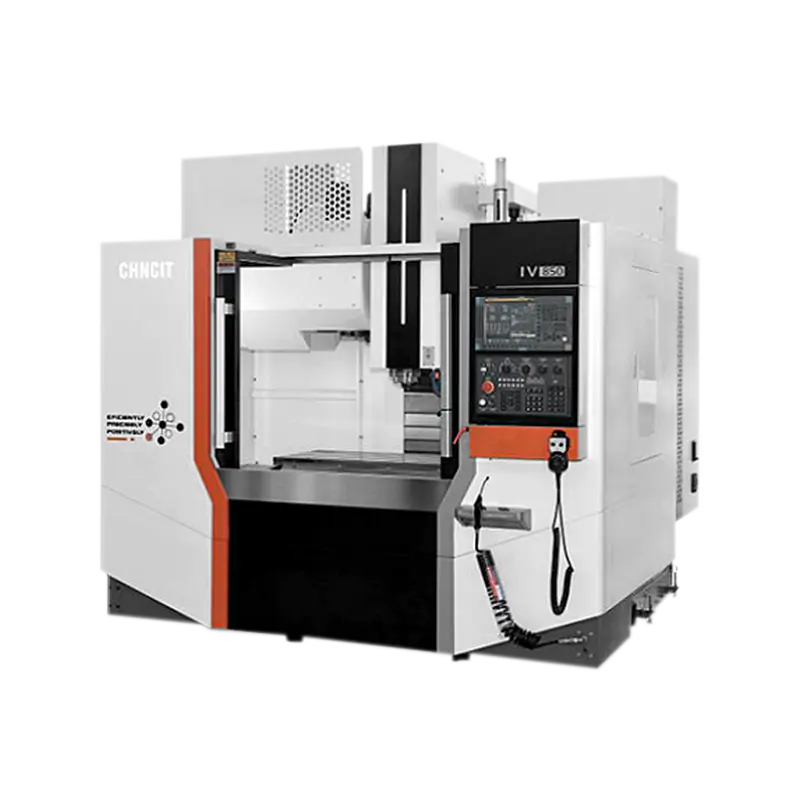
Whole matching original JN-IV850 photo; selected control, spindle and accessories to agree.
JN-IV850 is Jiangnan’s BT40 vertical machining-centre reference with 800 × 500 × 500 mm X/Y/Z travel. The table is 1000 × 500 mm with a listed 500 kg load reference, and spindle nose to table is 150–650 mm. Compare the complete housing fixture, total mass/offset and longest cutter assembly. Include access to a deep pocket or shoulder, tool withdrawal and the clearance around the tallest clamped part; this envelope is not a guarantee of milling performance or permitted eccentric loading.
The manufacturer’s web table separates A and B: A is a 12,000 rpm direct-driven spindle with 7.5 kW; B is an 8000 rpm belt-driven spindle with 11 kW. The linked technical file describes Mitsubishi M80B and the 8000 rpm/11 kW belt-drive build. Power duty is not defined, so these values are not labelled continuous or peak. Obtain the quoted spindle torque curve and a single dated reference. The file gives 48 m/min rapids versus 36 m/min on the web, 5000 kg versus 4500 kg, and different body dimensions. Those discrepancies cannot be resolved by choosing the fastest or lightest number.
The 24-tool reference needs confirmation of contracted standard versus option scope. The web table allows Ø80 mm occupied tools and Ø150 mm with neighbouring space empty; the belt-drive file gives Ø78/150 mm. Confirm the selected revision before loading the magazine. Both references give 250 mm length and 7 kg mass limits and a 2.5 s tool-to-tool time. Add withdrawal, approach, probing and chip clearing to any complete cycle estimate. Define the actual chip conveyor, through-spindle coolant, probing, automatic door and control package, including permitted supplier substitutions.
For acceptance, machine the demanding pocket, datum relationship or thin wall with the intended projection and material. Record thermal conditions, wear, tool changes and complete elapsed time, then inspect the released part where distortion matters. Keep static machine-geometry records separate from part results. Use the selected version’s footprint for foundation and handling, with extra service/tank/door clearances agreed explicitly. The whole original photograph is marked IV850; it represents the model and does not independently prove the selected direct/belt drive or accessory configuration.
| Same listing |
|---|
| JN-T500 |