Anyang Xinsheng turning
Anyang Xinsheng CK61160 (32/63 t)
Anyang Xinsheng Machine Tool Co., Ltd. · Anyang
- Workpiece mass alternatives32 tonnes or 63 tonnes; supported setup to approve
- Swing over bed / carriage1600 / 1250 mm, both configurations
- Workpiece-length choices4000–20,000 mm; selected bed, cutting reach to confirm
- Spindle motor alternatives75 kW (32 t) / 144 kW (63 t)
- Spindle speed alternatives0.8–160 rpm (32 t) / 0.5–125 rpm (63 t)
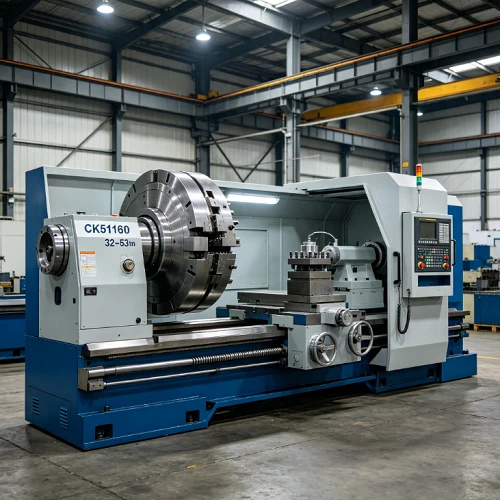
CK61160 is Anyang Xinsheng’s heavy horizontal CNC turning reference with separate 32-tonne and 63-tonne configurations. Both list 1600 mm swing over the bed and 1250 mm over the carriage, and workpiece-length choices from 4000 to 20,000 mm. Define blank mass, centre of gravity, fixtures, centre and rest positions before choosing the bed. The catalogue length range is not proof of uninterrupted cutting stroke with the tailstock, tools and supports installed.
The 32-tonne table lists a 75 kW spindle motor, 0.8–160 rpm, maximum 80 kNm spindle torque, maximum 80 kN cutting-force reference and 300 mm tailstock quill. The 63-tonne alternative lists 144 kW, 0.5–125 rpm, 120 kNm, 120 kN and 560 mm respectively. Select one coherent configuration. Maximum torque, speed and force are not simultaneously guaranteed at every operating point; obtain duty curves and an approved cutting plan for the material, engagement and overhang.
The source describes a three-guideway HT300 base, rack-and-pinion longitudinal feed, ball-screw cross feed and inlaid steel guides with automatic lubrication. The listed package includes FANUC 0i-TD, manual heavy four-jaw faceplate, four-station electric toolpost and an open steady rest for 650–1200 mm diameter. A smaller support journal needs its own arrangement. Closed rests, Siemens control, chip conveyor, external grinding head and live-milling attachment are options, with separate mounting, drive and acceptance scope.
Trial a representative loaded shaft using the intended lifting, rest and clamping plan. Include the difficult interrupted or low-speed cut, support adjustment, chip clearing and thermal routine, then inspect agreed datum relationships after release where appropriate. Request package-specific foundation reactions, alignment and maintenance access. A machine capability reference does not establish every rotor’s finished accuracy or a complete milling/grinding process. The whole original photograph carries the matching CK61160 32–63-tonne marking; the contracted configuration still requires confirmation.