
Baoji Zhongcheng: plan the bar-to-part process
Compare CK30E and CK46P from the stock and clamping arrangement, then check the gang-tool sequence and finished-part handling. Spindle-bore diameter alone does not establish bar capacity.
宝鸡忠诚精密数控设备有限责任公司 · Baoji, Shaanxi
Official company and both exact model pages reviewed 8 October 2026
First, separate bar stock from the turning envelope
For a bar-fed job, start with the usable stock diameter through the complete collet/drawtube system. For an individual blank, review its holding geometry and tool clearance separately.
| Production check | CK30E | CK46P |
|---|---|---|
| Bar capacity / spindle bore | 30 / 36 | 45 / 57 |
| Maximum turning diameter / length | 70 / 150 | 360 / 270 |
| Swing over bed / slide | 240 / 120 | 400 / 140 |
| Collet actuation | Pneumatic spring collet | Hydraulic hollow rotary cylinder, pull-back collet |
| Gang-tool arrangement | Dovetail plate | T-slot plate; eight holders listed |
| Spindle nose / maximum speed | A2-4 / 6000 rpm | A2-5 / 4000 rpm |
| Control listed | FANUC 0i-TF | GSK 988TA |
Swipe sideways for both model columns on a narrow phone.
Neither the 36/57 mm bore nor the maximum turning diameter increases the listed bar capacity. Submit the stock shape, size, straightness and collet engagement length for a workholding proposal.
Two different gang-tool setups
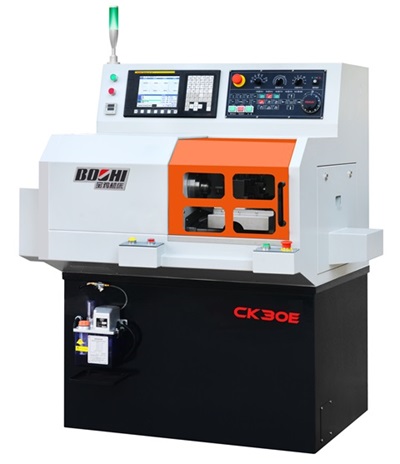
CK30E · compact small-component production
The integral flat bed pairs a pneumatic collet with a dovetail gang-tool plate. X/Z travels are 250 / 180 mm. Listed tool sizes are 12 × 12 mm for external turning and 25 mm for boring.
CK30E uses linear guides and 20 / 20 m/min rapid traverse. The related CK30 has hardened dovetail guides and 15 / 15 m/min; its figures should not be mixed into an E quotation. CK30E's spindle motor is 3.7 kW.
The manufacturer describes a stock-pulling arrangement on the tool plate. An optional Y-axis side-milling powered head needs a separate configuration and feature review.
See CK30E specifications ↗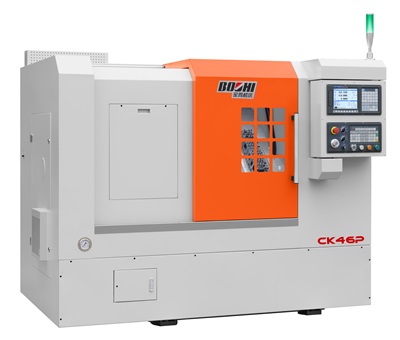
CK46P · larger stock and hydraulic workholding
The 45° slant-bed layout uses hydraulic collet actuation and a wider T-slot plate. X/Z travel is 400 / 400 mm; listed external tools are 20 × 20 mm and boring tools 25 mm.
The 5.5 / 7.5 kW motor figures need their duty conditions confirmed. The page offers side or rear chip-removal arrangements: locate the chip outlet, bin and maintenance access on the proposed cell drawing.
Its shared table also contains CK52P. Keep CK46P's 45 mm bar, A2-5 nose and 4000 rpm separate from CK52P's 51 mm bar and different spindle specification.
See CK46P specifications ↗Draw the sequence from bar to finished part
Load, advance and clamp
Identify bar length, end condition, support and feeding method. Agree collet opening, pull-back movement, grip length and clamp confirmation. CK30E's stock puller is not evidence that an external bar feeder or unattended cell is included.
Arrange tools around the actual cut
List facing, turning, drilling/boring, threading and cutoff in order. Show holder positions and tool projections on the gang plate; confirm approach paths and interference with the collet, stock and adjacent tools.
For cross features on CK30E, specify the optional powered head, its tools and spindle positioning requirements. An added side-milling head does not by itself establish a full five-axis or sub-spindle system.
Remove the part and clear the chips
Define cutoff support, catching/collection, deburring and any second operation. Agree feeder/controller interlocks, bar-end logic and recovery after an interrupted cycle. Locate coolant and chip access so the cell remains maintainable.
Approve the process using the real stock
Send representative stock and a drawing identifying critical diameter, thread, concentricity, surface finish and cutoff-length requirements. Run the agreed tool sequence with the proposed collet and feed method, then measure after the component is released.
Put these in the acceptance record
- Stock and material, tool/holder list, clamp setup, program revision and machine configuration.
- Measurement method and sample quantity for each critical feature.
- Complete cycle, including feed, clamp, cutoff and part collection; separately record manual tasks.
- Feeding/interlock operation, chip handling and agreed restart checks.
CK46P's product text mentions IT6 machining precision. This is a manufacturer claim without your component's complete test conditions; use agreed feature tolerances and measurement results as the purchase acceptance basis.
Before delivery, obtain site and utility drawings. The published CK30E mass is 1020 kg and dimensions 1319 × 1495 × 1805 mm; CK46P is 2800 kg and 2150 × 1640 × 2025 mm. Add feeder, door, chip-bin and service clearances to the installation plan.
Zhongcheng's turning and automation focus
The official company account identifies Baoji Zhongcheng Precision CNC Equipment as part of Baoji Machine Tool Group and describes development, manufacturing, sales and technical service for CNC lathes, mill-turn centers and automated machining units.
Its range includes gang-tool and turret machines. The two models reviewed here are gang-tool selections; a turret, mill-turn or automated-unit proposal requires its own model and configuration review.
Company and model facts above come from the manufacturer's material. The stock, tool-layout and acceptance sequence is CNCVerified's purchasing analysis. Request the exact contracting entity, configuration documentation, destination support and spare-parts responsibilities in the offer.
Send a bar-to-part production brief
Include stock diameter/length/material, part drawing, batch size, tool sequence, second operations and intended feeder/collection method. Add destination, utilities and the proposed trial acceptance. Ask for optional powered tooling and automation to be priced and identified separately.
Request a Zhongcheng quote ↗