
巨浪凯龙机床(太仓)有限公司 · CHIRON Group China
CHIRON: design the small-part process.
For Micro5 and Micro5 XL, start with the blank, fixture and tiny cutting tools. Then decide how five-axis access, tool space and automated loading work together.
Compare the two micro-machining routes ↓Prepare a CHIRON RFQ ↗
Original model pages, September 2026 technical sheets and company records reviewed 8 October 2026
More travel changes the fixture, not just the part size
CHIRON presents Micro5 for small medical, watch, jewellery and precision components, and Micro5 XL for an expanded micro-machining envelope. Both use five-axis machining. A flat blank fitting inside the linear travel still needs room for the fixture, tilted workpiece, tool and holder throughout the operation.
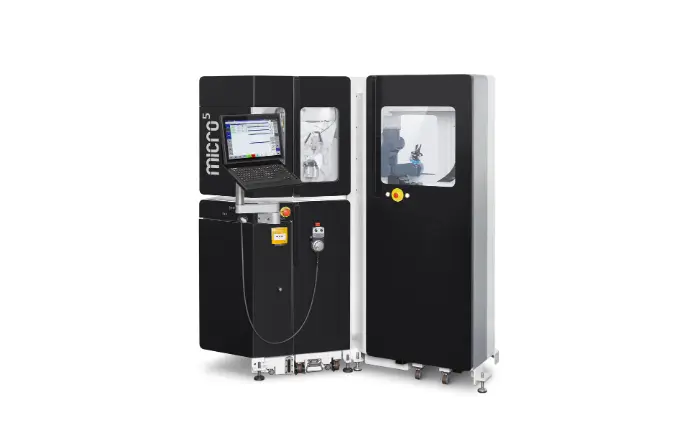
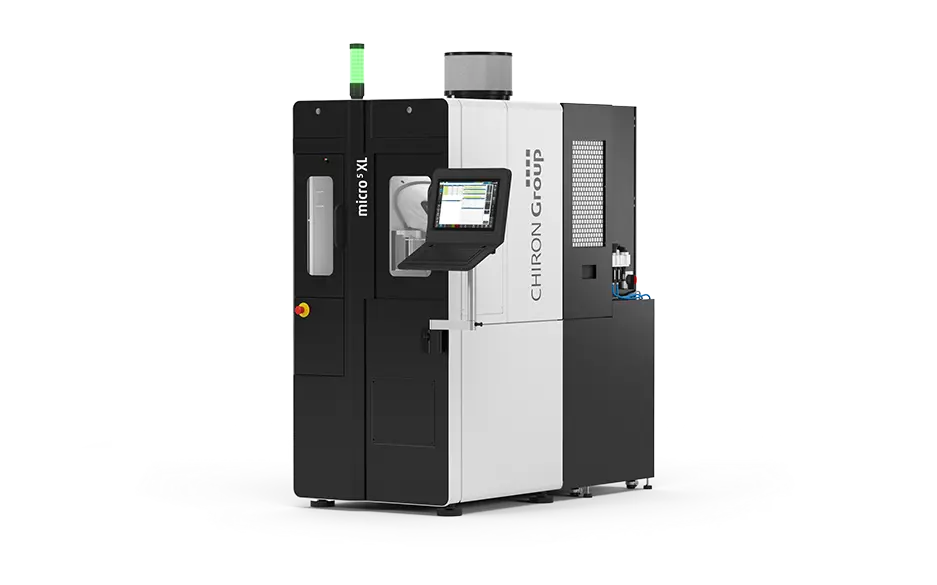
| Decision | Micro5 | Micro5 XL |
|---|---|---|
| X / Y / Z travel | 78 / 56 / 50 mm | 170 / 140 / 120 mm |
| Spindle interface | HSK-EZ15 | HSK-E25 |
| Spindle reference | Maximum 60,000 rpm | 40,000 or 50,000 rpm |
| Tool provision | Up to 60 tool options in sheet | 60 or 100 tools |
| Tool diameter | 18 mm; 40 mm with adjacent space clear | 30 mm; 65 mm with adjacent space clear |
| Chip-to-chip reference | 3.5 s | 3.9 s |
The sheets' axis travels are not a promise of that-sized workpiece at every rotary position. Bring the blank and fixture CAD, gripping surfaces and shortest safe tool projection into the collision study. The Micro5 page's 50 mm and XL page's 120 mm workpiece references also need the actual geometry and tilt checked.
Small tools need a different spindle conversation
Keep the torque units visible
Micro5's sheet gives maximum spindle torque 10.5 Ncm; XL gives 1.8 Nm. They use different units and interfaces. Neither sheet supplies a complete torque/power curve or duty at every speed. For a micro-drill, thin end mill or form tool, quote the actual material, diameter, engagement and holder rather than selecting on maximum rpm alone.
Plan occupied tool positions
The larger diameter allowance requires adjacent space to be clear. Count that lost capacity alongside roughing, finishing, drilling, sister tools and any measuring equipment. Match the approved tool assembly to the selected spindle interface and balance/speed limits; the magazine diameter is not permission to cut with any tool at maximum rpm.
A 3.5 or 3.9 second chip-to-chip reference is one change interval. The part cycle also includes positioning, five-axis motion, actual cuts, tool checks, cleaning, loading and inspection. Ask for the complete sequence with the proposed tools and fixture.
Prove the clean handover before running unattended
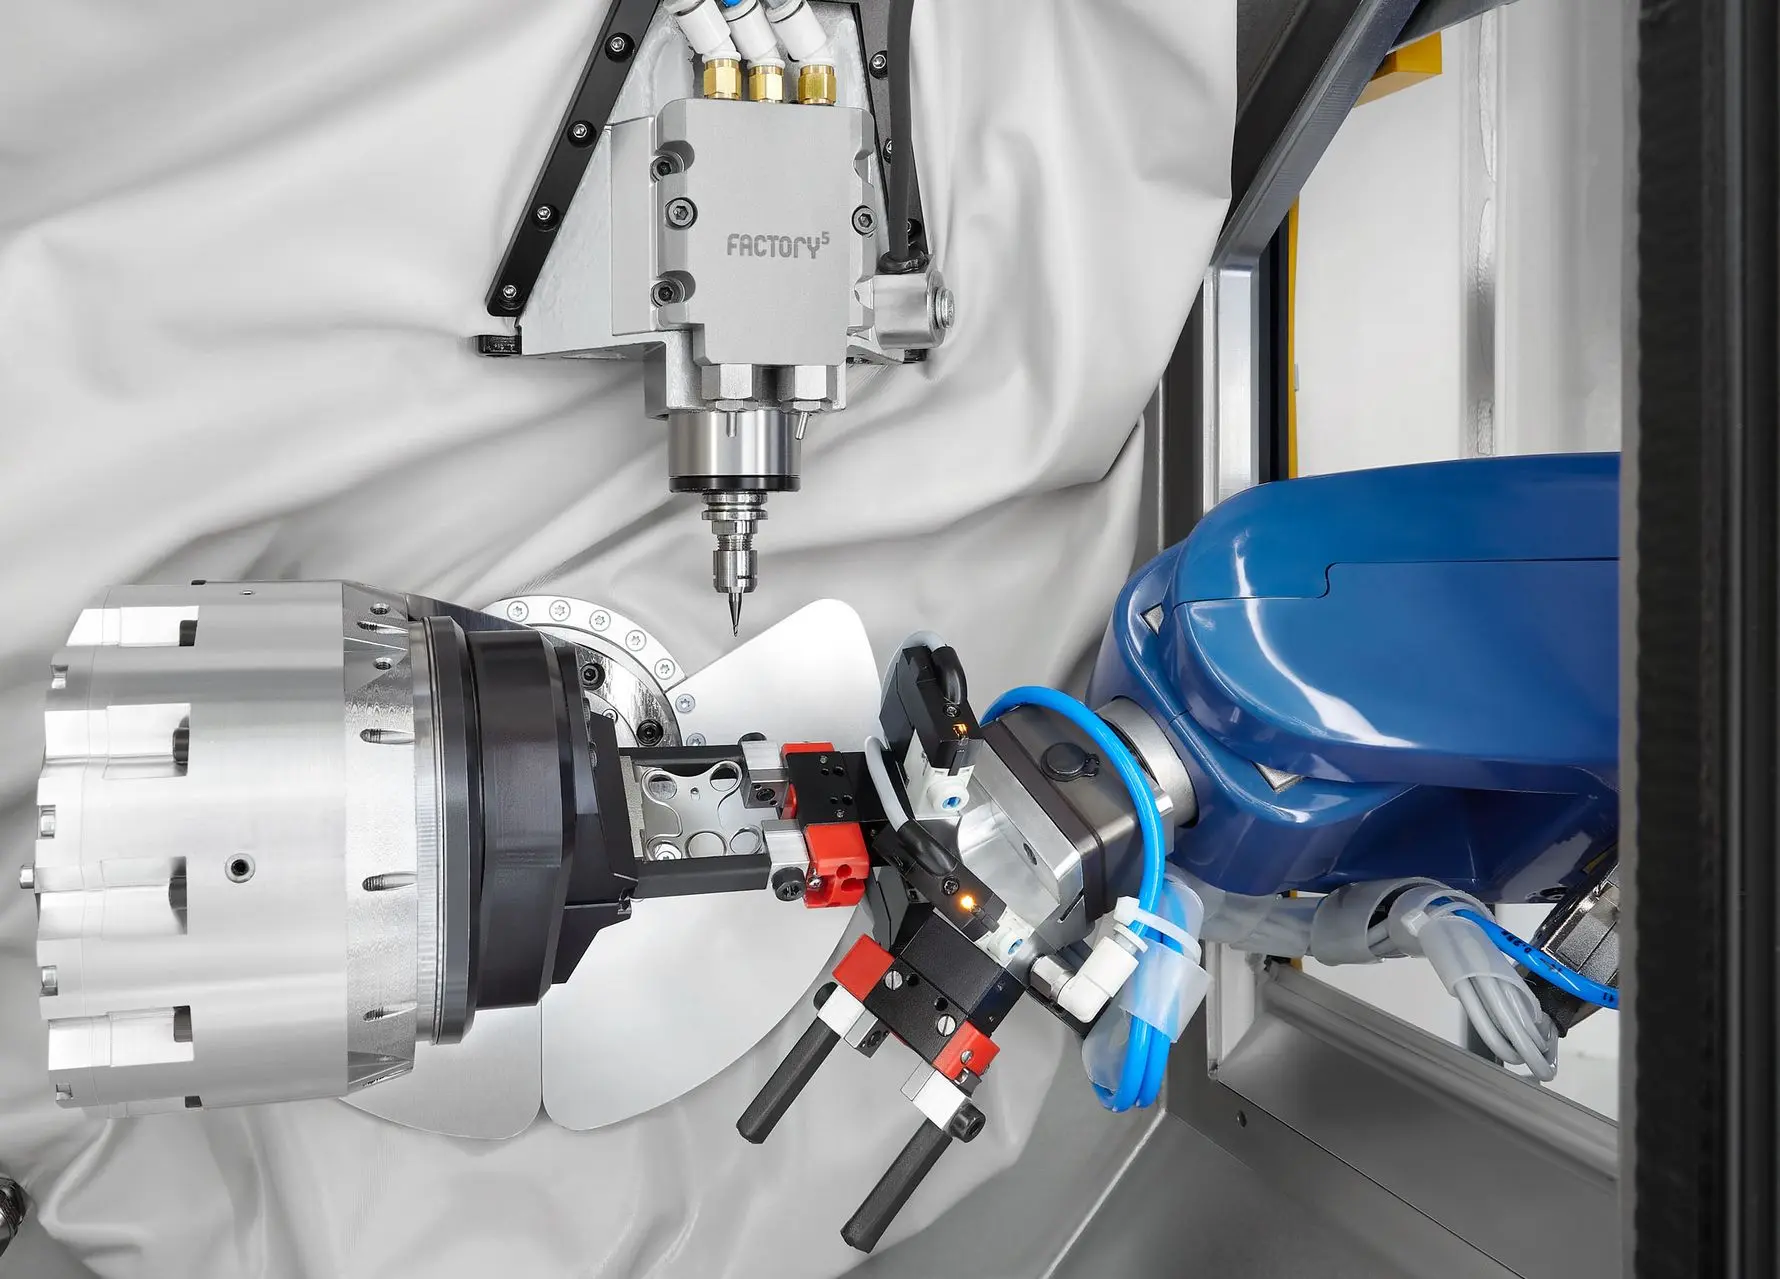
The current Micro5 page describes Variocell UNO handling and up to six pallets in the machining area. Name the complete system in the offer: loader, pallets, grippers, fixture, identification, safety interface and control integration. A handling picture does not establish that all of these are included in a base machine.
Present a reliable datum
Identify the gripping surface, insertion clearance and repeatable fixture location. Check a tilted workpiece against fingers, jaws, nozzle and tool access; include the reject or rework route.
Remove chips without losing the part
Trial cleaning and seating with the actual material and small features. For precious metals, agree the collection/recovery method and verify it on the intended process. Ask what confirms presence, seating and a successful clamp.
Recover safely
Demonstrate an interrupted load, tool change and machine cycle, along with restart and traceability. Include tool-life management, sister tools and operator intervention in the unattended-time estimate.
Inspect the tiny feature, then inspect the released part
Provide material, blank condition, drawing datums, burr limits, surface finish and the smallest feature. Agree CAM/postprocessor and five-axis simulation for the exact control and kinematics. A nominal travel or high spindle speed does not establish wall thickness, hole size or cosmetic finish.
Run representative conditions
Trial the actual fixture, holder projection, cutting tools, lubrication and thermal routine. Define tool-wear intervals and repeat the critical features over the agreed sample run; record complete elapsed time and changes.
Make measurement credible
Agree instrument access, reference method, environmental conditions and sample handling. Inspect after unclamping when fixture stress can affect geometry. Medical-part manufacture also needs the buyer's material, process and regulatory validation; the machine is not a device approval.
Taicang manufacturing and Swiss Micro5 expertise have different roles
CHIRON's China location page identifies 巨浪凯龙机床(太仓)有限公司 as the group's China subsidiary and describes the Taicang Future Factory as a development, manufacturing and sales centre. Its local range includes FZ 15 W, 22/25-series single- and twin-spindle routes, MILL five-axis systems and MC 528 TWIN. Large production parts require their own selected-model review; they are not scaled Micro5 applications.
The Swiss location page identifies CHIRON Swiss SA in Isérables as the birthplace of Micro5, with process, fixtures/tooling, CAD/CAM, automation, test-cut and service expertise. This does not assign every Micro5 or XL unit a manufacturing site. Confirm the contracting entity, actual build location, model revision and destination support in the quotation.
A 7 July 2025 Taicang government industry report names the exact China company and its local machine-tool activity. It corroborates the entity's industrial presence; it is not a Micro5 accuracy certificate. The China location describes spare parts, training, process optimisation, maintenance and refurbishment. Agree who supplies each service, language, remote-access requirements and response scope for the installation destination.
Send the smallest difficult feature, not only the overall size
Include material and blank CAD, fixture/gripping surfaces, tilted envelope, shortest tool projection, smallest hole or thin wall, burr/finish limits, occupied tool plan, spindle option, loader/pallet scope, complete output target, inspection method and destination. Request a representative trial and the actual build/service responsibilities.
CHIRON RFQ ↗