
浙江广旭数控设备有限公司
Hangzhou, Zhejiang
Guangxu routing & printed-contour cutting
Choose by the job: multiple cutters on plain stock, or following an outline on printed material. MD2500ATC and H2-2500CC share a sheet area, but their production tasks differ.
Company and both exact model pages reviewed 8 October 2026
The same sheet size, two different jobs
| Your production requirement | MD2500ATC | H2-2500CC |
|---|---|---|
| Main selection reason | Four-tool automatic-change routing | CCD registration for printed-contour cutting |
| Working area | 1300 × 2500 mm | 1300 × 2500 mm |
| Spindle power | 7.5 kW | 3.0 kW |
| Non-cutting travel | 40 m/min | 35 m/min |
| Quoted process to demonstrate | Tool selection, calibration and complete CAM job | Printed-sheet registration and cut alignment |
| Published machine mass | 1500 kg | 1000 kg |
Swipe sideways for both model columns on a narrow phone.
Give the supplier material type and thickness, the actual artwork or machining file, required edge finish and workholding plan. A 1300 × 2500 mm nominal area does not establish usable space once clamps, margins and registration requirements are added.
H2-2500CC: make the cut follow the print
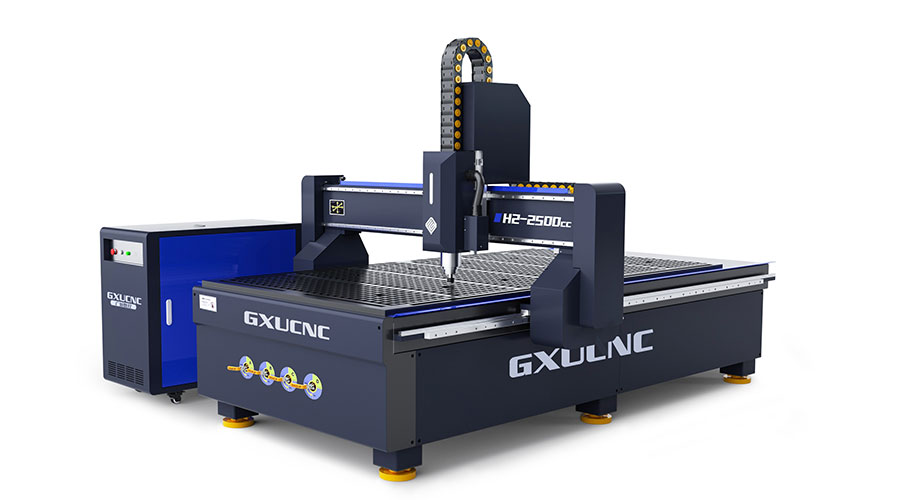
The official material presents a CCD camera and four-point positioning for irregular printed outlines. Its purpose is to align cutting with printed stock, rather than rely only on a nominal sheet origin.
Prepare one complete printed-job handoff
- Artwork: provide the original image/vector file and required final outline.
- Actual sheet: include material, thickness, print finish and the proposed registration marks.
- Cut result: agree the allowed cut-to-print offset, smallest features and edge quality.
Ask the demonstration to show file import, contour generation/editing, mark recognition and recovery if a mark cannot be read. Test the actual colors, reflectivity and print distortion instead of a different sample sheet.
The parameter table specifies servo drive, while a general component illustration mentions stepper/servo. Identify the delivered drive system and controller in the quotation. Its equipment and tool options should be named individually; this page does not assign MD2500ATC's four-tool magazine to H2.
Review H2-2500CC model specifications ↗MD2500ATC: plan the four-tool operation sequence
MD2500ATC lists a four-position inline magazine and automatic tool calibration. Its moving gantry uses rack transmission on X/Y and a ground ball screw on Z. The model's 7.5 kW spindle rating should be paired with the actual cutter, material and duty requirements.
The company names G-code and PLT files produced by several CAD/CAM applications. Agree the actual postprocessor, controller dialect, tool-change commands and offsets, then dry-run a representative program before cutting.
Send an operation list with the tools
For each pocket, engraving pass, hole or perimeter cut, name the cutter/holder, projection, depth, machining order and desired finish. Confirm magazine clearance, calibration method and safe approach/retract positions.
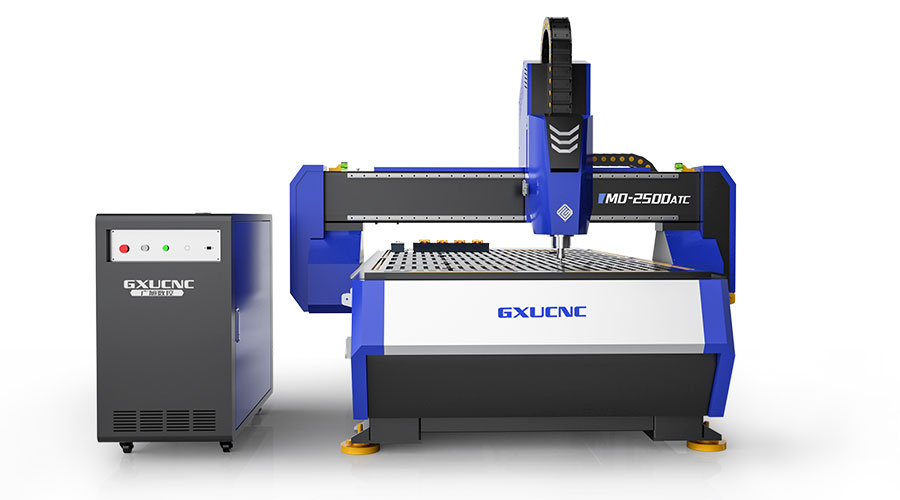
The model material lists wood, acrylic, aluminum, copper, composite aluminum panels, plastics and carbon-fiber composites as intended applications. Those categories do not specify a permitted thickness, feed, cut quality or extraction package. Request a trial and suitable chip/dust handling for the exact material.
Review MD2500ATC model specifications ↗Use one production sheet to agree acceptance
Hold it as you will in production
Specify vacuum zones, spoilboard or clamps and the smallest parts remaining after cutting. Demonstrate how the last cut is supported and how finished pieces are removed without shifting the rest of the job.
Measure the relevant result
For printed work, measure cut-to-print alignment across the sheet and around difficult contours. For routing, measure representative dimensions and inspect edge finish with the agreed tools/material. Record the method, sample quantity and required tolerances.
Count the complete cycle
Include loading, registration or calibration, tool changes, cutting and unloading. Keep operator work and non-cutting movements visible in the result; neither published travel speed nor a repeat-positioning figure establishes complete production output.
The catalog gives processing/repeat-positioning figures of ±0.05 / ±0.02 mm for MD2500ATC and ±0.2 / ±0.1 mm for H2-2500CC. These manufacturer figures do not include a complete test method or your stock/print conditions. Use agreed dimensional or cut-to-print limits for the actual sample.
Both tables name AC 380 V / 50 Hz. Include your destination supply and extraction/workholding requirements in the installation offer. H2 dimensions are listed as 3175 × 2038 × 1856 mm; add material-loading, cabinet and service access, and obtain the full MD2500ATC layout separately.
Guangxu's sheet-processing equipment business
Zhejiang Guangxu CNC Equipment develops and manufactures equipment for laser processing, sign production and furniture manufacturing in Hangzhou. Its official catalog includes CNC routers, laser-cutting machines, laser-welding equipment and customized models.
A Zhejiang trade-promotion article published 30 June 2025, sourced to Hangzhou's trade-promotion council, names the exact company among exhibitors at a June industrial exhibition in Indonesia and describes its routing/laser equipment business. That dated exhibitor account is separate from a machine inspection or certification.
This study compares two routing/cutting models. Laser processes require their own material, source-power, enclosure and application review; their capabilities are not inferred from either spindle machine. The purchasing and trial guidance above is CNCVerified's analysis of the reviewed manufacturer material.
Send the sheet, file and desired result
Attach artwork/CAM files and representative printed or plain material. State thickness, sheet size, workholding, tool sequence, finish/alignment tolerances, batch mix and destination utilities. Ask for the configured machine and a demonstrated full job.
Request a Guangxu quote ↗