
嘉泰数控科技股份公司 · Quanzhou, Fujian
J-TECH: hold the thin housing, then measure the complete cycle.
Compare JT-TL510A and JT-TL1000 by fixture span, nose clearance and usable tools. Specify machine acceptance separately from loading, inspection and sorting.
Compare the loaded part ↓Prepare a J-TECH RFQ ↗
Individual model tables, company material, the 2025 issuer report and a 2026 regulator record reviewed 8 October 2026
A longer table does not remove the thin-wall problem
J-TECH presents these BT30 drilling/tapping centres for small housings, frames, heat sinks and similar parts. Start with wall thickness, support points and the hole/pocket sequence. A phone-style shell or light frame can fit the machine yet move under clamping or cutting. For TL1000, review the longer loaded fixture and remote features; for TL510A, review the compact nest, tool reach and space used by multiple parts.
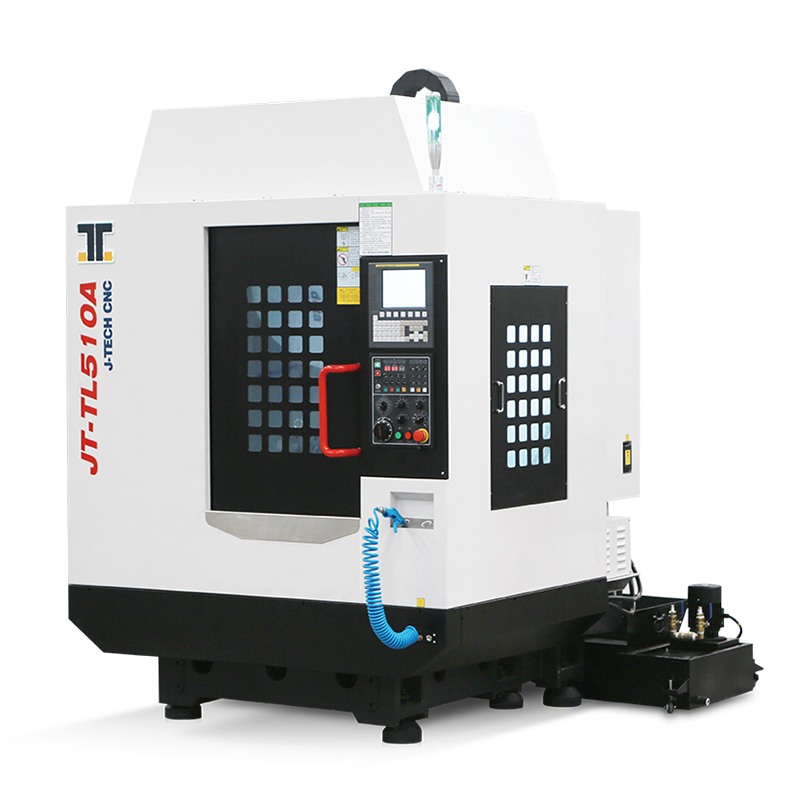
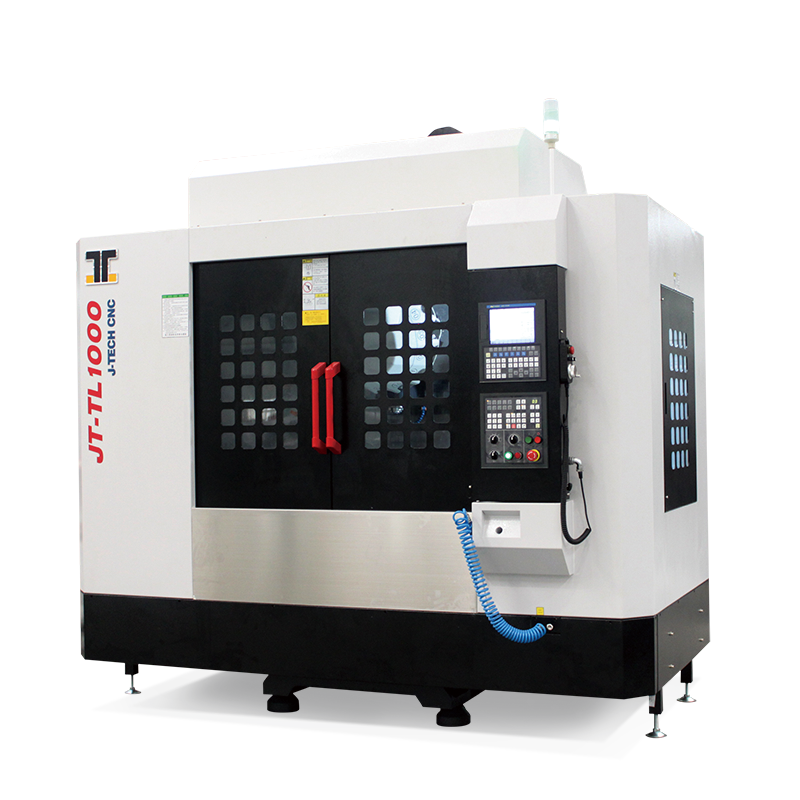
Swipe the model-table comparison on a phone. The conflicting headline figures are addressed below.
| Loaded setup reference | JT-TL510A | JT-TL1000 |
|---|---|---|
| X / Y / Z travel | 510 / 400 / 350 mm | 1000 / 500 / 350 mm |
| Table / load reference | 650 × 400 mm / 250 kg | 1100 × 500 mm / 350 kg |
| Nose-to-table window | 150–500 mm | 100–450 mm |
| Spindle-centre to column | 450 mm | 550 mm |
| Model-table spindle | 20,000 rpm direct / BT30 | 21,000 rpm direct / BT30 |
| Model-table rapids | 60 m/min X/Y/Z | 48 m/min X/Y/Z |
| Magazine / tool length | 21 positions / 200 mm | 16 radial positions / 200 mm |
Both have 350 mm Z travel, but the nose windows differ. TL1000's longer X stroke does not add vertical clearance. Draw the shortest tool at the lowest surface, the longest holder above the tallest clamp and the withdrawal route. Include fixture mass, loading hardware and offset in the load review. Obtain permissible distribution and the interference drawing before committing to a multi-nest arrangement.
Use one dated build sheet when the page disagrees with itself
- TL510A · 16 or 21 tools?
- The structure section labels a 16-tool magazine, while the exact table gives 21 positions. Its headline says 1.9 s tool-to-tool, while the table says 2 s. Request the delivered magazine and change-time definition. The table's Ø60/80 mm pair does not explain the occupancy condition; do not assume both permit every neighbouring tool. Ask for the complete occupied-tool layout and holder-mass limit.
- TL1000 · headline or model table?
- The headline says 20,000 rpm and 60 m/min. The exact table gives 21,000 rpm, 48/48/48 m/min, a 16-position radial magazine, Ø80 mm tool diameter, 200 mm length and 3 kg mass. This profile uses the table as a reference and keeps the disagreement visible. The 2.2 kW motor entry lacks a duty curve; check torque at the actual tap and cutter speeds.
- Controls and included equipment
- TL510A's table names FANUC 0i-MF; TL1000 lists FANUC 0i-MF or Mitsubishi M80. The accessory panel mixes family references, optional 16/21 magazines, fourth-axis arrangements, automatic doors, safety locks and measuring equipment. Agree the exact model/control, included safeguards and options; a family accessory list is not the delivered bill of materials.
Buying the machine and buying a sorted production cell are different jobs
The manufacturer describes linking drilling centres with robots, fixtures and transfer equipment for metal-housing production, adding online inspection and good/reject sorting. That is an integration scope, not a feature proved by either bare machine's table.
Machine boundary
Define fixture, tool list, coolant and chips, control program, door/interlock behaviour and finished-part acceptance. The published rapid and tool-to-tool values cover only pieces of the sequence. They do not establish a thin-wall part's stability, thread quality or total cycle.
Cell boundary
Define blank presentation, grip/support, part orientation, clean datum seating, inspection method, reject handling and traceability. Agree control/robot interfaces, enclosure and restart after an interrupted cycle. A pneumatic door or cloud connection alone does not establish safe autonomous operation or correct sorting.
Specify who supplies each component, owns the interface work and accepts the combined cell. Request separate machine and full-cell test records. Review tools, chips, air and lubrication alarms during extended operation rather than demonstrating only one robot load.
Let the housing reveal the clamp and inspection errors
Trial the real support and clamp sequence
Use the production material and wall thickness, including any later surface treatment or machining allowance. Record locating and clamping points, loading orientation, cutter projection and cutting order. Inspect flatness and wall/slot relationships after release where deformation matters.
Test the difficult hole and the distant feature
Include the smallest thread, deepest blind hole and burr-sensitive edge. On a long TL1000 fixture, inspect the feature furthest from the main datum as well as the nearby one. Agree gauges, measurement uncertainty, thermal conditions and sample size; static positioning figures are not a finished-part guarantee.
Count accepted parts through a complete run
Measure loading, datum cleaning, machining, tool changes, inspection and sorting together. Challenge an incorrectly seated blank and a rejected part using an agreed safe procedure. Record tool wear, recovery and scrap criteria. Quote the full accepted-part cycle and yield conditions, not just rapid travel or the fastest single part.
Check the contracting entity and the ongoing delivery obligation
The 2025 issuer report identifies 嘉泰数控科技股份公司, J-TECH CNC TECHNOLOGY CO., LTD., in Quanzhou, and records incorporation on 12 July 2011. The company page's 1997 factory-history statement is a predecessor history, not that entity's incorporation date. The report describes machine equipment, automation, online inspection and precision processing; it does not certify the two models or establish every advertised industry application as a completed customer project.
The 2025 issuer report, pages 43–44 contains a qualified financial audit opinion and a material going-concern uncertainty paragraph. A 8 April 2026 Fujian regulator decision concerns guarantees and disclosure. These are business/governance records, not a machine test or a finding that these models are defective. For a purchase or integrated line, obtain current contracting and production responsibilities, staged delivery/acceptance terms and a documented service/spares arrangement.
J-TECH's presales navigation provides process-solution, trial-machining, selection and training routes. Agree the actual trial, installation, training and destination support in the contract. Obtain utilities, lifting, foundation and maintenance access for the selected machine/cell. Domestic network statements do not prove overseas response time or the scope of a specific warranty.
Send a supported housing and an accepted-part target
Include part/fixture CAD, material and wall thickness, clamp/support plan, total load and offset, critical holes/threads and distant datums, tool list/projections, chosen model/control/magazine, coolant/chip needs, loading/inspection/sorting scope, released-part inspection method, full-cycle and run-length targets, delivery destination and staged acceptance requirements. Request one dated build sheet and a trial covering the complete route.
J-TECH RFQ ↗