

无锡开源机床集团有限公司 · Wuxi, Jiangsu
K-YUAN centreless grinding: choose the support and feed route for the part.
A straight cylinder that can pass through the wheels needs a different setup from a shouldered or profiled part. Compare the group's M1050A and MK10100 catalogue references, then define the blade, wheels, feed and acceptance trial.
Choose through-feed or infeed ↓ Prepare a K-YUAN RFQ ↗
Company history, original centreless catalogue and both model tables reviewed 8 October 2026
Can the part pass through, or must it stop at the grinding position?
Straight cylindrical OD · through-feed
Draw the full blank, not only its finished diameter. Identify steps, heads, grooves, interrupted surfaces and anything that could strike the guides or wheels. Define how parts enter, remain supported and leave the grinding zone. Both references list through-feed capacity, with different diameter, length and wheel widths.
A through-feed arrangement does not automatically maintain every feature's concentricity to an existing bore or centre datum. Specify the required relationship and the inspection method before choosing the locating/support strategy.
Shoulder, taper or stopped feature · infeed
Send axial positions, shoulder clearances and the wheel form. M1050A's catalogue describes an added infeed mechanism for conical parts up to 1:20 taper; its table separates through-feed Ø5–50 mm from infeed Ø7–50 mm. Do not treat that attachment as included in every standard machine.
MK10100 lists infeed Ø5–100 mm and 280 mm maximum grinding length as special order, while the standard-support through-feed reference is Ø5–100 mm and 250 mm. Agree the stopped-part support, loading and dressing package explicitly.
Two different feed and wheel packages
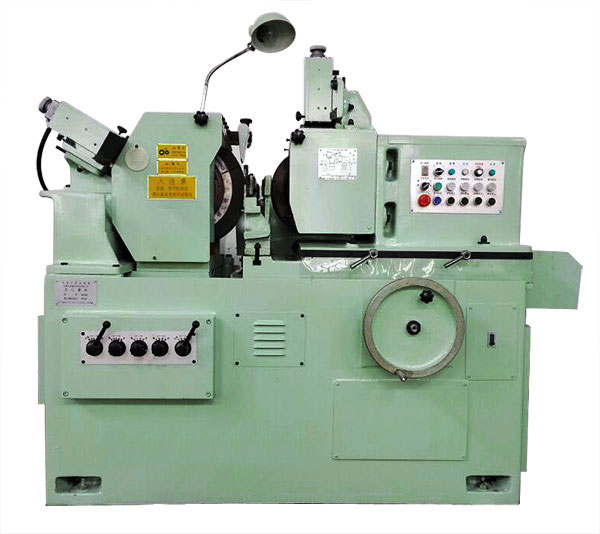
M1050A · manual main feed ↗
The regulating-wheel stand uses manual main feed and a hydraulic slide swing for infeed. The grinding spindle is described with a five-pad hydrodynamic bearing; the regulating spindle uses a sliding-bearing arrangement. Grinding/regulating dressing feeds are manual, with hydraulic-cylinder reciprocation.
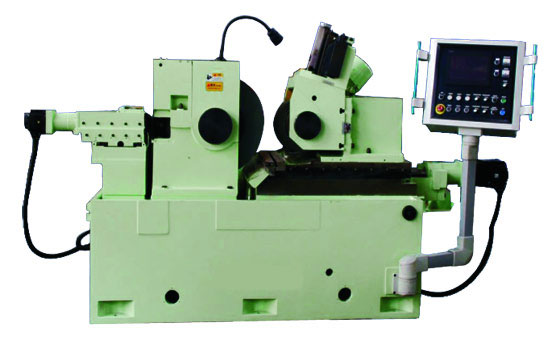
MK10100 · servo main feed ↗
The catalogue calls it a four-axis CNC centreless grinder. The model description names a single-sided moving regulating-wheel stand, double-V rolling-steel guides and servo feed, with dual-supported rolling bearings for both spindles. Dresser reciprocation has geared-motor or servo alternatives; confirm the delivered arrangement.
Swipe the comparison on a small screen. The check label stays visible.
| Check | M1050A | MK10100 |
|---|---|---|
| Through-feed diameter | Ø5–50 mm | Ø5–100 mm standard support |
| Infeed diameter | Ø7–50 mm attachment/configuration to confirm | Ø5–100 mm special order |
| Grinding length reference | Maximum 120 mm | Through-feed 250 mm standard; infeed 280 mm special order |
| Grinding wheel | P400 × 150 × 203 | 1~610 × 300 × 305 mm published designation |
| Regulating wheel | PSA300 × 150 × 127 | 1~320 × 300 × 203 mm published designation |
| Grinding spindle | 1668 rpm; 11 kW motor | 1380 rpm; 22 kW motor |
| Regulating spindle | 20–200 rpm; 1.5 kW motor | 10–200 rpm working / 300 rpm dressing; 3 kW motor |
| Machine reference | 1920 × 1681 × 1479 mm; 2800 kg | 2420 × 1540 × 1700 mm; approximately 5900 kg |
The blade and wheel relationship define the grinding setup
The published distance from the grinding/regulating-wheel centre line to the support base is 220 mm for M1050A and 200 mm for MK10100. These describe the machine arrangement; they are not a ready-made workpiece centre-height or blade-setting recipe. Specify the part diameter, support blade geometry/material, contact position, regulating-wheel setting, axial guides and clearances with the process proposal.
Wheel width is a process choice
MK10100's wider 300 mm wheel does not by itself prove a higher removal rate or a finished-part output target. Choose abrasive, bond, form, grade, coolant and allowance for the actual material/heat treatment. Confirm wheel balance, spindle condition, loading and dressing interval before agreeing production performance.
Keep dressing and working speeds separate
MK10100 lists 300 rpm regulating-wheel dressing speed separately from 10–200 rpm working speed. Request the dresser actuation, compensation and profile strategy on the delivered machine. M1050A's manual dressing feeds and hydraulic reciprocation need a different setup and operator sequence; a controller photograph is not proof of automated compensation.
For ring-shaped parts, show wall thickness, bore, stiffness and any requirement linking the finished OD to another datum. Establish support and deformation control using the real blank. For feeding automation, define entry/exit guides, part separation, jam detection and measurement; no automatic feeder is established by either base table.
Accept the grinding process with representative blanks
Fix the support and abrasive recipe
Record material, heat treatment, blank OD/allowance, part length, blade, wheel specifications, dress form, coolant and feeding arrangement. For infeed, include the actual shoulder/taper clearance and special-order attachment; for through-feed, use the intended entry and exit supports.
Run beyond the first acceptable part
Agree warm-up and a repeat run that includes dressing, loading, wear and inspection. Record grinding parameters and compensation after dressing. Include throughput variation, loading/handling and rejects when assessing accepted parts per cycle or batch.
Check roundness, size and released condition
Agree measurement positions and methods for roundness, diameter consistency and surface roughness, plus cylindricity/datum relationships where the drawing requires them. Inspect released parts under agreed temperature conditions and check grinding integrity appropriately for the material.
The source publishes working-accuracy values for each reference, but does not give the complete blank, support, wheel and test conditions beside them. Those values are not unconditional guarantees for every material or setup. Make the part, process settings, test duration and inspection method part of the acceptance schedule.
A grinding solution, with a clearly named supplier
Wuxi K-YUAN Machine Tools Group Co., Ltd. presents grinder sales, machine-tool casting, sheet-metal work and spindle repair/technology activities. Its company history distinguishes the original 1948 machine works from the group formed in 1997, and records disposal of the machine-tool share company in 2015. Historic factory and joint-venture names should not be assumed to be the current contracting or manufacturing entity for these catalogue machines.
The company describes a grinding laboratory established in 2016, with spindle-related technology, centreless/double-face grinding trials and instruments for stiffness, vibration, thermal deformation and motion accuracy. Request a current, part-specific process demonstration and the responsible team rather than treating this dated description as evidence of every available test or current OEM partnership.
A 2 June 2026 Wuxi industry authority notice names 无锡开源机床集团有限公司 in an association officer nomination record. It supports the company identity in a dated public record; it is not model certification or a grinding-performance test.
Name the supplier, actual machine manufacturer, new/refurbished status, model and serial/build revision, configuration, warranty and destination service. Include foundation/handling drawings, fluid and electrical requirements, blade/wheel/dresser supply, setup training, controller/parameter backups and acceptance. Reference total motor power is approximately 13.78 kW for M1050A and 27 kW for MK10100; distinguish it from the grinding-spindle motor alone.
Send the part, feed route and datum requirements
Attach material/heat treatment, blank and finished OD, length, shoulders/taper, bore/wall thickness, drawing datums, roundness/size/finish criteria and inspection method. Specify through-feed or stopped infeed, wheel/support concept, allowance, output target, handling and destination. Ask for the named supplying/manufacturing entities and the delivered configuration.
Send K-YUAN RFQ ↗