
Ningxia Little Giant Machine Tool Co., Ltd. · 宁夏小巨人机床有限公司 · Yinchuan
Choose the loaded fixture. Then choose the spindle duty.
Mazak’s Ningxia operation combines manufacturing with an engineering centre for trials and training. Compare the current China VCN-460 L and VCN-600 L references by reach, distributed load and continuous power.
Compare the current China builds ↓Prepare a Little Giant RFQ ↗
China model-detail sheets, Ningxia factory material and a dated safety-standardisation notice reviewed 8 October 2026
The bigger table has the same vertical reach
The exact China detail sheets identify VCN-460 L and VCN-600 L. Use the L designation when comparing a quotation with these specifications. Both references use a BT40 12,000 rpm spindle, 510 mm Z travel and a 150–660 mm table-to-spindle-end window. The larger table does not provide a higher fixture or longer vertical stroke.
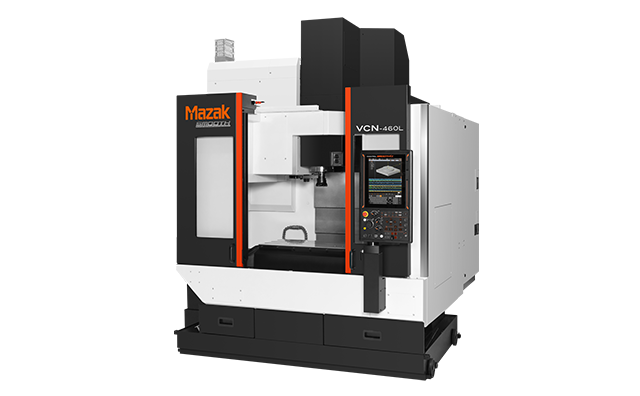
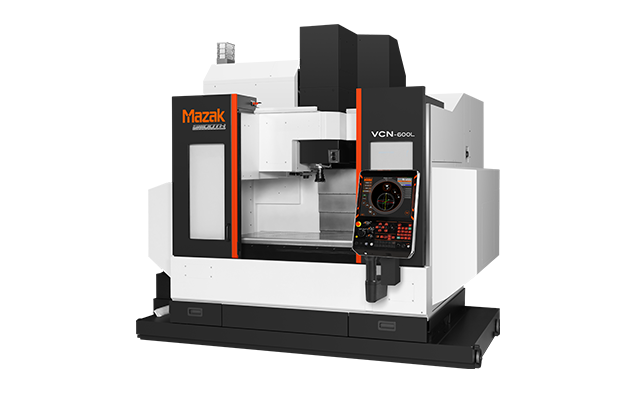
Swipe the table on a phone. Loads are specified for uniform distribution; pallet limits are addressed separately below.
| Exact China detail reference | VCN-460 L | VCN-600 L |
|---|---|---|
| X / Y / Z travel | 560 / 460 / 510 mm | 1050 / 600 / 510 mm |
| Table dimensions | 900 × 460 mm | 1300 × 600 mm |
| Uniformly distributed load | 500 kg | 1200 kg |
| Spindle-end window | 150–660 mm | 150–660 mm |
| Maximum rapid X/Y/Z | 42 / 42 / 42 m/min | 42 / 42 / 42 m/min |
| Magazine | 30 positions | 30 positions |
| Listed machine mass | 4800 kg | 6800 kg |
Draw the mounted workpiece, locating/clamping points and required cutting path. A 900 mm table is not 900 mm X travel: VCN-460 L gives 560 mm. Check access to the far feature as well as the part fitting on the table. For VCN-600 L, include the long fixture’s overhang and load distribution; 1200 kg uniformly distributed is not permission for every concentrated or offset load.
18.5 kW is not the continuous rating
The duty entries belong together
Both detail sheets list 18.5 kW at 10% ED and 11 kW continuous. Torque is 119 Nm at 10% ED or 95.5 Nm at 25% ED. Request the torque/speed curve and permitted duty for the proposed cut. Do not combine peak torque, maximum rpm and continuous running into one unsupported performance claim.
The family page’s removal-rate comparisons are manufacturer examples with stated tools/material, not a guaranteed result on the buyer’s part. Test the actual cutter engagement, chip removal and sustained roughing interval.
A pallet route and a fine-finishing route need separate decisions
- VCN-600 optional pallet exchange
- The family page lists an optional two-pallet arrangement with 1300 × 550 mm pallets, 800 kg maximum load, five 18 mm T-slots at 100 mm spacing and 17 s exchange reference. That pallet is narrower than the ordinary 1300 × 600 mm table and has a different load limit. Agree delivered compatibility and load definition. Include locating/cleaning, loading and inspection in the cycle; an exchange time alone does not establish accepted parts per hour.
- High-speed and small-tool finishing
- The family describes 60,000/80,000 rpm super-spindle options for VCN-460/600 and an 18,000 rpm spindle option specifically for VCN-600. These are separate packages from the 12,000 rpm detail reference. Obtain tool interfaces, allowable runout, coolant, control and automatic-change scope for the selected option. A published small STAVAX mould example does not establish the same finish on another material or geometry.
- Automation and factory access
- The Ningxia engineering-centre description includes trial machining, training and example automation cells. Define the actual robot/pallet system, guarding, tool-life monitoring, part identification and restart responsibilities. The detail-sheet body widths/lengths with SmoothEz are 2000 × 2729 mm and 2880 × 3094 mm respectively; heights are 2812 and 2817 mm. Obtain the complete installed layout, utilities and service space for the quoted cell.
Use the engineering centre to answer one difficult part question
Bring the actual fixture and demanding operation
For a compact job, test the lowest surface with the shortest tool and the deepest hole with its complete assembly. For the longer fixture, test the most distant datum and the heaviest sustained cut. Include blank condition, material and chip evacuation. Agree tool wear and thermal conditions rather than showing only a short demonstration cut.
Measure the released part against the drawing
Choose the key datum relationship, tolerance and surface requirement, then agree gauges, uncertainty and sample size. Include clamping deformation and re-loading where relevant. Machine positioning, a manufacturer removal-rate example or one polished test block does not replace the production-part inspection report.
Trial the selected option through a complete run
For pallet work, test seating after repeated exchanges and include cleaning/loading. For small-tool finishing, test the actual tool runout and surface measurement method. Record machining, changes, inspection and recovery together. Assign machine and combined-cell acceptance separately, with the delivered control and programs.
Ningxia’s manufacturing base is distinct from the global catalogue
Mazak identifies Ningxia Little Giant in Yinchuan as its first high-precision CNC production base in China, with an engineering centre for customer training and trial machining. The manufacturer’s MTF2025 event in Ningxia listed VCN-460 L and VCN-600 L among displayed machines. A display at that site does not by itself prove the manufacturing origin of every displayed model or offered serial unit.
A 17 January 2025 Ningxia Emergency Management notice names the exact company in its level-two safety-production standardisation list, with a stated three-year term. Its scope concerns enterprise safety production, not machining accuracy, model certification or an independent audit by CNCVerified.
Earlier regional references include VCN-430A, VCN-430B and VCN-530C. Current China family material instead lists VCN-535C and VCN-700D in its BT50 group. Do not transfer their parameters or photos into the earlier BT40 records. For an older model or installed machine, identify exact designation, serial year, control and regional documentation before comparing it with the current L build.
Specify the contracting entity, manufacturing site, configuration and acceptance location for the actual unit. Agree training, postprocessor/control support, spare-parts scope and destination response terms. The group’s service network and factory concept do not establish a particular warranty or a guaranteed delivery date.
Send the fixture, duty cycle and selected options
Include part/fixture CAD, total load and distribution, critical distant/low features, complete tools and occupied slots, material and sustained-cut duty, intended China L or earlier regional model, spindle/control, pallet or small-tool finishing options, inspection method and sample run, installation destination and utilities, manufacturing origin and acceptance responsibilities.
Little Giant RFQ ↗