
MLTOR · 迈雷特
Zhongshan, Guangdong
MLTOR: choose the cutting route for your gear geometry
Internal cylindrical gears and spiral bevel gears need different tools, locating arrangements and inspection plans. Start with the tooth drawing before comparing these two machines.
Official company material and original model brochures reviewed 8 October 2026
Which tooth geometry are you making?
Straight or helical internal teeth
The YK8035 route is gear skiving. Check the internal tooth geometry, cutter entry and exit, adjacent shoulders and clamping clearance together. An accessible bore is essential information for a tooling proposal.
Review YK8035 tooling and envelope ↓Teeth on a conical gear blank
The YK2232 route is spiral bevel gear milling. Specify the bevel geometry, cutter system, locating surfaces and, where applicable, the mating gear and assembly requirements.
Review YK2232 cutting package ↓350 mm and 320 mm describe different dimensions
YK8035 publishes a maximum machining inner diameter of 350 mm. YK2232 publishes a maximum pitch diameter of 320 mm. Neither number should be substituted for the other, or treated as a complete blank-and-fixture envelope. Send a dimensioned section through the gear and its locating surfaces.
YK8035: clear the cutter inside the gear
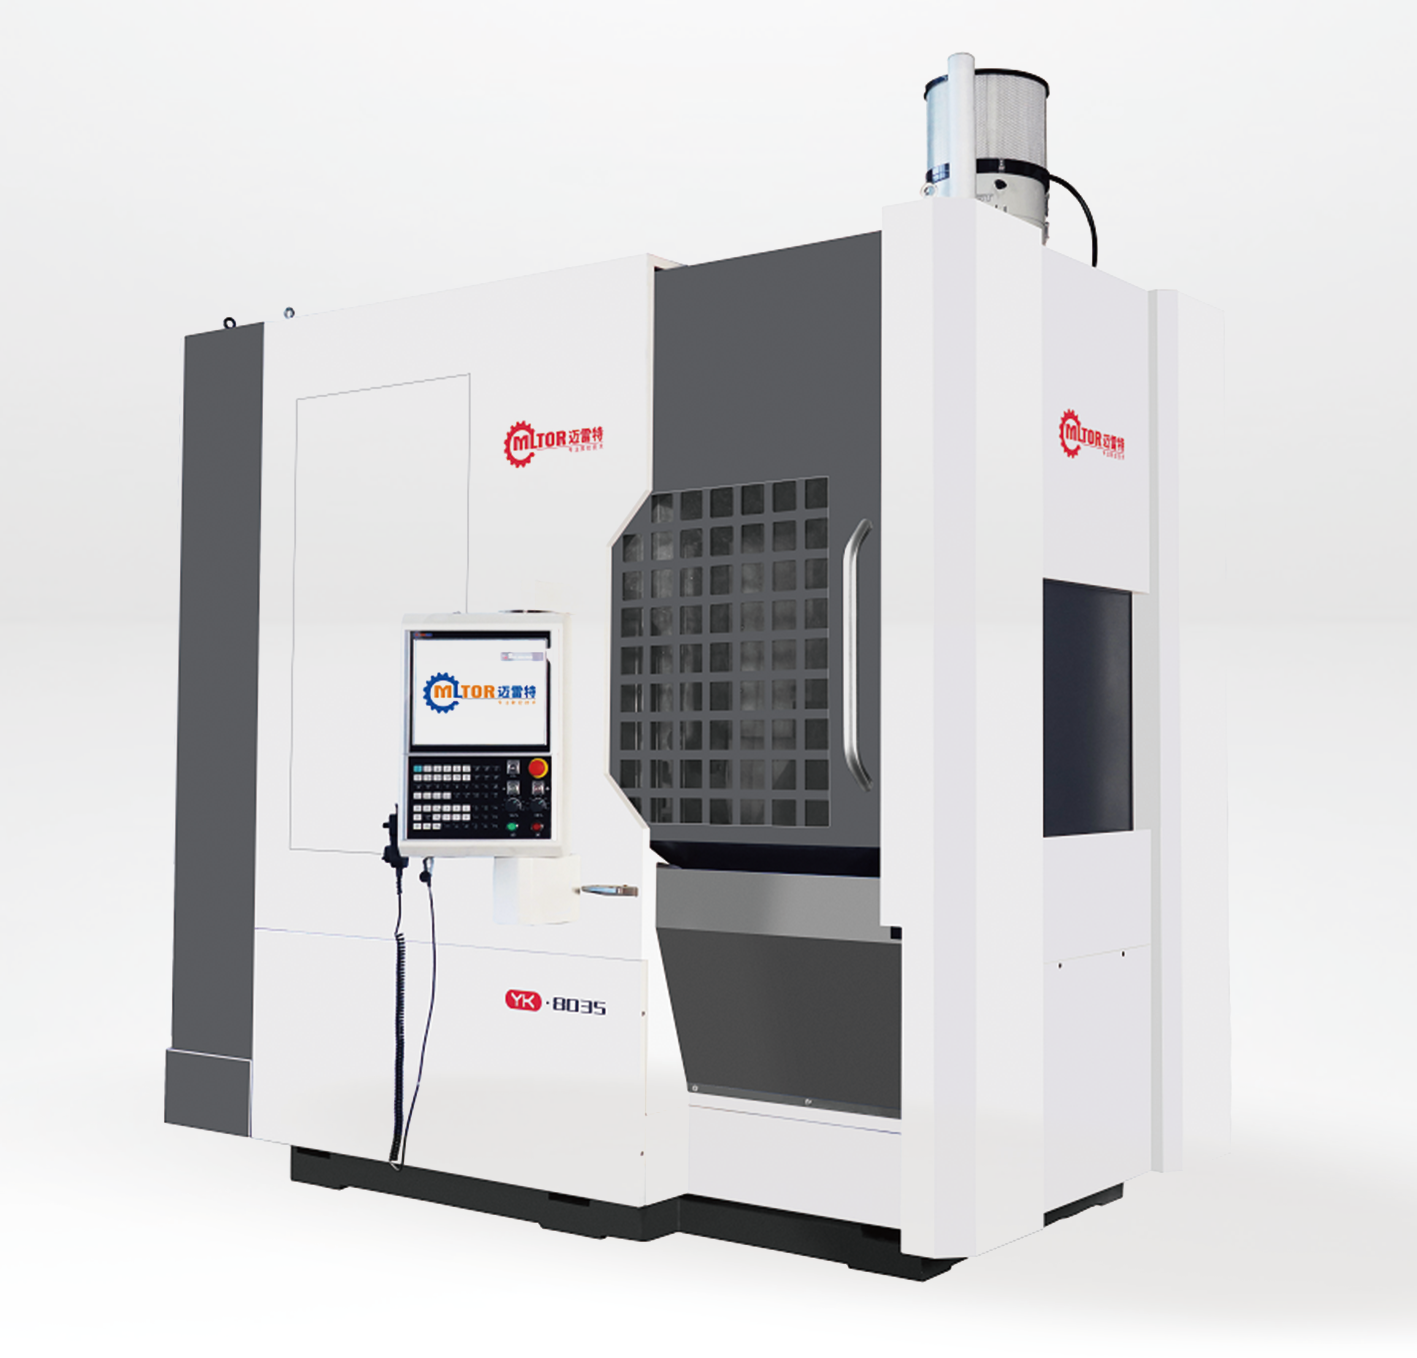
Internal skiving envelope
- Maximum machining inner diameter / module
- 350 mm / 4
- Maximum skiving length / minimum teeth
- 100 mm / 17
- Tool spindle / worktable speed
- 1500 rpm / 1000 rpm
- Worktable diameter
- 370 mm
- Tool shift / tool-head swivel
- ±55 mm / ±30°
- Z range / tool interface
- 75–355 mm / HSK100
- Main motor / total power entry
- 27 kW / 55 kW
- Machine dimensions / mass
- 4100 × 2800 × 2800 mm / 11000 kg
Approve the cutter and fixture as a pair
Supply internal tooth count, module, helix information, tooth length and the blank's bore, shoulders and clamping section. Request a cutter proposal and an interference check covering approach, full tooth depth and withdrawal. The published ±30° head swivel is a machine setting range, not a stated maximum workpiece helix angle.
MLTOR describes six controlled axes, direct-drive B/C axes, rotary-encoder feedback, cooling and its iSmart-Ai800A control. Demonstrate the offered control version, gear program and any remote/MES interface using your own job. A named interface does not establish compatibility with your production system.
YK2232: specify the bevel cutter system
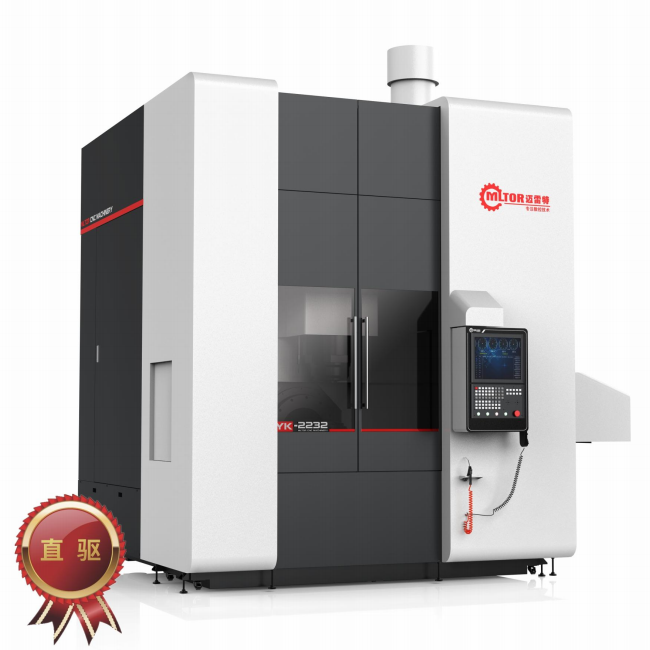
| Gear / cutting item | Published value | Proposal requirement |
|---|---|---|
| Pitch diameter / module | Up to 320 mm / 6 | Complete blank, pitch geometry and tooth drawing |
| Whole tooth depth / face width | 14 / 40 mm | Actual tooth system and machined width |
| Teeth / root-cone angle | 5–150 / 0–90° | Gear and mating-member geometry where relevant |
| Cutter-disc sizes | 3.5, 4, 6 and 7.5 inches | Selected cutter, blades, holder and supply scope |
| Tool spindle | 1000 rpm; HSK-100A | Tool assembly and cutting conditions |
| Work spindle | 300 rpm rated; 500 rpm maximum | Operating duty for the proposed job |
| Axis arrangement | Six controlled; five simultaneous | Program demonstration for the specified gear |
| Dimensions / mass | 3920 × 3201 × 3760 mm / 15200 kg | Installed layout, foundation and service clearances |
Swipe the cutting-package table on a narrow phone.
Agree the cutter system and the data needed to calculate settings before purchasing tooling. Include the locating bore, back face and any shaft/fixture projection in the clearance study. A supported cutter-disc diameter alone does not confirm every tooth system or blank can be processed.
MLTOR also describes loading, inspection, washing and storage modules. Order them as an explicit automation package with interfaces and acceptance criteria; they are not established as standard equipment on the pictured machine.
A gear drawing is more useful than a diameter-only inquiry
Tooth definition
Name cylindrical internal or spiral bevel geometry. Include tooth count, module convention, pressure angle, helix or cone information, face width, tooth depth and the drawing revision. Supply the tooth-system data requested by the proposed tooling process.
Blank and datum
Specify material, hardness/heat-treatment state, blank dimensions, locating faces, bore or shaft, clamping allowance and obstructions. Describe incoming variation and which features are already finished.
Production sequence
Show where gear cutting sits relative to heat treatment and later finishing. Give batch sizes, part mix, tool-life expectations, loading arrangements and inspection availability. Identify any manual operations within a requested cycle.
Agree how the finished gear will be accepted
The brochures contain manufacturer accuracy-grade claims. They are not CNCVerified test reports, and the inspection standard must match the gear form and drawing. Ask the supplier to identify the standard, revision, measured characteristics, measurement equipment and report for your trial part.
Internal-gear trial
Demonstrate the actual cutter/fixture setup, tooth entry and exit, completed tooth length and gear measurement against the drawing. Inspect the part after unclamping using the agreed datums. Record material state, tooling, cutting settings, inspection method and cycle boundaries.
Spiral-bevel trial
Approve the cutter settings and locating method, then inspect the machined member to its specified criteria. If the purchase includes a matched pair or assembly performance, agree the mating member, contact-pattern/backlash evaluation and test conditions separately. Cutting one member does not prove assembly acceptance.
For both routes, separate machining time from loading, setup, inspection and tool changes. Retain the program, tooling list and inspection report. Include control backups, training, utilities, foundation requirements and destination service obligations in the handover.
MLTOR's gear-manufacturing focus
MLTOR's official company material identifies 中山迈雷特数控技术有限公司 in Zhongshan, Guangdong. Its reviewed catalog covers gear-processing machines and related control/automation offerings. The two machines above address distinct gear forms; they do not represent interchangeable capacity or every product in the company's catalog.
A Zhongshan Science and Technology Bureau notice dated 21 August 2026 lists the company against a precision-gear flexible-manufacturing equipment pilot platform in a proposed recognition list. This is a dated proposed-list record, not evidence of final approval or machine-model certification.
The selection and acceptance guidance on this page is CNCVerified's editorial analysis of the reviewed manufacturer material. A quotation should identify the contracting entity, exact machine configuration, tooling and service responsibilities.
Send a gear-specific machining brief
Attach the gear drawing and blank section, tooth-system data, material and heat-treatment state, locating surfaces, batch mix and inspection criteria. Name the internal-skiving or spiral-bevel route and request a demonstrated cutter/fixture proposal.
Request an MLTOR quote ↗