
山东兄弟数控机床有限公司
Tengzhou, Shandong
Shandong Xiongdi CAK lathes: specify the spindle version and supported part.
CAK6150 and CAK6160 cover different bed-swing envelopes. The basic, B and C spindle builds and bed-length choices are separate decisions; a larger bore or longer bed should not be assumed from the family name.
Original CAK6150-1000, CAK6160 family and CAK6160-1000 references reviewed 8 October 2026
Keep the basic spindle, B and C columns separate
The published CAK6150 table combines the base, B and C references; the CAK6160 family table does the same. Choose the exact ordered suffix and length before comparing bar passage, chuck/interface, speed range and support. These are CNC turning references for outside/inside diameters, faces, grooves, tapers and threads; the reviewed materials do not establish a live-tool or simultaneous milling package.
Swipe on a small screen to compare the two family columns.
| Published check | CAK6150 reference | CAK6160 reference |
|---|---|---|
| Bed swing | 500 mm | 610 mm |
| Base spindle bore | 52 mm | 52 mm |
| B spindle bore | 80 mm | 80 mm |
| C spindle bore | 104 mm | 105 mm |
| Internal spindle taper | Base MT6; B Ø90 at 1:20; C Ø113 at 1:20 | Base MT6; B Ø90 at 1:20; C Ø113 at 1:20 |
| Published spindle motor | 7.5 kW | 7.5 kW |
| Tailstock sleeve | 150 mm travel; MT5 | 150 mm travel; MT5 |
| Rapid X / Z | 4 / 6 m/min | 4 / 6 m/min |
The CAK6150-C bore is published as 104 mm and CAK6160-C as 105 mm. Do not silently make them equal or apply either to the basic 52 mm spindle. A bore figure alone is not a supported bar-feed capacity: confirm chuck drawtube, jaws, liner, bar support and the permissible rotating arrangement on the selected build.
Bed swing, tool passage and supported length answer different questions
Disc, ring or short shaft
CAK6150 lists 500 mm bed swing but only 280 mm swing over the cross slide. Show the clamped blank, jaws, toolholder and approach path; a part that clears the bed may still strike the cross slide or tool assembly. CAK6160's reviewed table lists 610 mm bed swing without a corresponding cross-slide figure. Obtain that working clearance rather than borrowing it from CAK6150.
Longer supported shaft
CAK6150-1000 lists 1000 mm processing length; the CAK6160 family offers 750/1000/1500/2000/3000 mm length references. Usable cut length depends on chuck projection, tailstock/centre, tools and any steady/follower rest. Define grip length, protrusion, slenderness, centre holes and support; the 150 mm sleeve stroke is not the tailstock body's travel or the full machining length.
Original 1000-length model views
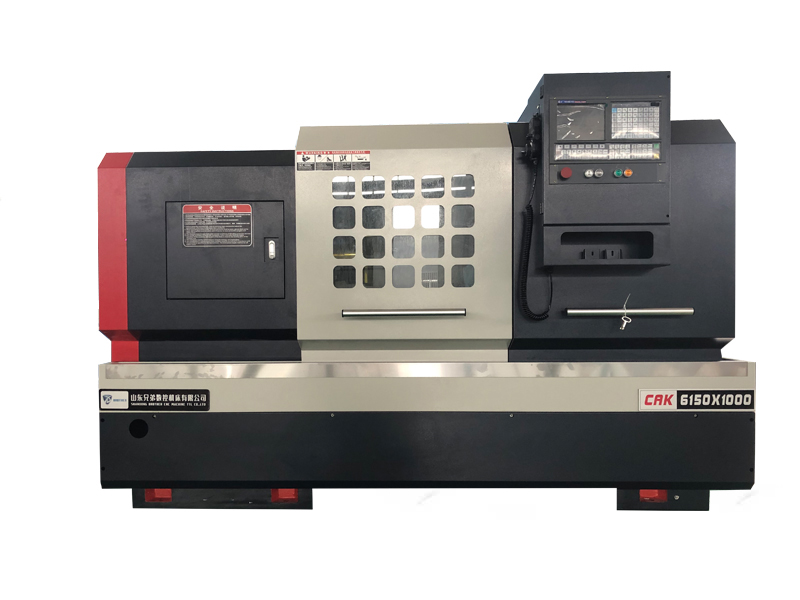
CAK6150 reference ↗
Use its base 52 mm spindle and 500/280 mm swing references as separate checks. The 1000-length packaging reference is 2750 × 1550 × 1700 mm. Confirm the exact spindle, drive, chuck, holder and supported cut envelope before selecting the machine.
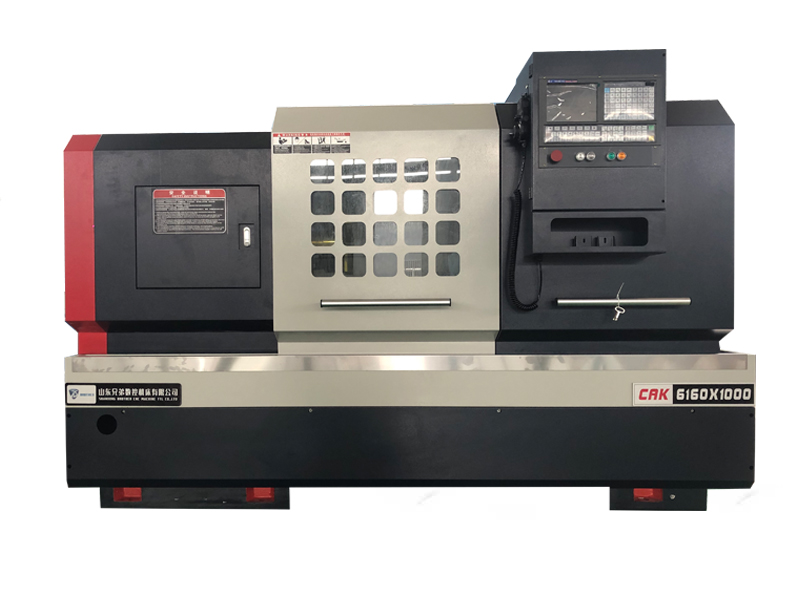
CAK6160 reference ↗
The family table offers the larger 610 mm bed swing, with a 2750 × 1550 × 1900 mm packaging reference for the 1000-length version. Longer beds change handling and installation requirements; do not extend the photograph's configuration to all lengths.
The CAK6150-1000 page lists 2550 mm length in its summary but 2750 mm in the detailed 1000-length packaging row. These references do not agree. Use the ordered machine and shipping drawings for access and handling; neither catalogue figure replaces that check.
Quote the gear changes, chuck and toolholder as a package
The CAK6150 table lists three speed ranges, 21–150, 66–500 and 162–1500 rpm, with automatic gear change optional. CAK6160 lists a manual three-range 21–1500 rpm arrangement and a separate 100–1600 rpm independent-spindle alternative. Do not add these into one standard speed package. Confirm the actual spindle drive, gear-change method, torque curve and program/operator sequence for the material and roughing cut.
Chuck and tailstock
The references describe manual three-jaw chuck and self-locking manual tailstock arrangements, with hydraulic or other actuation offered as options. Specify jaws, grip force, rotating mass, speed, centre and support. The table's C6/D8 labels are not a chuck diameter in millimetres; obtain the actual spindle interface and chuck drawing.
Control and tools
The text describes four-station vertical and six-station horizontal toolholder alternatives and several control/drive choices. Identify the delivered holder, station size, index/locking sequence, control revision and threading/arc functions. A catalogue controller list does not confirm current availability, simultaneous option compatibility or automatic compensation.
Test the difficult shoulder, thread and released shaft
Use the final gripping and support concept
Choose representative material/heat treatment and blank allowance. Record jaw projection, grip length, tailstock/centre and any rest, tool nose geometry and program. For a disc, test the largest relevant tool passage; for a shaft, test the longest supported cut and thread run-out.
Include manual actions and changes
Run loading, clamping, gear changes, tool indexing, roughing, finishing and inspection. Confirm which actions are manual on the delivered build. Do not quote unattended output or complete-cycle time from spindle speed, rapid traverse or a short demonstration alone.
Measure after unclamping
Check the agreed drawing datums, straightness, diameter/taper, shoulders, thread form and finish under stated thermal conditions. The original table and prose give different repeatability figures; obtain the applicable test sheet and part acceptance. Catalogue resolution and machine-axis figures do not guarantee the released part.
Name the Tengzhou supplier and ordered build
The original site identifies 山东兄弟数控机床有限公司 in Tengzhou and presents CNC/conventional lathes, radial drills and related machine-tool products. The material reviewed here establishes its published CAK references and configuration descriptions; it is not an independent site audit or proof of a certification. Confirm the legal supplier and machine nameplate, warranty and destination support in the order.
The family tables provide packaging dimensions and paired weight values without clearly defining each weight. Request net machine and shipping masses separately, with actual lifting, foundation, power and service drawings. Define levelling, lubrication, coolant, guarded operation, commissioning, training, parameters/program backups and the approved chuck/support arrangement. Qualified installation must follow the delivered machine instructions and applicable site requirements.
Send the exact suffix, length and supported part
Attach material, blank/finished drawing, jaw grip and projection, shaft length/diameter, centre/rest arrangement, internal bore or bar requirement, shoulders/threads, toolholder and released-part inspection. Name basic/B/C spindle, bed length, drive/gear changes, chuck/tailstock actuation, control, quantity target and destination.
Send Xiongdi RFQ ↗