
宁波天瑞精工机械有限公司 · Ningbo Sky Master Precision Machinery
SKY MASTER: match the spindle to the cut.
Compare the VF108P and VF1290 around the loaded fixture, holder interface and continuous duty. For multi-face work, check the cradle route separately.
Compare the two VF setups ↓Prepare a SKY MASTER RFQ ↗
Original model/configuration tables, inspection illustrations and primary standards record reviewed 8 October 2026
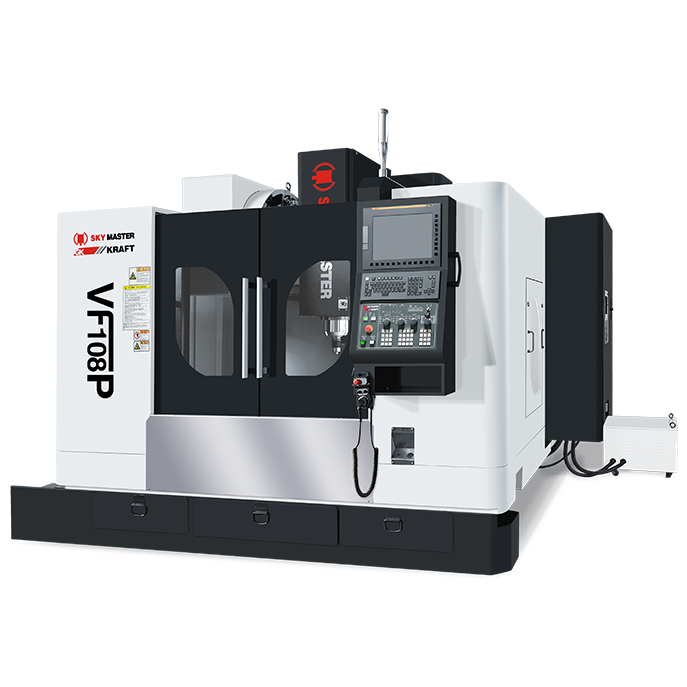
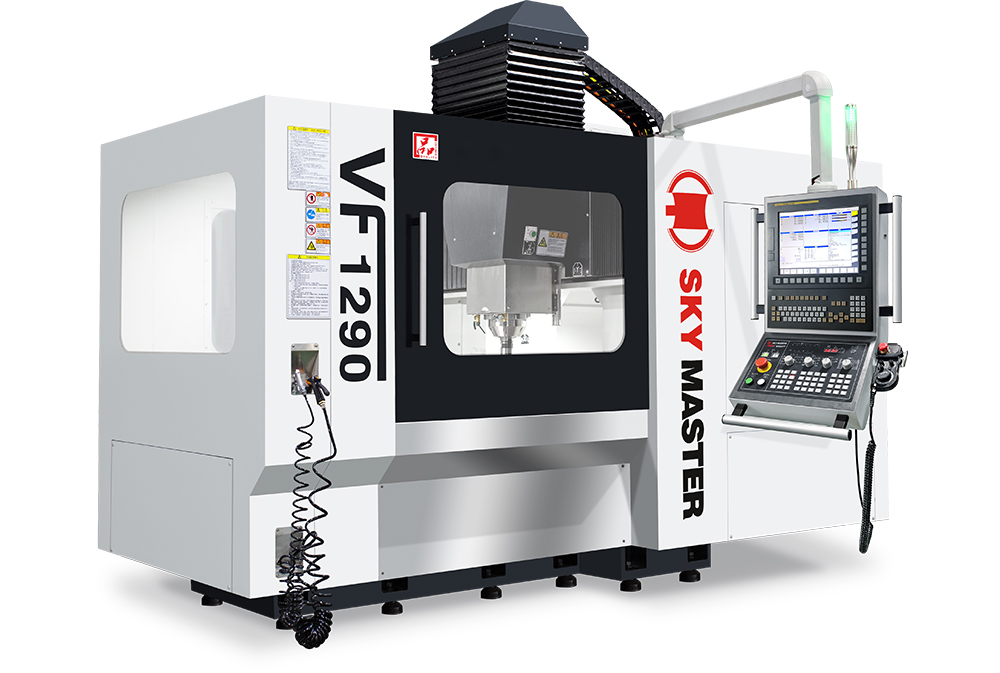
VF1290 is wider in Y; VF108P has more listed Z travel
These are three-axis high-speed-series references. VF1290 has a larger table and Y travel, but its 500 mm Z stroke is shorter than VF108P's 600 mm. Put the actual fixture, tallest tool assembly, workpiece height and deepest feature in a loaded section; table size and Z travel alone do not establish spindle-nose clearance or safe approach.
On a phone, swipe the comparison sideways.
| Reference | VF108P | VF1290 base |
|---|---|---|
| X / Y / Z travel | 1080 / 600 / 600 mm | 1200 / 800 / 500 mm |
| Table size | 1280 × 600 mm | 1320 × 800 mm |
| Listed spindle | HSK-A63, direct drive, 15,000 rpm | HSK-A63, direct drive, 15,000 rpm |
| Continuous / maximum motor power | 9 / 15 kW | 9 / 15 kW |
| Continuous / maximum torque | 57.3 / 120 Nm | 57.3 / 120 Nm |
| Machine dimensions L/W/H | 3930 / 3510 / 2850 mm | 4220 / 3350 / 3215 mm |
| Machine mass | 6900 kg | 12,000 kg |
Obtain the permitted table load and offset for the complete fixture; the individual technical tables do not give a load value here. These machine dimensions are not the full operating/service footprint. The original layout drawings show doors and the swing of the control enclosure beyond the main body.
Do not assemble a VF1290 from three different columns
Base VF1290
The base table gives 15,000 rpm direct drive, HSK-A63, 9/15 kW and 57.3/120 Nm continuous/maximum. FANUC 0i-MF Plus is the listed control. Use it as one coherent reference, then name any accepted alternative.
VF1290A
The A column gives a 24,000 rpm built-in spindle, HSK-A63, 30/39 kW and 29.1/37.8 Nm continuous/maximum. Its listed control is Mitsubishi M830W. More power does not mean more torque at every speed.
VF1290B
The B column gives 36,000 rpm built-in spindle, HSK-E50, 20/26 kW and 10.4/13.5 Nm continuous/maximum, also with Mitsubishi M830W. It needs a different holder and magazine plan from the A63 variants.
For a large roughing cutter, start with engagement and the duty curve at the actual cutting speed. For a small finishing tool, start with required surface speed, runout, holder balance and projection. Continuous and maximum ratings are different; the table is not a complete speed/torque curve or a guaranteed cycle on every material.
Make the tool and chip plan part of the selected build
VF108P's configuration table offers BBT40 and higher-speed electric-spindle alternatives, plus several arm/chain magazines. Those alternatives do not change the baseline table by default. VF1290's A63 arm/chain/drum choices and the B variant's E50 drum route also differ. Specify actual occupied tools, largest diameter, length, mass, adjacent-position clearance and sister tools; a list of magazine choices is not one included tool capacity.
Multi-face access moves the workpiece into the collision study
SKY MASTER's catalogue separates VL linear-guide, VF high-speed, VU cradle, UM five-axis double-column and VM double-column routes. A cradle is relevant when the drawing needs inclined access or datum relationships across several faces. It does not make every part fit simply because its flat outline fits the X/Y travel.
The VU500/600/800 group table distinguishes Ø500/630/800 mm tables from Ø630/800/1000 mm maximum workpiece-diameter references. The first two share a listed +90° to −120° A range; the larger reference gives +120° to −120°, with C rotation listed separately. Bring the tilted part, fixture and tools into the swept-envelope check, then confirm allowable mass and moment at the selected angle.
The group page uses M-suffix names in its configuration list and shorter names in its technical columns. Specify the exact suffix/revision and associated rotary drive, control, table and photo before comparing a quote. Its TCP/inclined-plane functions, reference-ball compensation and measuring options need the actual CAM/postprocessor, calibration and contract scope. These five-axis references must not be transferred to VF108P or VF1290.
Turn the manufacturer's inspection sequence into your acceptance record
The quality page illustrates incoming inspection, assembly/running checks and servo adjustment, followed by geometric, laser and ballbar checks, heavy cutting, spindle vibration/noise, thermal elongation, trial cutting and final checks. That is the manufacturer's published inspection process; it is not an independent test of the machine offered to you.
Check the selected machine and thermal routine
Request records tied to the delivered serial number and build: axis positioning/reversal, geometry, spindle runout, vibration and temperature behaviour at agreed conditions. Record the installed compensation and scale configuration. A ballbar result is not a finished-part dimensional report.
Trial the difficult cut with your tools
Use the intended material, fixture, holder projection and cutting engagement. Include a demanding roughing cut and the smallest or deepest finishing feature. Record tool wear, chip removal, warm-up and complete elapsed time rather than extrapolating from maximum rpm.
Release and inspect the part
Agree drawing datums, inspection equipment, sample count and thermal conditions before cutting. Inspect after unclamping where fixture stress can alter shape. For a five-axis route, include cross-face relationships and the agreed rotary calibration/CAM revision.
Use company and service evidence for the scope it actually supports
The Chinese site identifies 宁波天瑞精工机械有限公司; the English version uses NingBo Sky Master Precision Machinery Co., LTD. Its original logo carries both SKY MASTER and KRAFT branding, and its company page describes a German development partnership. This does not establish a German manufacturing origin for every delivered machine.
The official GB/T 42707.2-2024 record names the exact Chinese company among drafting units for CNC remote-operation/maintenance fault diagnosis and predictive maintenance, effective 1 May 2025. Participation is a dated company record, not certification of a VF model or proof that remote diagnosis is installed.
Agree the actual contracting/manufacturing entity, destination power, transport/access plan, commissioning and control/CAM training. For remote support, specify data access, permissions, backups and who performs on-site work. Request the selected machine's declaration and applicable safety documents rather than assuming the company's general certification claims cover every option and destination.
Send the tool assembly as well as the part
Include material and blank/fixture CAD, loaded mass and offset, tallest setup, deepest feature, tool/holder dimensions and balance requirements, cutting duty, selected VF suffix/spindle/control, occupied magazine, coolant/chip needs, measurement/CAM scope, acceptance drawing and installation destination. For VU, add tilted envelope and rotary loading.
SKY MASTER RFQ ↗