
Steel fabrication · plate processing
Shandong Sunrise CNC Machinery Co., Ltd.
For a connection plate, choose the hole-making process before the machine. Sunrise's reviewed drilling and punch/marking models differ in thickness, hole size, clamping and tooling.
Official company and model tables checked 8 October 2026
- Chinese entity
- 山东天旭数控机械有限公司
- Published location
- Qihe, Shandong
- Compare here
- TPD2016 drilling · TPP103 punch/mark
Which route survives the hardest plate?
Steel grade, thickness, hole diameter, edge distance and the required finished edge can eliminate a route before price or cycle time matters. Check the demanding part in the mix, not an average plate.
| Decision | TPD2016 · drilling | TPP103 · punching/marking |
|---|---|---|
| Plate/stack thickness | Up to 100 mm processing thickness; 15–100 mm clamping range | 5–25 mm plate |
| Hole size | Ø12–50 mm drill | Ø26 mm maximum punch |
| Part arrangement | One, two or four zones, with different per-part sizes | 1500 × 800 mm maximum plate; at least 25 mm hole-to-edge |
| What must be proved | Clamp access, stack registration and breakthrough | Material-dependent force, die clearance and burr/edge quality |
Swipe the table sideways on a narrow screen.
A mixed job can need both processes. Request a routing proposal for every plate class. The published 1000 kN force is not a promise that every Ø26 mm hole in every 25 mm steel plate can be punched acceptably.
The loading plan changes the usable area
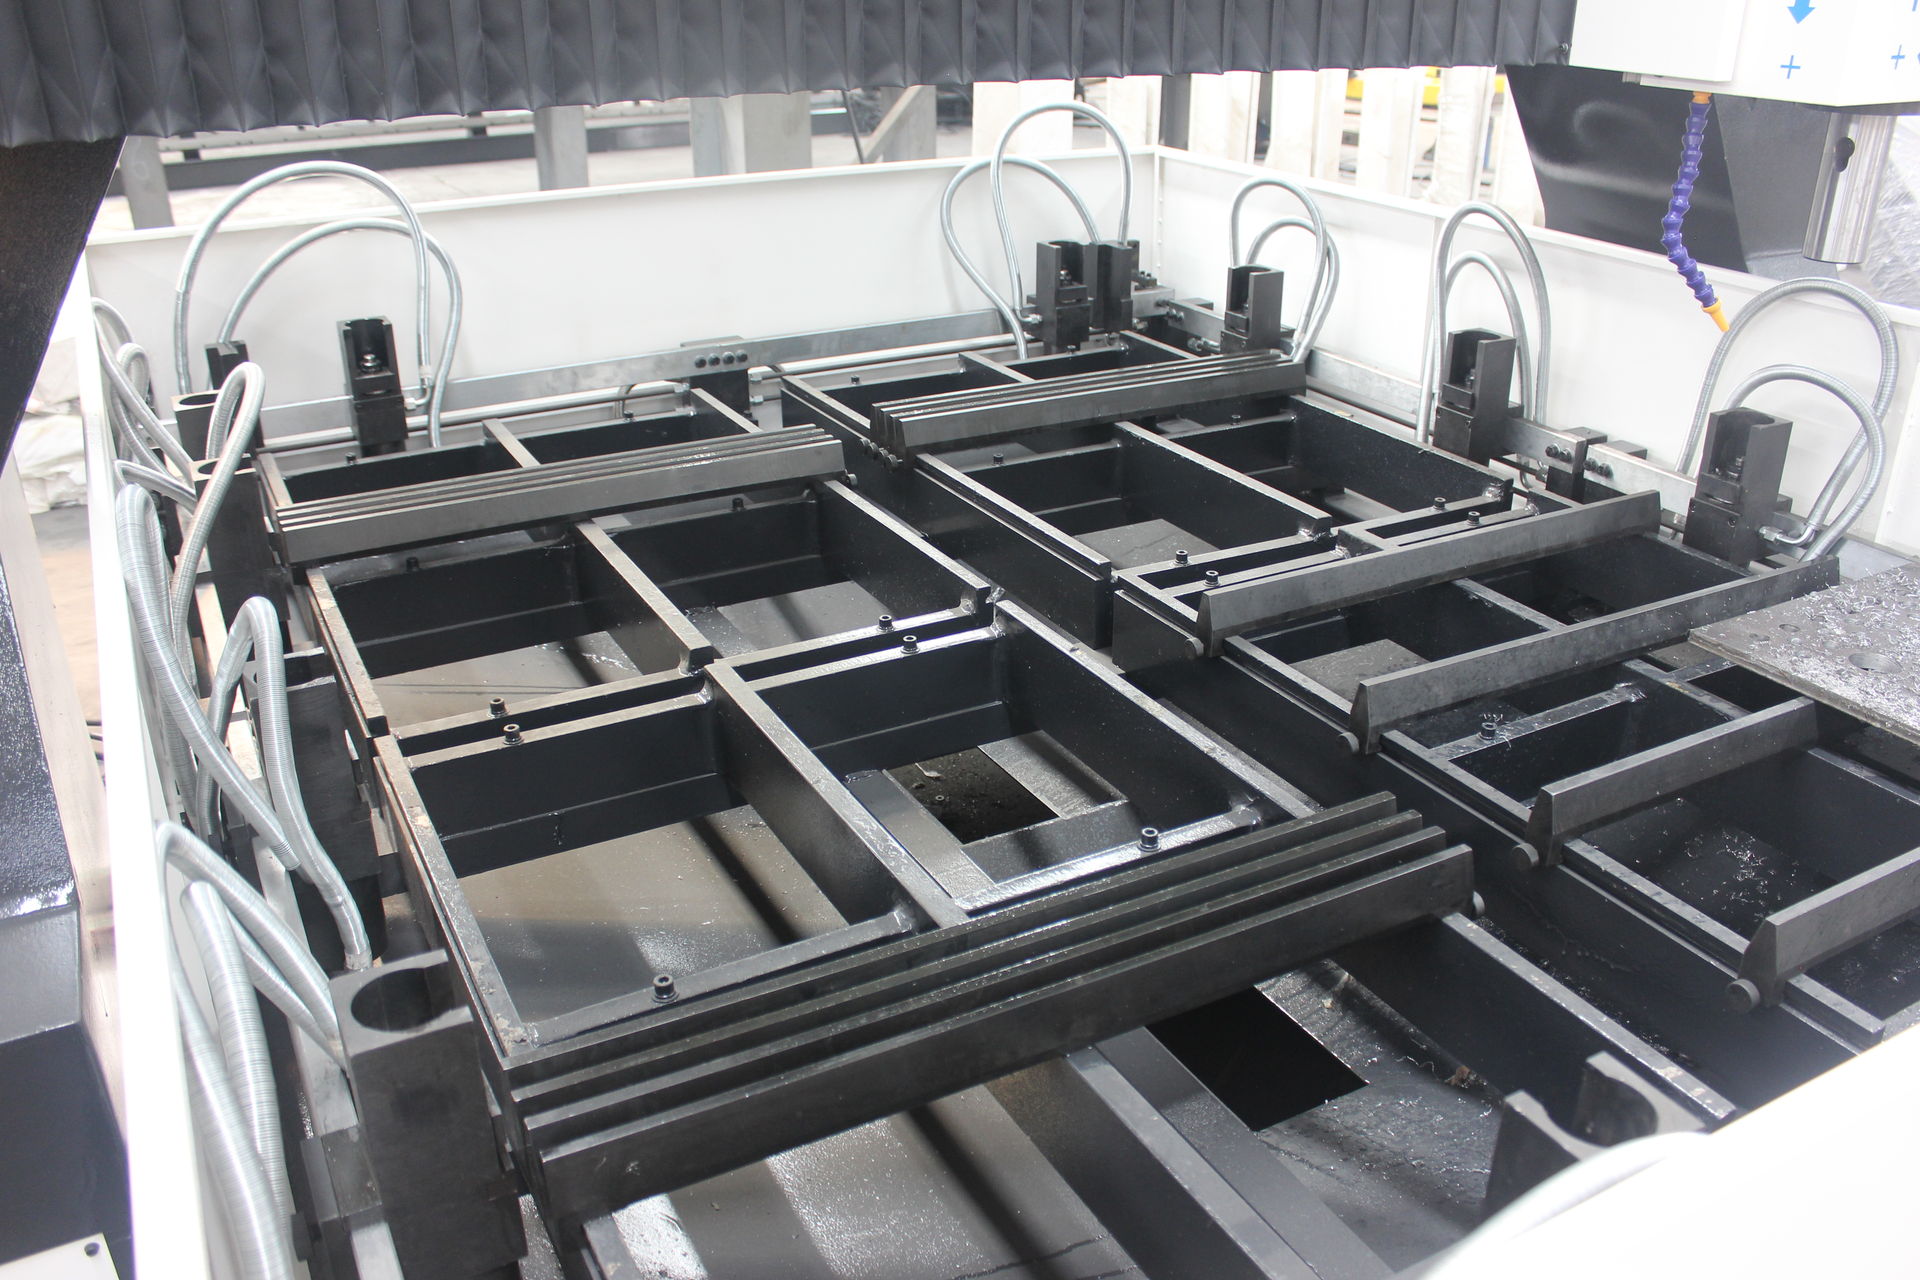
TPD2016: draw the clamps on the plate
One workpiece can occupy 2000 × 1600 mm. Two-part zoning allows 1000 × 1600 mm per part; four-part zoning allows 1000 × 800 mm. The maker lists twelve table clamps at 7.5 kN each, plus a separate bed-locking cylinder.
Plot all holes, datum edges and clamp positions. For stacked plates, specify the registration method, total stack and drill exit condition. A small part does not automatically fit a zone when a clamp blocks the hole pattern.
TPD2016 model and specifications ↗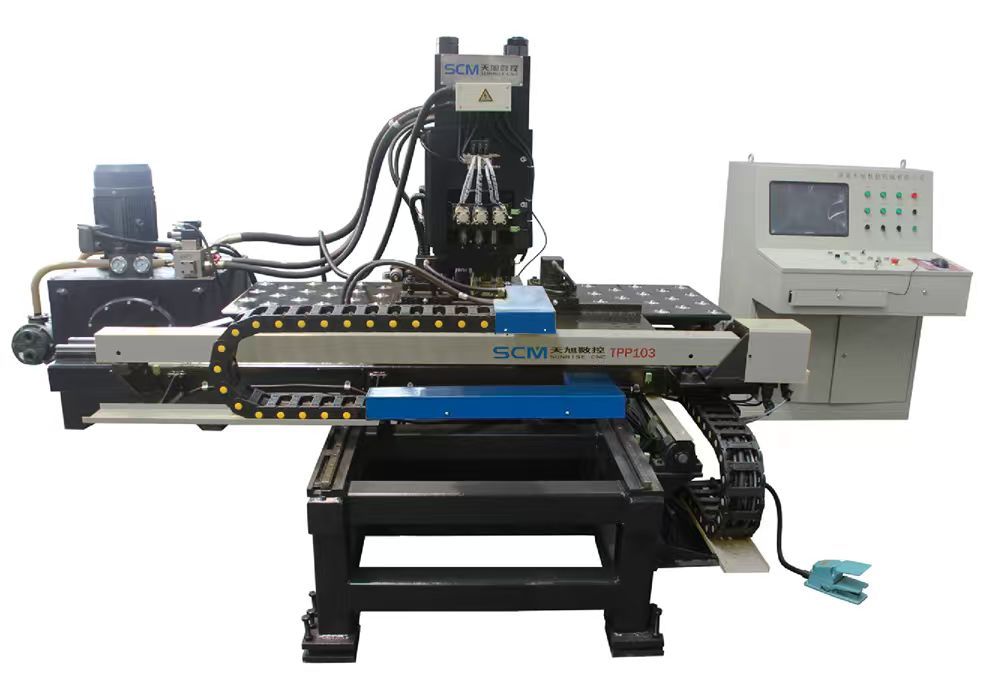
TPP103: dies and marking belong on the nest
The C-frame machine lists three die stations, including marking. The TPP103 column gives 1000 kN punch force, 800 kN marking force and twelve characters. The reinforced TPPR103 on the same source page has different ratings; those are not used here.
Supply each hole diameter, nearest edge, character string and steel grade. Ask for die clearance, loading orientation, support and a tested burr limit. The photo represents the product family; confirm the exact offered build.
TPP103 model and specifications ↗Check the drawing-to-machine handoff
The TPD series describes converting AutoCAD drawings and accepting programs produced by TEKLA lofting software. TPP103 also lists AutoCAD or lofting input. These descriptions do not establish compatibility with every export or software release.
- Send a representative production file. Include units, hole coordinates, plate orientation and part identifier.
- Approve the resulting hole schedule. Check datum zero, mirrored parts, hole sizes and marking before machining.
- Define the whole cell. Quote loading, chip or slug removal, coolant, marking, deburring and final inspection, with each supplied item identified.
Make one acceptance plate answer the real questions
Choose the thickest or most difficult material in the order mix, including the smallest edge distance and demanding hole pattern. Agree diameter and position measurements, burr/edge acceptance, stack alignment where applicable, tool/die wear and a cycle breakdown including loading and inspection. A no-load motion video cannot establish the result.
Bring these items to the trial
- CAD/DXF and dimensioned drawing with the agreed datum.
- Steel grade, material condition and single/stack thickness.
- Hole schedule, marking text, finish and downstream assembly requirements.
- Inspection method and acceptable measured limits for the sample.
A builder of fabrication equipment
The manufacturer's company account identifies Shandong Tianxu CNC Machinery in Qihe, Shandong, using the Sunrise CNC mark. Its published range includes drilling, punching, milling and cutting equipment for tower members, structural steel, tube plates and other fabricated components. This page compares only the two named plate machines; the wider range needs its own model review.
The national standards platform lists the Chinese company among drafting organizations for angle-processing-line plan 20254241-T-604, issued in August 2025. This supports a specific standards-project association; it does not certify TPD2016 or TPP103. Exact official source records and rejected claims are retained privately.
Send the plate mix, not only a model name
Attach the drawings, steel grades, plate/stack thicknesses, hole sizes and edge distances, marking needs, annual mix and inspection criteria. Ask for a routing, tool/die schedule, clamp layout, trial and installation proposal.
Prepare a Sunrise RFQ ↗