
Suzhou Tieba CNC Machine Tool Co., Ltd.
Tripak machining-centre range
Size the fixture and cutting tools before choosing a Tieba machining centre.
TB-855G and TB-2518 address different table loads, spindle interfaces and tool envelopes. Check the complete clamped part and the required cutting operation before comparing travel numbers.
Official company, model columns and original images reviewed 8 October 2026
Include the fixture in both the height and the load
The company describes vertical, gantry, drilling/tapping and horizontal machining centres, with application sectors including moulds, automotive and electronic communications. This comparison covers two existing model references; a neighbouring catalogue model's spindle, load or head options are not assigned to either one.
| Workholding check | TB-855G vertical | TB-2518 gantry |
|---|---|---|
| X / Y / Z travel | 800 / 550 / 550 mm | 2500 / 1800 / 1000 mm |
| Table and rated load | 1000 × 550 mm; 500 kg | 1600 × 2500 mm; 7000 kg |
| Spindle nose to table | 110–660 mm | 150–1150 mm |
| Spindle choice | BT40: 12000 rpm direct drive or 10000 rpm belt drive | BT50: 6000 rpm belt drive |
| Tool length / mass | 300 mm / 8 kg catalogue limits | 350 mm / 15 kg catalogue limits |
| First drawing to send | Vise/fixture stack, part datums and longest tool | Loaded fixture mass distribution, tall features, lifting and cutter reach |
Swipe horizontally on a small screen.
A table-load rating includes the workholding package; it is not unrestricted workpiece mass. Calculate fixture, clamps and blank together, and agree load distribution and permitted moments. Check spindle nose position, tool/holder projection and part/support height in one drawing. Z travel alone does not establish usable part height.
TB-855G: decide the spindle from the real cut
TB-855G model ↗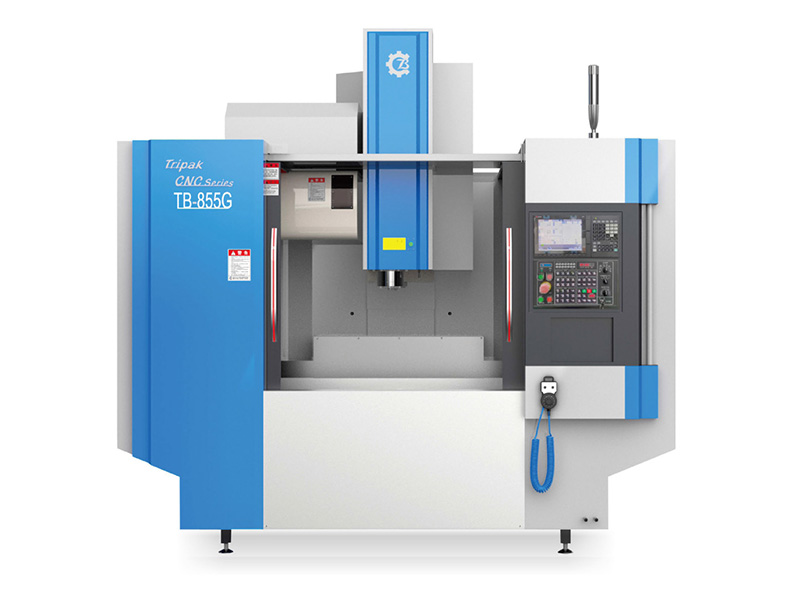
The exact TB-855G column gives 800 mm X travel, despite the number in the model name. Its 1000 × 550 mm table and 500 kg load reference suit a different workholding package from the larger gantry; verify the actual part rather than infer travel from “855”.
The page lists direct-drive 12000 rpm and belt-drive 10000 rpm alternatives. Obtain the chosen spindle's torque curve and the duty basis for its 11/15 kW rating pair. A fast small cutter and a heavy roughing cutter require different checks; the maximum speed does not establish sustained power at the intended cut.
Its 24-position magazine permits 80 mm tool diameter with adjacent pockets occupied, or 160 mm with adjacent pockets empty. Account for empty stations and sister tools before calling the magazine adequate for the job.
TB-2518: prove the large fixture and working reach
TB-2518 model ↗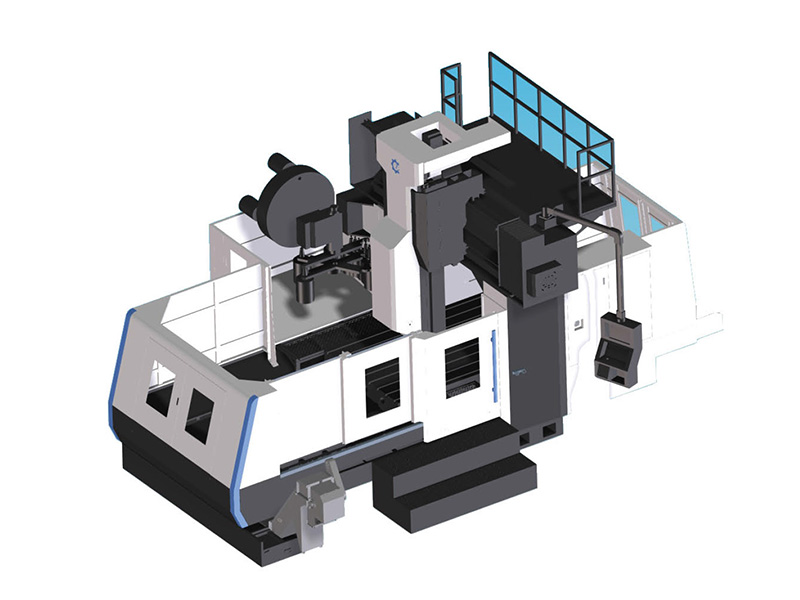
The TB-2518 column lists a 1600 × 2500 mm table, 7000 kg table load and 2500 / 1800 / 1000 mm travels. Its spindle-nose-to-table range is 150–1150 mm, with BT50 belt drive up to 6000 rpm and a 22/26 kW rating pair. Agree the duty and torque for roughing, drilling or the intended large cutter.
A wide table and Y travel do not specify every clearance between the gantry, part and fixture. Request the cross-section and access drawing, including raised bosses, clamps, longest tools and load/unload route. Any angle head, extra axis or five-face process must be itemised; gantry naming alone does not include those capabilities.
A large cutter can reduce the usable magazine
TB-2518 tooling boundary
The table lists 24 tools, 350 mm maximum length and 15 kg maximum weight. Maximum diameter is 110 mm with adjacent stations occupied, or 220 mm with adjacent stations empty. Include the entire holder/adapter and cutter assembly in the reach and permitted mass check; confirm how the limits apply with the supplying party.
Clearance before cutting
List roughing, finishing, drilling and tapping tools, sister tools and blank magazine positions. Check the machining clearance and tool-change path. A cutter that clears the workpiece in one position may still interfere with an adjacent tool, clamp or enclosure during exchange.
Use different trial parts for the two decisions
These are buyer-planning examples, not claimed Tieba customer results. Replace them with the actual drawing, material and inspection requirements.
A compact plate or housing on TB-855G
Trial the intended vise/fixture, longest drill or tap and a representative small-tool operation. Include hole-to-datum position, pocket/face dimensions and surface condition. Record the installed spindle, program and tooling; measure after release and include load/unload plus tool replacement when evaluating accepted-part output.
A heavy mould plate or base on TB-2518
Trial the representative mass, supports and clamps with the intended roughing and finishing sequence. Measure drawing-critical geometry near the centre and difficult edges under the agreed thermal/load conditions. Check flatness and datum relationships after releasing clamps; include lifting, setup and head/tool changes in elapsed time.
The pages' ±0.005/300 positioning and ±0.003/300 repeat-positioning entries do not warrant finished-part geometry under every loaded fixture. Define machine inspection separately from part acceptance, with test method, temperature, instrument and sampling agreed. Retain accepted parts, rejects, interventions and tool usage alongside cycle data.
Plan lifting, foundations and responsibility before shipment
The TB-2518 column gives 25,000 kg machine mass. Obtain current shipping/foundation drawings, floor-loading requirements, delivery route and crane plan. Its blank overall-dimension fields cannot be filled by borrowing a neighbouring model. For either machine, confirm supply units, power, air, coolant, chip handling and service access from the installation package.
Suzhou Tieba CNC Machine Tool Co., Ltd. uses Tripak branding in the reviewed catalogue. The government-hosted 2025 Jiangsu technology-based SME list names the Chinese entity at row 20092. This dated listing supports identity, not a machine certification, factory audit or delivered machining result.
The order should identify the legal supplier, configuration, control/postprocessor, destination-service party and acceptance responsibilities. Specify training, program/parameter backups, consumables and fixture/tooling handover. Agree optional probing, rotary equipment, heads and chip/coolant systems individually.
Send the loaded fixture and tool schedule
Include part/datum drawings; material and blank condition; fixture/blank mass and distribution; clamp/support heights; longest/heaviest tools and large-diameter magazine occupancy; spindle/drive choice; roughing/finishing requirements; accepted-output target; lifting/installation drawings and destination.
Send Tieba RFQ ↗