
Factory profile · precision machining
Beijing Jingdiao Technology Group Co., Ltd.
First prove the part and fixture fit the axis envelope. Then define the controller, CAM and measurement package as separate deliverables.
Manufacturer product pages reviewed September–October 2026 · Profile reviewed October 2026
- Reviewed routes
- Three-axis · five-axis
- Compared here
- JDHGT600T · 600TH · MRA600
- First buyer check
- Tool, fixture and rotary access
Does the part need rotary access—or more Z room?
A three-axis part with a taller fixture may favor a different Z envelope. A multi-face part may need five-axis motion, but only when the loaded fixture and longest holder clear the full rotary sweep.
| Machine | Travel / table | Published load | Deciding check |
|---|---|---|---|
| JDHGT600T · 3-axis | XYZ 600 / 500 / 200 mm; 650 × 650 mm table | 300 kg | Can the full tool and fixture stack fit 200 mm Z? |
| JDHGT600TH · 3-axis | XYZ 600 / 500 / 300 mm; 650 × 650 mm table | 300 kg | Does extra Z resolve the setup without rotary motion? |
| MRA600 · 5-axis | XYZ about 650 / 660 / 500 mm; Ø630 mm table | 400 kg | Do part and fixture clear every A/C position? |
On a narrow screen, swipe the comparison sideways.
The 600T photo does not show the 600TH build
These two machines share a published table class but differ in vertical travel and spindle offerings. The pictured machine below is specifically JDHGT600T. Do not infer the TH enclosure or option package from that photo.
JDHGT600T
200 mm Z travel and a listed 32,000 rpm HSK-E32 configuration. Build a height stack from the stock, fixture, holder and longest cutter, then check approach and retraction—not only cutting depth.
Review 600T ↗JDHGT600TH
300 mm Z travel. Published spindle alternatives include 24,000 rpm BT30 or 20,000 rpm HSK-A50. Quote one selected spindle and holder; the fastest number and different interface cannot be combined into one machine.
Review 600TH ↗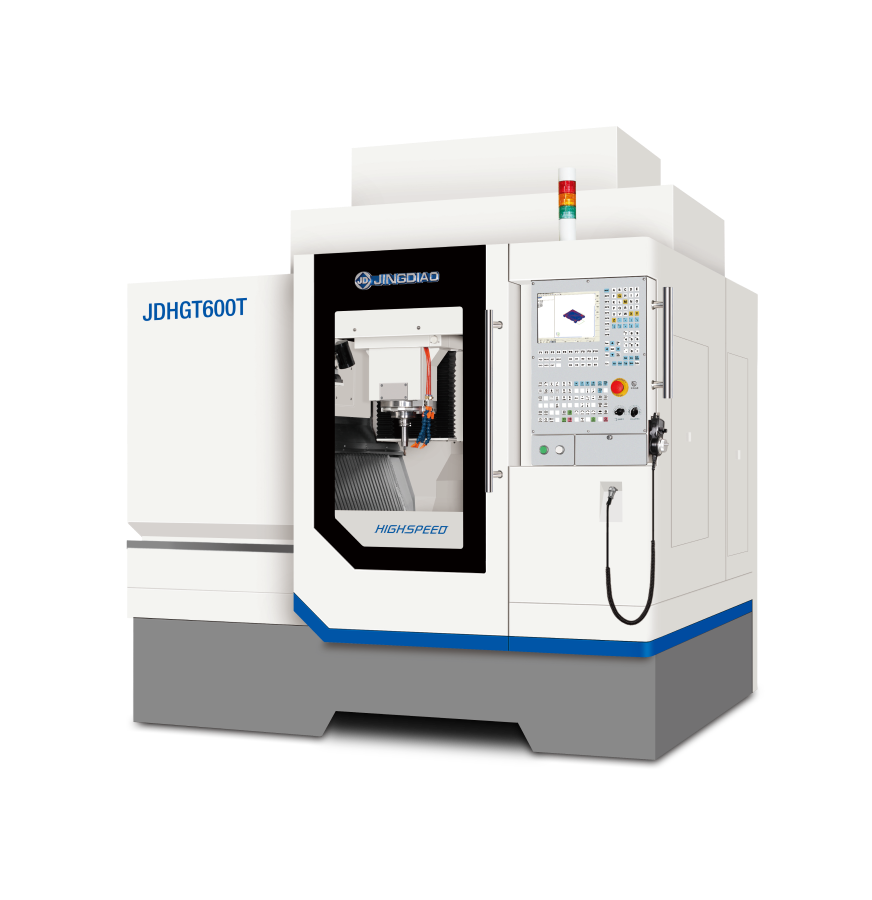
MRA600: test the swept volume
The manufacturer publishes a −120° to 90° A-axis range and 360° C-axis range for MRA600. Those angles do not mean a cutter reaches every face of a clamped part. Simulate the loaded setup through each programmed position and verify table, clamp, tool holder and enclosure clearance.
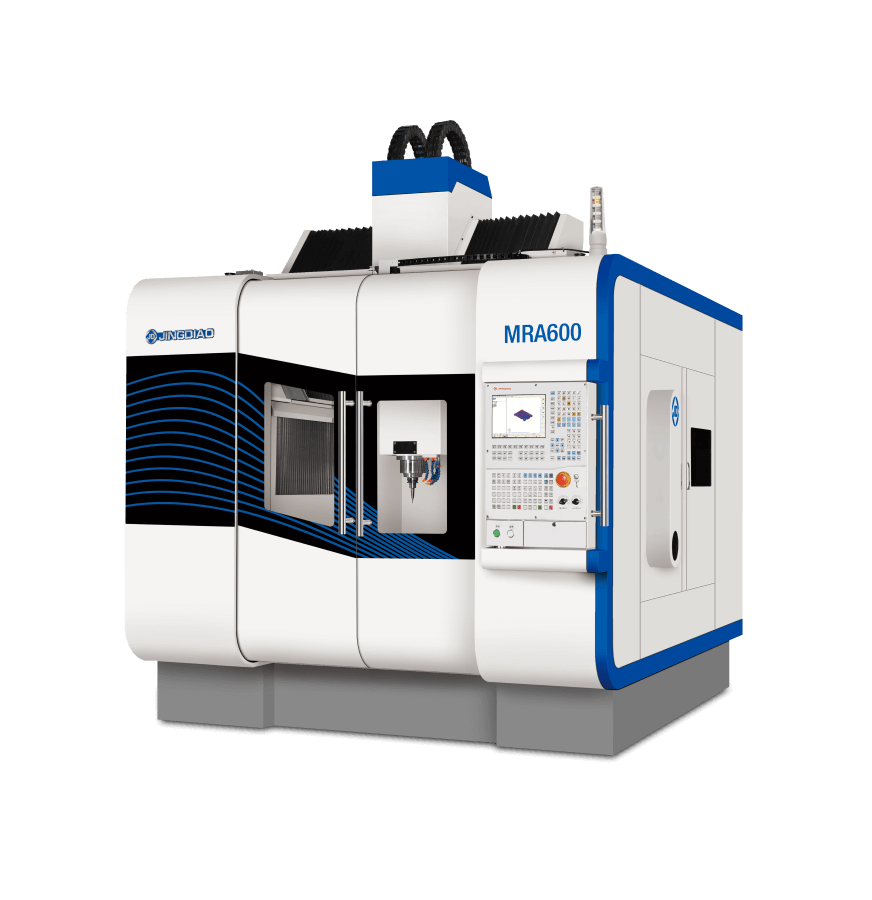
One part, one specified spindle
The model page lists 20,000 rpm HSK-A50 and 15,000 rpm HSK-A63 alternatives. Select the holder, tool length and spindle package against the cutting program. Ask for collision review and a measured sample part.
MRA600 model details ↗Machine, controller, CAM and probing are four lines
Jingdiao presents CNC control, CAM and on-machine measurement alongside its machine range. That portfolio does not establish that every function is standard on every model. An RFQ should name the controller release, postprocessor/program preparation, tool and workpiece probing, calibration method, training and inspection output for the exact proposed build.
A useful acceptance sample
- Choose the difficult face or deepest feature from a real production drawing.
- Provide STEP, stock, material, fixture, maximum holder assembly and loaded weight.
- Define finish, geometric tolerance, datum, measuring instrument and required report.
- For five axes, supply rotary positions and collision-sensitive clamps.
Other Jingdiao listings need their own fit review
These existing model pages remain available, but the travel and spindle figures above apply only to the three named configurations.
What was checked
The three named configurations and process portfolio come from manufacturer model and system pages. A 2024 Beijing municipal report describes the group's Beijing headquarters and production footprint at that time. It does not verify the present build location, a particular machine's delivered options or achieved part quality. Field-level source and media records are kept privately.
Ask for a part and process proposal
Attach the drawing and process facts through CNCVerified:
- Part/fixture/stock geometry, material, loaded weight and tallest tool.
- Three-axis access or required A/C positions and collision constraints.
- Selected spindle/holder, control, CAM and probing deliverables.
- Measured sample criteria, volume, training and installation destination.