
Hangzhou Good Friend · FEELER / Fair Friend · Hangzhou, Zhejiang
Choose the loaded fixture, then the VMP build.
Table area, reachable cuts and spindle packages answer different questions. Keep the Hangzhou entity and the FEELER brand distinct.
Official China and FEELER material, exhibition identity and historic issuer record reviewed 8 October 2026
Five table sizes, three different loaded-fixture decisions.
The VMP series is a vertical machining-centre route. Begin with the fixture footprint, clamps, part mass and cutting coordinates. A table can support a fixture whose full surface is not reachable by the spindle; axis travel is not a finished-part capacity.
| Retained model | X / Y / Z travel mm | Table mm | Maximum load kg |
|---|---|---|---|
| VMP-30 | 760 / 420 / 510 | 890 × 420 | 300 |
| VMP-32 | 820 / 520 / 505 | 950 × 520 | 800 |
| VMP-40 | 1020 / 520 / 505 | 1150 × 520 | 800 |
| VMP-45 | 1100 / 610 / 600 | 1200 × 600 | 1500 |
| VMP-50 | 1300 / 610 / 600 | 1420 × 600 | 1500 |
Current FEELER series table, with its merged cells checked against the named columns. Swipe to the load column on a phone. Confirm the actual revision and loaded setup.
Compact, relatively light fixture
VMP-30 has a 300 kg table-load figure. Include clamps, fixture, part and any rotary equipment in that check. Confirm the highest feature’s holder/nose clearance separately.
More Y reach or X length
VMP-32 adds Y reach and table load over VMP-30. VMP-40 adds X travel over VMP-32 while retaining the same published Y/Z travel and load. Locate the difficult end features before choosing the longer table.
Heavier or wider setup
VMP-45 and VMP-50 share the published Y/Z travel and 1500 kg load. VMP-50 adds X travel and table length. Neither establishes clearance around a tall fixture or a standard rotary package.
Specify the taper and spindle as one package.
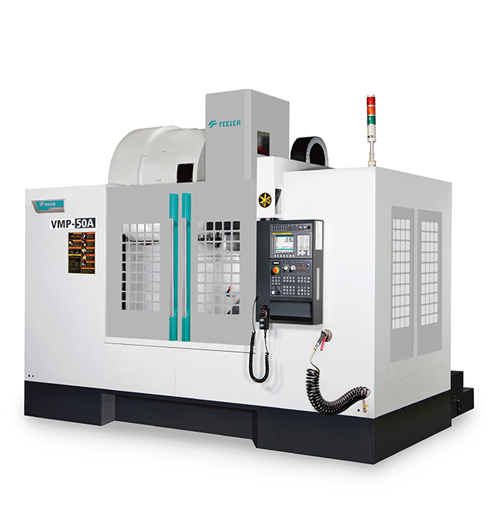
The VMP-45 and VMP-50 columns contain alternatives: 10,000 / 4,000 rpm, No.40 / No.50 taper and 22 / 24 tools. The table does not itself pair every alternative into a supplied configuration. Request one coherent spindle, interface, magazine and tool-limit schedule; do not combine the fastest spindle with whichever taper and tool count looks most attractive.
For VMP-30, VMP-32 and VMP-40, the current columns list 10,000 rpm and No.40 taper. Confirm the actual duty curve, controller, holder standard, retention system and occupied tool limits. A taper number and maximum speed do not establish low-speed torque, holder access or surface quality for your cut.
The official family description attributes its cutting-stability approach to a cast-iron structure, an A-frame column and enlarged base. It also discusses guideways, wear pads and ball-screw drive. Use these descriptions to ask about the offered build and test conditions; a structural description is not an inspected-part accuracy guarantee.
Separate longer travel from a faster complete job.
VMP-32 and VMP-40 list X/Y/Z rapid rates of 40/40/30 m/min. The VMP-30 column lists 36/36/36, while VMP-45 and VMP-50 list 36/36/24. These are axis rapid rates. Loading, tool changes, probing, cutting, chip clearing and unloading still determine the complete production cycle.
The same current table includes separately named APC models. VMP-32APC has its own 700 × 500 mm table and 200 kg load; those figures and an automatic-pallet package must not be transferred to the retained VMP-32. If reducing operator time is the goal, compare the actual loading method and pallet schedule with the ordinary build, including fixture duplication and recovery.
For a mixed job queue, show tool usage, fixture changes and the real ratio of repeat to changeover work. Agree which setup, first-off inspection and intervention time the supplier includes in a cycle proposal. An axis-speed comparison alone will not answer the production question.
The Hangzhou record and the Taiwan brand are separate identities.
This directory keeps its existing Hangzhou Good Friend Precision Machinery record. A 2021 Hong Kong issuer report names that Chinese company. The current China company site identifies 友嘉国际数控机床有限公司 at the Hangzhou Xiaoshan location and describes a business established in 1993. Obtain current registration and contracting-name correspondence for the proposed transaction instead of treating a historic English name as a verified current seller.
FEELER’s current company page identifies the brand with Fair Friend Enterprise Co., Ltd. in Taiwan under FFG. The TIMTOS exhibitor record independently associates that company name with FEELER. Those sources establish brand/company context; they do not prove that every VMP machine on this page is manufactured by the Hangzhou legal entity.
Request the quotation’s legal seller, actual builder and build location, serial-machine records and destination service provider. Keep original factory inspection and the distributor or integrator’s commissioning responsibilities separate. Neither group-wide rankings nor historic tax status are used here as a certification of the supplied machine.
Prove the difficult feature after the part leaves the fixture.
Loaded reach and tool access
Use a fixture drawing with masses, clamps, datum locations and all critical cuts. Demonstrate the longest holder and the feature nearest a clamp or travel limit. Confirm loading access and service clearances.
Material-specific machining
Record material, stock allowance, cutting tools, spindle duty, feeds, coolant and chip handling. Trial the critical deep hole, end feature or surface with the supplied package rather than a favourable substitute.
Released-part measurement
Define datums, geometry and finish limits, sampling and measurement/thermal conditions. Measure after release and repeat the representative work. Keep positioning data distinct from accepted part results.
Delivered responsibility
Agree configuration, installation, utilities, guarding, training, documentation, recovery and service. For a cell, allocate fixture, loading, interface and whole-cell acceptance duties to named parties.
Send a fixture drawing and a build question.
Include part/material, fixture and total mass, required cutting coordinates, clamps and loaded height, tool interfaces, critical tolerances and inspection conditions. Add batch mix, complete-cycle boundaries, destination and installation access.
Name the VMP model, taper/spindle alternative and any pallet or loading requirement. Ask for current contracting identity, actual manufacturing location and one complete configuration with a representative trial.
Prepare a FEELER RFQ ↗