
5-axis · Neway
Neway VM650FA
Neway CNC Equipment (Suzhou) Co., Ltd.
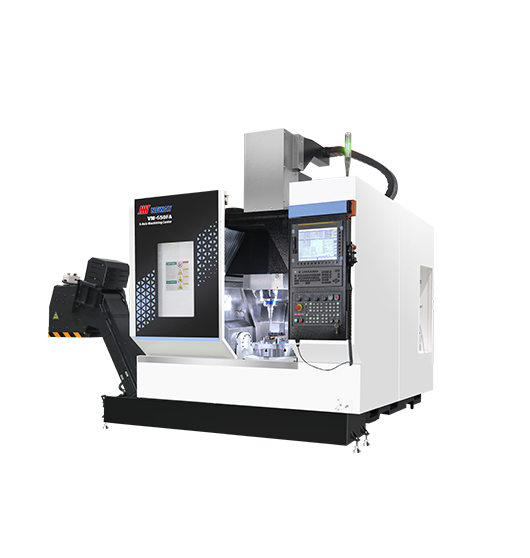
Whole original image marked VM650FA; no numerical or supplied-controller guarantee inferred.
The manufacturer distinguishes VM650FA by X/Y/Z/A/C simultaneous motion. Its table is Ø650 mm, the listed maximum table load is 500 kg, and linear travels are 650/715/500 mm. Select the fixture and clamp layout for this A/C arrangement rather than reusing a VM650F B/C setup model. The wider Y entry is a linear axis reference, not permission for an arbitrary overhanging part.
The shared row headed B/C explicitly marks the FA column as A/C and gives ±120°/360°. Read the exact column annotation. Spindle-nose-to-table distance is 150–650 mm. Check the loaded fixture through A tilt and C rotation, with the full holders and approach paths; obtain load, moment and inertia limits at the intended angle. The 500 kg catalog entry is not a verified allowable eccentric load at all orientations.
For VM650FA the spindle-speed entry is 10–16,000 rpm, the main-motor entry is 15 kW, and the table identifies No.40 7:24 taper with MAS403 BT40 holders. The disc magazine has twenty-four positions. This differs from the F version’s HSK-A63 package; a proposal that mixes those column values needs correction before a tool set is ordered.
The power entry has no duty duration or torque curve here, and the table omits full tool diameter, length, mass and occupied-neighbour limits. Request the exact motor/spindle drive, populated magazine and tool-retention schedule. Verify cooling, probing and controller/postprocessor functions for the selected unit rather than inferring them from the photographed console.
Supply the component, mounted mass and centre of gravity, fixture model and complete tools, then mark the surfaces that require coordinated A/C cutting. Demonstrate the production CAM program at its restrictive orientations and measure the released geometry. For work that only needs indexed faces, agree the locating/clamping and datum-transfer sequence instead of buying motion capability without a defined application.
Include interrupted-cycle recovery, rotary calibration and repeat setup in the trial. Keep loading, tool changes, chip removal and inspection in the elapsed result; 48/48/40 m/min linear rapids are not the cutting cycle. Ask for the installation and service layout, utilities, parameter/software backups and training responsibilities in the same dated build specification.
Catalog specifications
- Motion described
- X / Y / Z / A / C simultaneous
- Table diameter / maximum table load
- Ø650 mm / 500 kg; angular/eccentric load conditions to confirm
- X / Y / Z travel
- 650 / 715 / 500 mm
- A / C rotation reference
- ±120° / 360°; A/C annotation in the shared rotary row
- Spindle nose to table
- 150–650 mm
- Spindle speed entry
- 10–16000 rpm